
Application
3D Printer Nozzle Cleaning
For 3D Printer Nozzle Cleaning, the brush must reach the working area, disturb or collect sintered polymer/carbonized residue/resin residue, and release it without creating unacceptable surface damage or process interference. The available access and required motion should be reviewed together with the cleaning method.
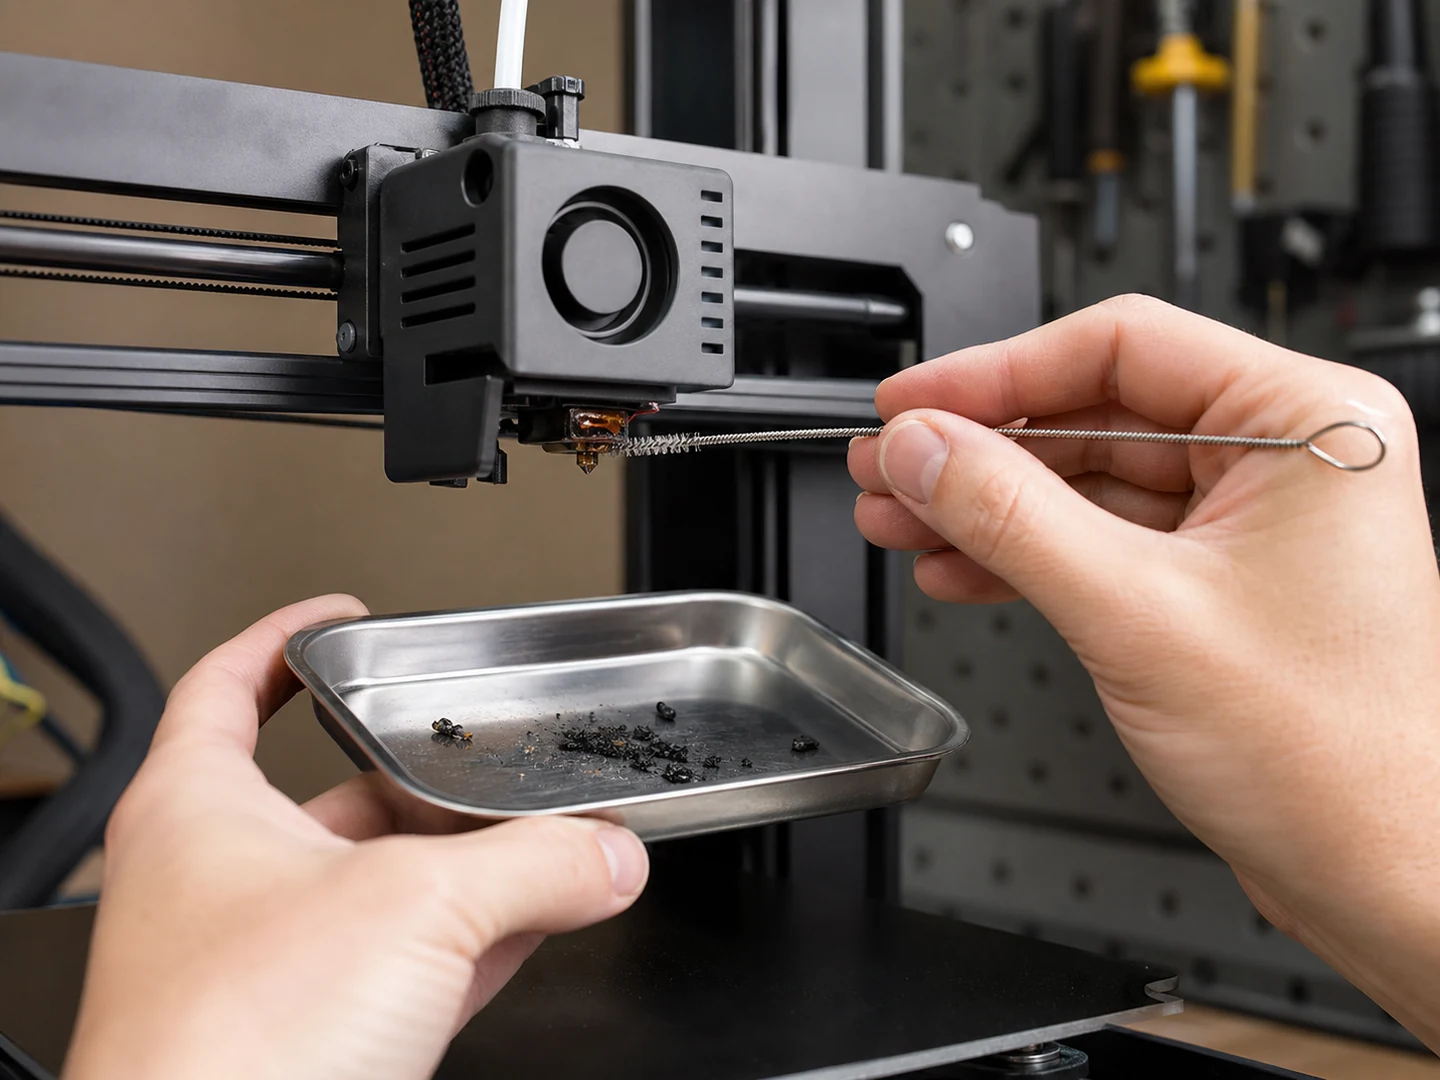
At a glance
- Cleaning target
- Sintered Polymer/Carbonized Residue/Resin Residue
- Working environment
- Dry Indoor Area / High-Temperature Equipment Maintenance Area
- Cleaning method
- Dry Brushing / Wet Brushing
- Requirements to check
- Power-Isolation and Hot-Component Maintenance Procedures; Scratch Control for Brass Nozzles and Surface Coatings
A hot-end nozzle is cleaned at temperature and to a fixed orifice size, so the tool has to lift carbonized polymer without opening the bore the printer is calibrated around.
What makes 3D Printer Nozzle Cleaning different from other electronics and precision cleaning?
The main difficulty is removing oil, carbon, scale, biofilm, process residue, and particles from bores, channels, tubes, hoses, ports, and internal passages without damaging the surface, loading the brush, or carrying contamination back into the process.
The work happens in dry indoor area and high-temperature equipment maintenance area against sintered polymer, carbonized residue and resin residue.
The part people get wrong: the residue tells you the filament, but the access opening tells you the construction. Get them in that order and the shortlist is short.
What are the most common cleaning targets in 3D Printer Nozzle Cleaning?
One target with two faces: the external tip and heater-block area a brush may touch, and the orifice it must not enter.
| Part or area | Residue type | Cleaning requirement |
|---|---|---|
| Hot-End Nozzle Tip and Bore | Sintered Polymer, Carbonized Residue, Resin Residue | The head must be narrower than the opening and stiff enough to lift residue without splaying at the mouth. |
The dimensional envelope those targets impose on the brush:
| Parameter | Typical range |
|---|---|
| Cleaning target | External nozzle tip and heater-block-adjacent deposits |
| Nozzle size | Use the installed nozzle specification; nozzle orifice size is not a brush-size specification |
| Brush contact | Use a small soft brass brush only on compatible metal nozzle exteriors; keep heater and thermistor wiring clear |
| Internal clogging | Use cleaning filament, cold-pull, or the printer maker’s unclogging method rather than pushing a brush through the orifice |
| Selection input | Nozzle material, hot-end geometry, access clearance, and contamination type |
Which brush types work for each cleaning target?
Miniature brass brush, detail brush or calibrated bore tool used under the printer maker’s maintenance procedure.
| Cleaning target | Recommended brush type | Why it fits |
|---|---|---|
| Hot-End Nozzle Tip and Bore | Handheld Detail Brushes | A fine hand-guided head lets the operator work the nozzle tip and the melt chamber without loading force onto the hot end. |
The layouts this application is normally built in:
- Driven brush — use when oil, carbon, scale, biofilm, process residue, and particles needs repeatable scrubbing or controlled relative movement
- Passive or free-running brush — use for loose contamination and lower process complexity on bores, channels, tubes, hoses, ports, and internal passages
- Localized hand, strip, or tube brush — use where only an edge, gap, port, or maintenance point needs contact
In practical brush terms: reach first, then residue. A brush that fits but is too soft can be stiffened; a brush that does not fit is simply the wrong tool.
What filament materials work best for 3D Printer Nozzle Cleaning?
Brass or soft metal for compatible hardened residues on approved nozzle alloys; nylon for cooled external areas; exact choice follows nozzle material.
| If the condition is… | Filament to start with | Why |
|---|---|---|
| Carbonised polymer on a brass nozzle exterior | Brass Wire | softer than the nozzle it cleans, so it lifts the deposit and not the metal |
| Hardened steel or plated nozzles | Copper Wire | softer still, for alloys a brass brush would still mark |
| Cooled heater block and surrounding parts | Nylon PA | safe around wiring and thermistor leads once the hot end is off |
The constraints this application puts on the filament:
| Constraint | Value for this application |
|---|---|
| Filament hardness | Medium–Hard |
| Maximum service temperature | 300°C |
| Chemical exposure | No Added Medium; Isopropyl Alcohol; Acetone (according to Printing-Material Compatibility) |
| Cleaning method | Dry Brushing, Wet Brushing |
How do I choose the right brush for my 3d printer nozzle equipment?
Nozzle bore caps the tool, hot-end material caps the fill, and the temperature at cleaning decides what survives the contact.
Work through it in this order:
- Identify the target part and measure the access opening or clearance
- Describe the residue: what it is, how thick it sits, and how strongly it holds
- Choose the construction that can physically reach that target
- Set the filament from surface risk, working temperature and cleaning chemistry
- Fix filament diameter, free trim length and density for the contact pressure you need
- Run one cycle and check the result before committing to a production quantity
Before you commit to a quantity, send the nozzle bore, the hot-end material, and the temperature at which cleaning happens.
When is a 3D printer nozzle brush the wrong tool?
A cold pull, a purge with cleaning filament or a solvent soak clears the melt zone from the inside, which is usually where the problem sits. A nozzle worn oversize or with a damaged orifice is replaced, because it is a consumable rather than a repairable part.
What common mistakes should I avoid in 3D Printer Nozzle Cleaning?
- Ordering by printer model instead of nozzle bore and the temperature at which cleaning happens
- Changing brush material while leaving excessive engagement, poor alignment, or no discharge path unchanged
- Copying a worn brush without recording motion, direction, mounting, and the original working diameter
When a brush is running but not cleaning, start here rather than adding pressure:
| Symptom | What to change |
|---|---|
| Residue remains | Increase relative motion or discharge, then change filament diameter or density; do not add pressure before checking loading by oil, carbon, scale, biofilm, process residue, and particles. |
| Surface marks or scratches | Reduce engagement, use finer or softer fill, and remove trapped abrasive particles from contact with bores, channels, tubes, hoses, ports, and internal passages. |
| Rapid wear or uneven cleaning | Check alignment, runout, support, motion, temperature, chemical attack, and whether the brush covers the complete working path. |
| Brush loads or redeposits residue | Open the fill pattern or add wash, vacuum, air, scraping, or a collection path so removed oil, carbon, scale, biofilm, process residue, and particles leaves the contact zone. |
Continue Exploring
Recommended Reading & Related Brush Resources
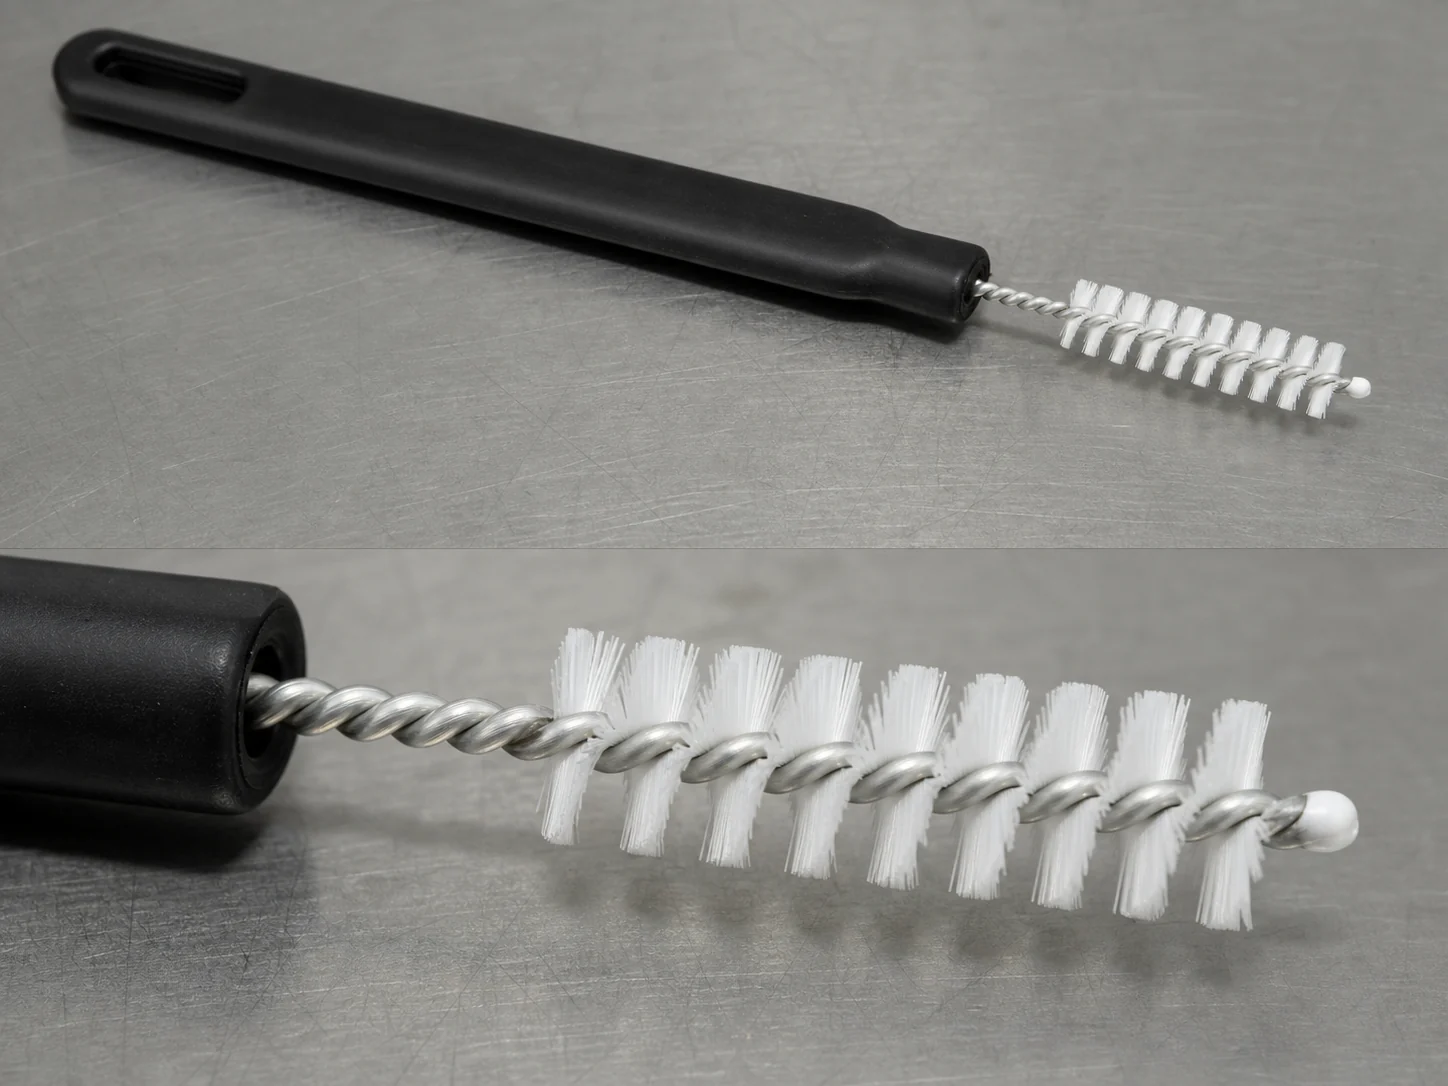
3D Printer Nozzle Cleaning Brush
Clean external 3D printer nozzles, heat blocks, and hotend parts with this brass wire…
See the specification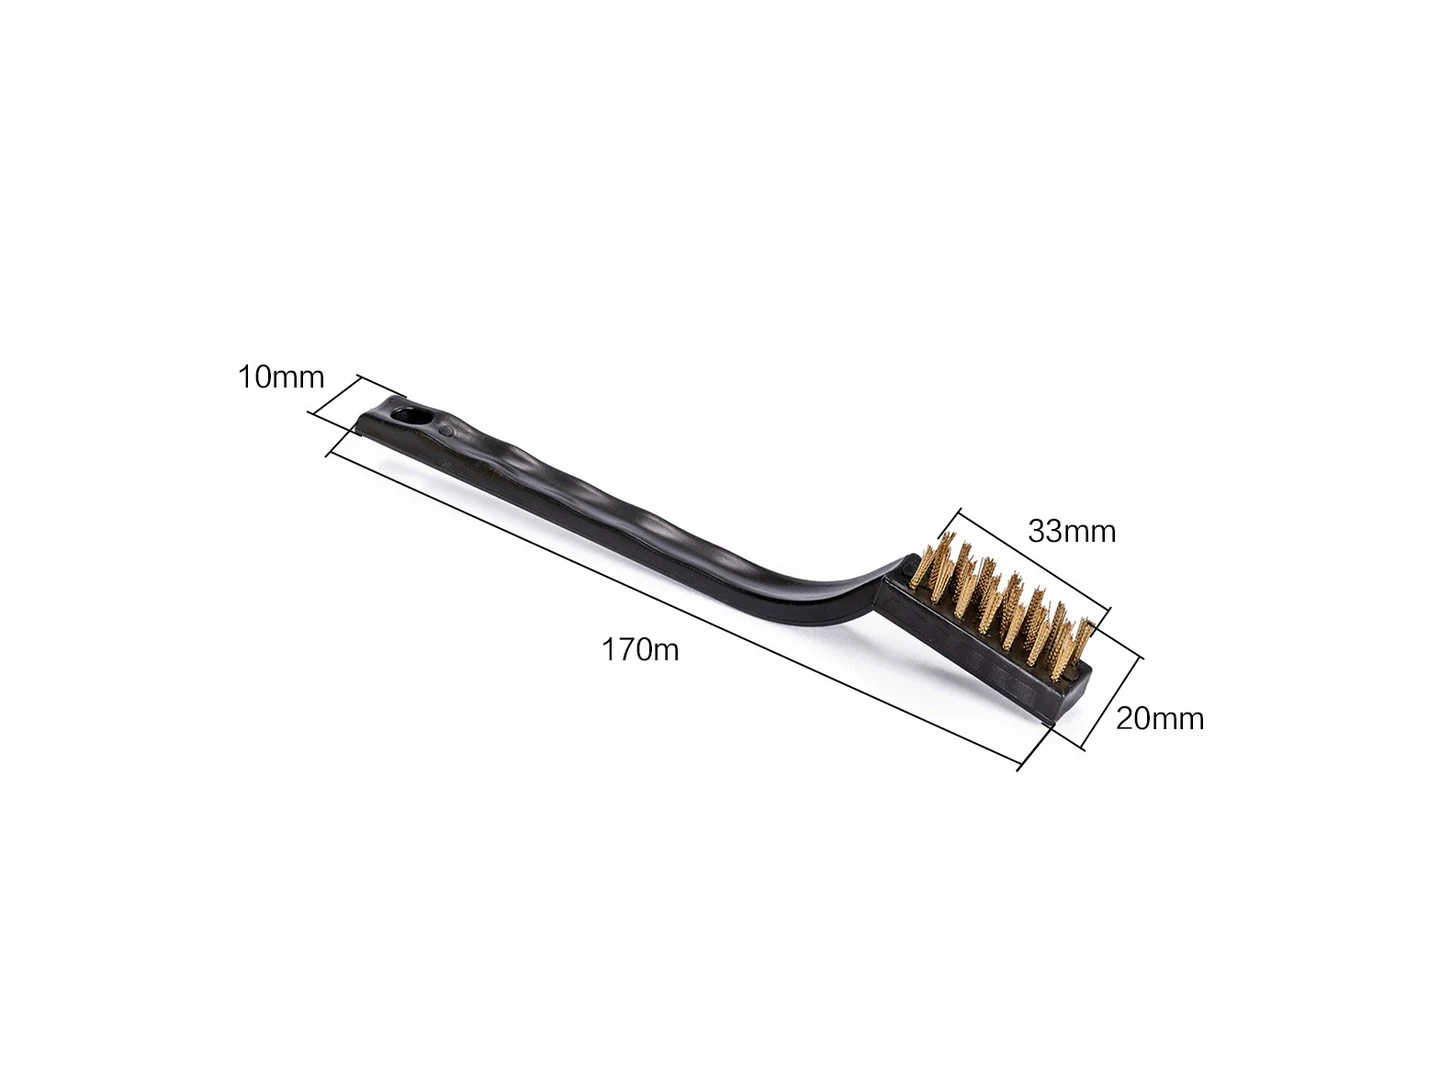
3D Printer Nozzle Brush
Small brass-wire 3D printer nozzle brush for hotend and heater-block cleaning at 200–250°C. Customizable…
See the specification
Inkjet Nozzle Cleaning Brush
Custom inkjet nozzle cleaning brush with PBT or PTFE filaments, 2–6 mm tip, 100–150…
See the specification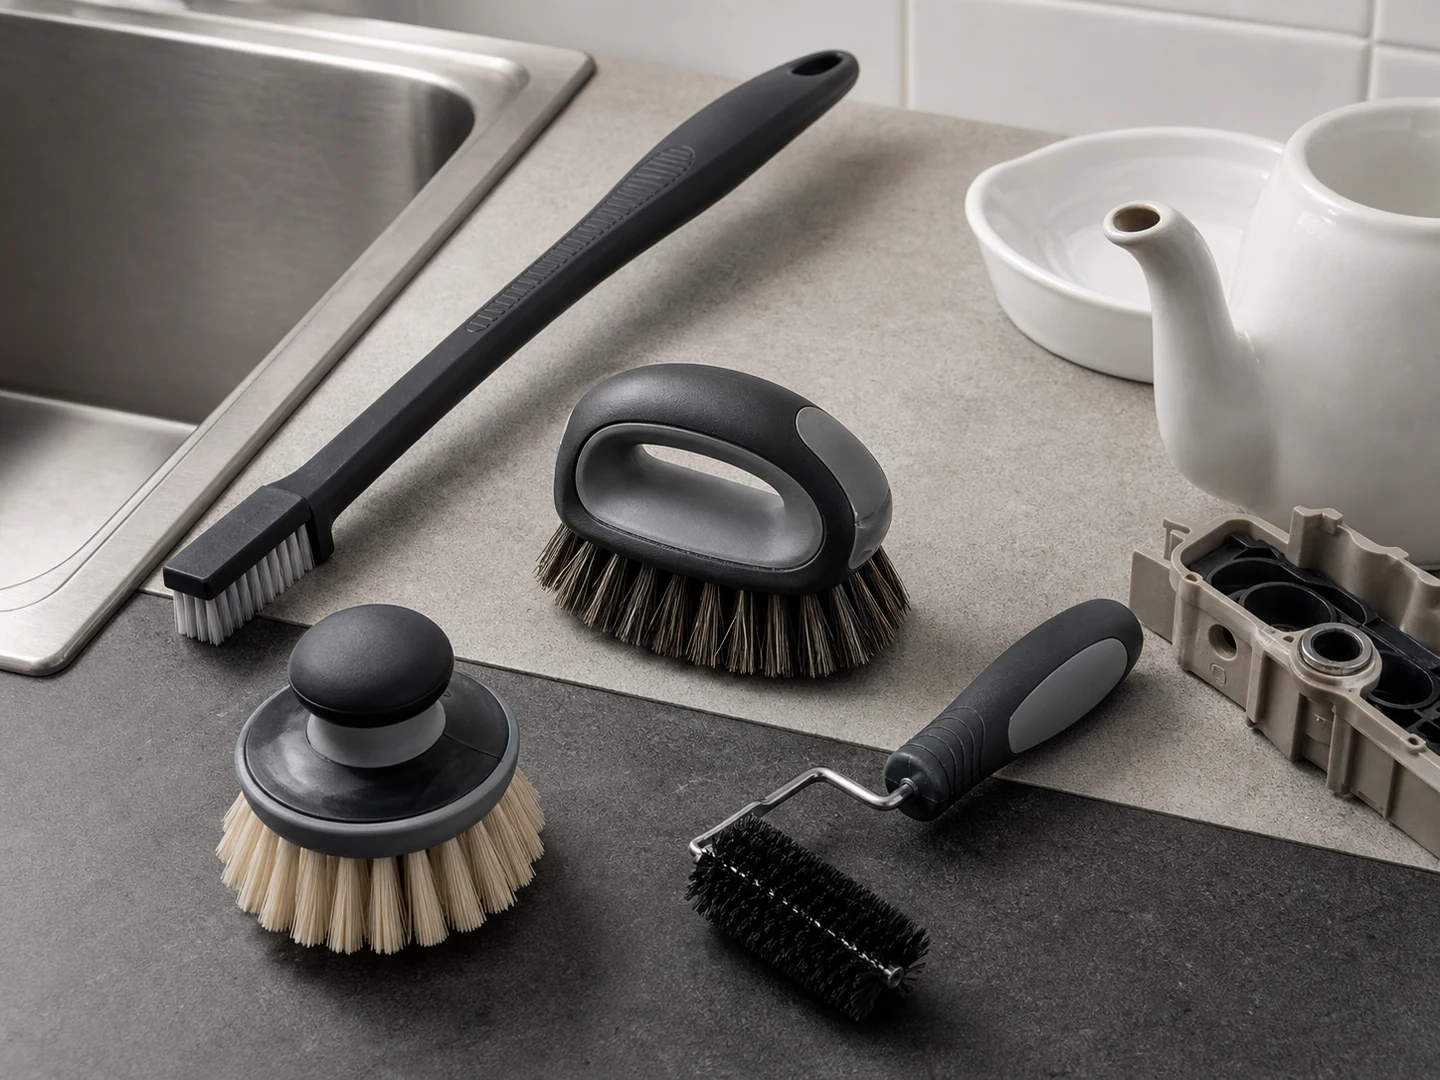
Custom Handheld Detail Brushes
Choose a handheld detail brush when you need direct control in seams, recesses, fittings,…
See how this type is built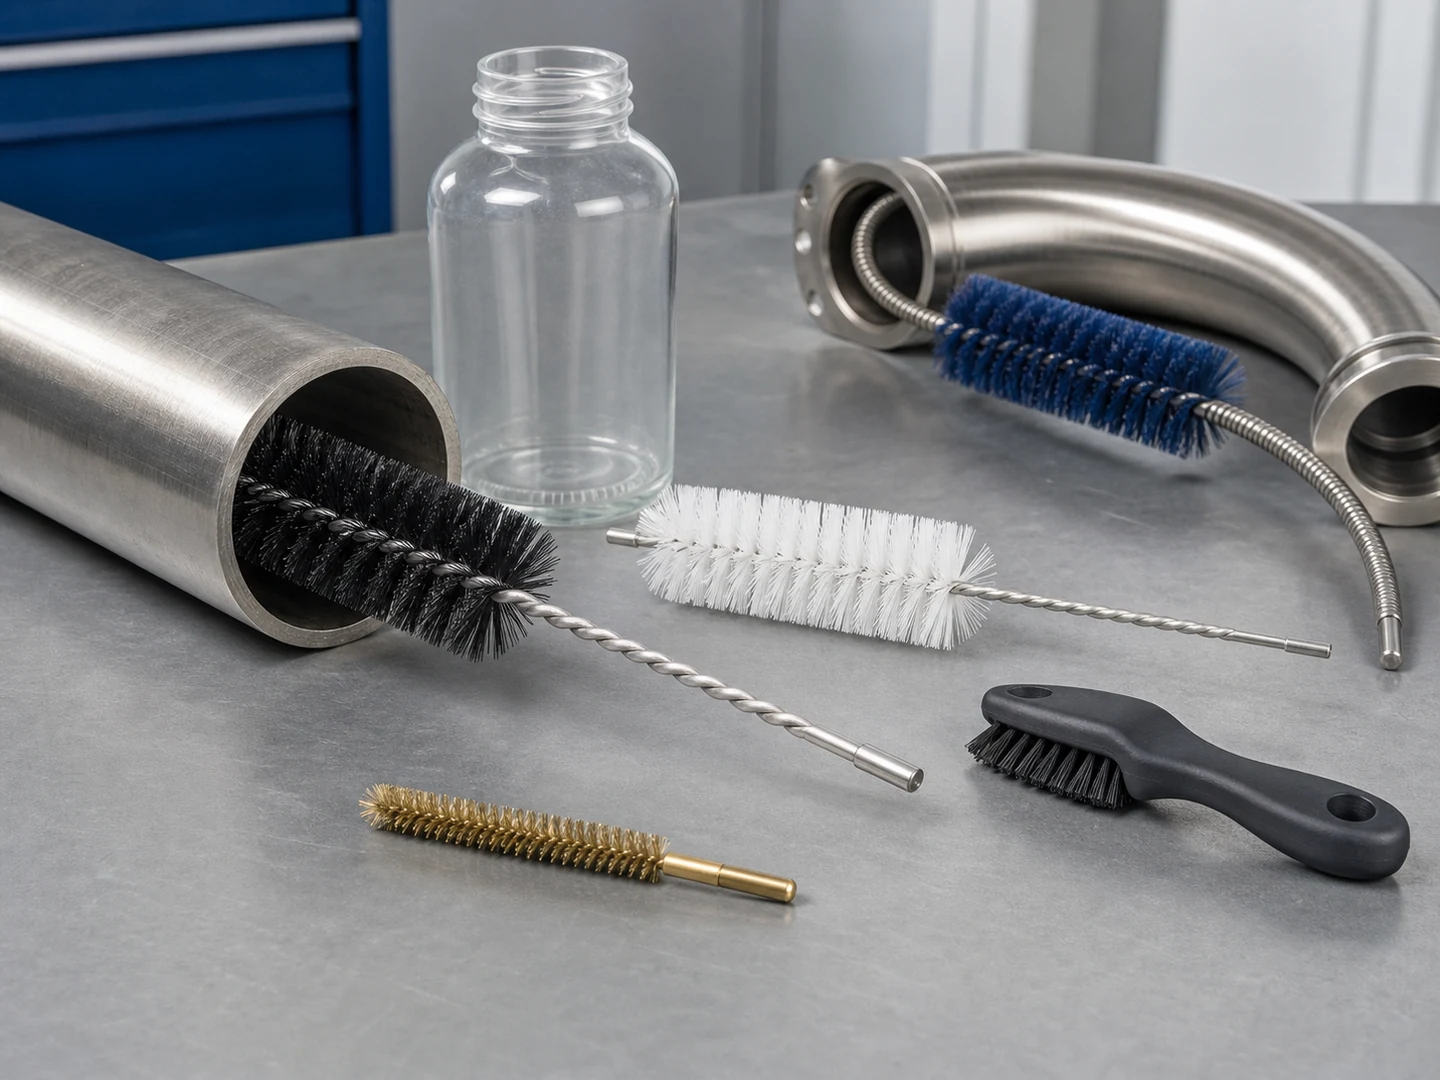
Custom Tube & Pipe Bore Brushes
Choose a tube, pipe, or bore brush when the working surface is inside a…
See how this type is built
Nylon PA
Choose Nylon PA based on its stiffness, recovery, wear, wet-service, chemical, and temperature behavior.
Compare this material
Brass Wire
Choose Brass Wire based on its stiffness, recovery, wear, wet-service, chemical, and temperature behavior.
Compare this material
Copper Wire
Choose Copper Wire based on its stiffness, recovery, wear, wet-service, chemical, and temperature behavior.…
Compare this materialCustom Manufacturing RFQ
Discuss This Application
Share the working surface, residue, dimensions, material direction, interface, quantity and drawing or sample photo.
Custom Brush RFQ
Request a Custom Cleaning Brush Quote
Upload a drawing, product photo, or sample photo and provide the core dimensions and cleaning conditions.
“We need a brush to remove wet residue from a stainless steel conveyor, about 800mm wide. The current brush wears quickly. We can send photos.”
“We sell drinkware and need a cleaning brush to include with the product. Quantity around 5,000 pieces.”