
Application
Industrial Machine Cleaning
For Industrial Machine Cleaning, the brush must reach the working area, disturb or collect cement dust/caked deposits/fine particles, and release it without creating unacceptable surface damage or process interference. Access space, brush movement, and cleaning method are the main factors in selecting the structure.
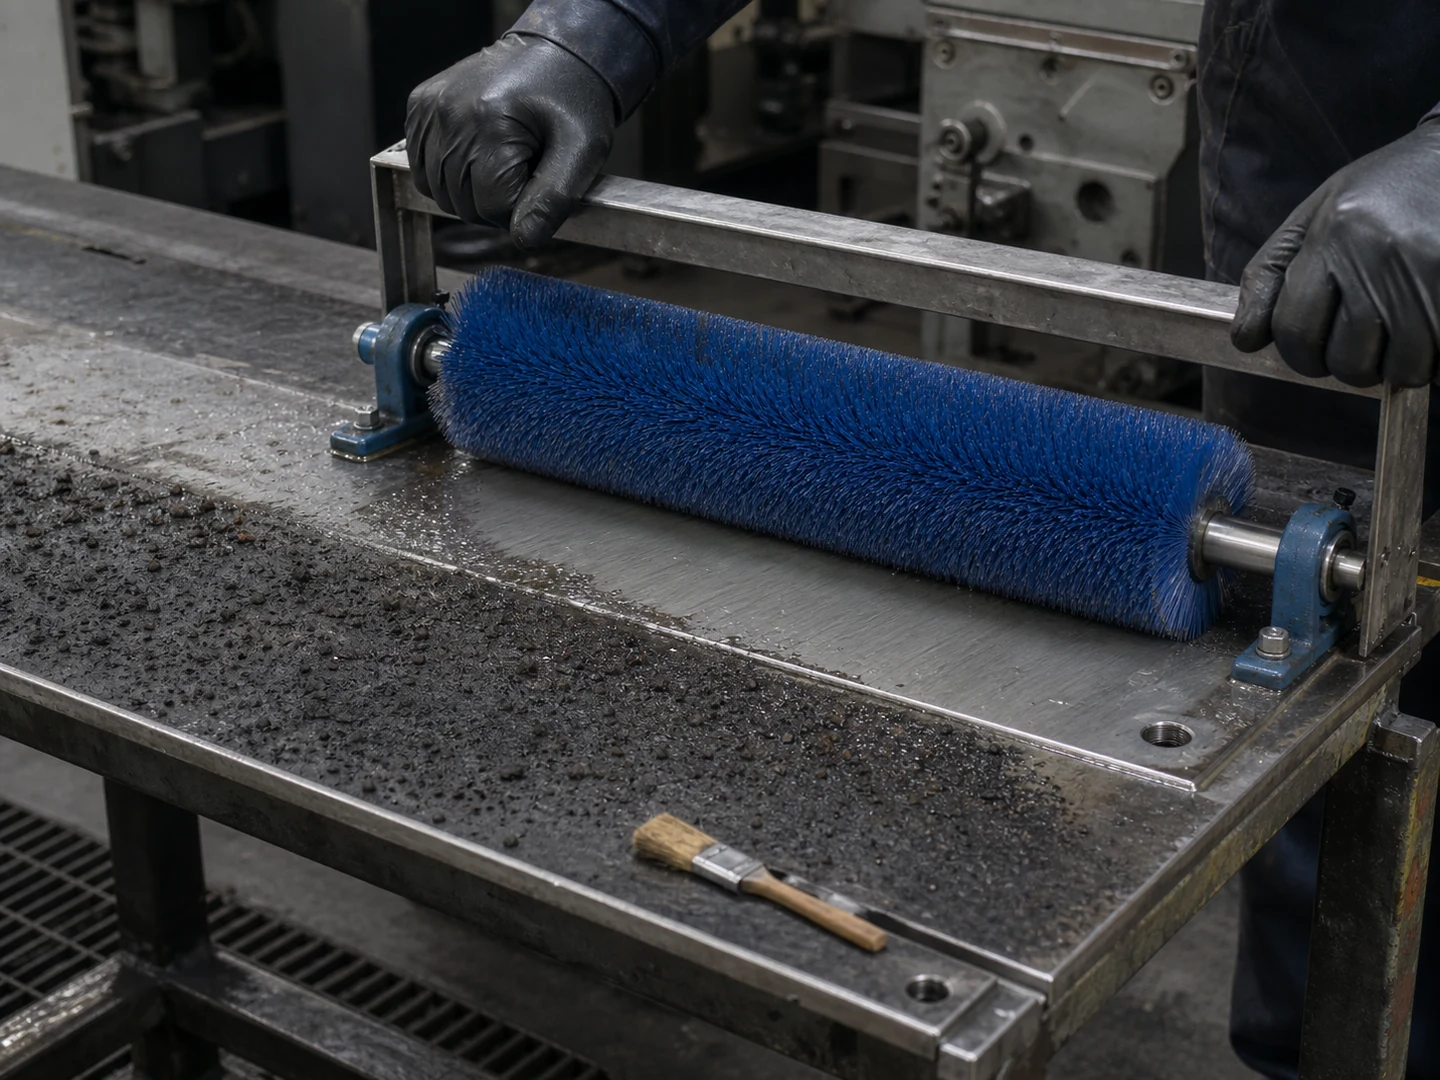
At a glance
- Cleaning target
- Cement Dust/Caked Deposits/Fine Particles
- Working environment
- Dry Indoor Area / Hazardous Area
- Cleaning method
- Dry Brushing / Wet Brushing
- Requirements to check
- Combustible-Dust Explosion Protection / Occupational-Exposure Control; Machinery-Safety SOP
Machine cleaning is contact-zone work — ways, guards, rollers and lubrication ports each present a different access shape, and the brush changes with that shape long before it changes with the deposit.
What makes Industrial Machine Cleaning different from other industrial and manufacturing cleaning?
The main difficulty is removing carryback, powder, fibers, chips, sticky product, and scale from belts, screens, drums, rollers, guides, and machine surfaces without damaging the surface, loading the brush, or carrying contamination back into the process.
The work happens in dry indoor area and hazardous area against cement dust, caked deposits and fine particles.
The part people get wrong: the residue tells you the filament, but the access opening tells you the construction. Get them in that order and the shortlist is short.
What are the most common cleaning targets in Industrial Machine Cleaning?
5 targets, each with its own opening, residue and contact requirement.
| Part or area | Residue type | Cleaning requirement |
|---|---|---|
| Machine Bed and Way | Chips, coolant film, oil, caked fine particles | The head must reach the working face and apply even contact without marking the surface. |
| Guard and Enclosure | Airborne dust, chips, coolant mist deposits | The strip must run the full length of the gap and keep light, continuous contact without binding. |
| Roller and Feed-System | Adhering powder, fines, oil film, product carryover | The brush must span the working width and hold even contact along the whole face while the surface moves under it. |
| Lubrication-Port and Crevice | Grit, hardened grease, dust and swarf packing | The head must be narrower than the opening and stiff enough to lift residue without splaying at the mouth. |
| Chip and Swarf Removal | Oil, grease and adhering swarf | The head must reach the working face and apply even contact without marking the surface. |
What the equipment leaves you to work inside:
| Parameter | Typical range |
|---|---|
| Brush architecture | Roller, strip/lath, plate, hand brush or tube brush selected from the actual access geometry |
| Primary dimensions | Working width/OD/core/shaft or head size are machine-drawing dimensions, not a universal range |
| Fill reference | Nylon 0.05–1.2 mm, PP 0.07–2.0 mm and PBT 0.15–0.2 mm are documented catalog ranges; metal/abrasive fill is used only where the substrate permits |
| ESD | Use conductive construction and a ground path only for static-sensitive zones |
Which brush types work for each cleaning target?
Hand brush, strip, cylinder, disc, tube or machine-specific attachment based on the contact zone.
| Cleaning target | Recommended brush type | Why it fits |
|---|---|---|
| Machine Bed and Way | Handheld Detail Brushes | Dust cakes on the bed and gets dragged under the slide, so a hand-guided head clears it off the way surfaces before the machine is cycled again. |
| Guard and Enclosure | Strip Seal Brushes | Here the brush is fitted rather than carried: a strip along the guard edge keeps dust out of the enclosure without stopping the door from moving. |
| Roller and Feed-System | Roller and Conveyor Brushes | Feed rollers pick dust up and put it back down again, so a brush in constant contact with the roller keeps the transferring surface clean while it runs. |
| Lubrication-Port and Crevice | Handheld Detail Brushes | A grease point collects grit that the gun would push straight into the bearing, so a narrow head clears the fitting before it is coupled. |
| Chip and Swarf Removal | Oily swarf clings and will not blow off, so a hand-guided head sweeps it into a pan instead of putting it into the air. |
How the brush is usually carried on the machine:
- Driven brush — use when carryback, powder, fibers, chips, sticky product, and scale needs repeatable scrubbing or controlled relative movement
- Passive or free-running brush — use for loose contamination and lower process complexity on belts, screens, drums, rollers, guides, and machine surfaces
- Localized hand, strip, or tube brush — use where only an edge, gap, port, or maintenance point needs contact
In practical brush terms: match the construction to the access before anything else. A geometry that cannot reach the target will not be rescued by a better filament.
What filament materials work best for Industrial Machine Cleaning?
Nylon/PBT/PP for general cleaning; wire or abrasive for approved metal finishing; conductive or chemical-resistant grades where documented.
| If the condition is… | Filament to start with | Why |
|---|---|---|
| Sensitive or coated surface | Nylon PA | balanced flex life and abrasion resistance |
| Wet, washdown, or detergent service | Polypropylene PP | acid, alkali, water, and detergent resistance |
| Bonded residue or aggressive cleaning | Abrasive Nylon | controlled cutting without loose wire |
What the duty rules out before you start comparing grades:
| Constraint | Value for this application |
|---|---|
| Filament hardness | Hard |
| Maximum service temperature | 100°C |
| Chemical exposure | No Added Medium; Becomes Strongly Alkaline After Contact with Water pH 11–13 |
| Cleaning method | Dry Brushing, Wet Brushing |
How do I choose the right brush for my industrial machine equipment?
Specify by contact zone rather than by machine — ways, guards, rollers and lubrication ports present different access, so each gets its own brush.
Work through it in this order:
- Identify the target part and measure the access opening or clearance
- Describe the residue: what it is, how thick it sits, and how strongly it holds
- Choose the construction that can physically reach that target
- Set the filament from surface risk, working temperature and cleaning chemistry
- Fix filament diameter, free trim length and density for the contact pressure you need
- Run one cycle and check the result before committing to a production quantity
Before you commit to a quantity, send the dimensions of each contact zone — way, guard, roller, port — and what the deposit is.
When is an industrial machine brush the wrong tool?
Chip conveyors, coolant filtration and vacuum extraction remove the bulk of it; brushing is the finishing pass. And a hot, energised or moving machine is a lockout question before it is a tool question.
What common mistakes should I avoid in Industrial Machine Cleaning?
- Describing the machine instead of the contact zone — a way, a guard and a lubrication port take different brushes
- Changing brush material while leaving excessive engagement, poor alignment, or no discharge path unchanged
- Copying a worn brush without recording motion, direction, mounting, and the original working diameter
If the brush is already in service and the result is wrong, work from the symptom:
| Symptom | What to change |
|---|---|
| Residue remains | Increase relative motion or discharge, then change filament diameter or density; do not add pressure before checking loading by carryback, powder, fibers, chips, sticky product, and scale. |
| Surface marks or scratches | Reduce engagement, use finer or softer fill, and remove trapped abrasive particles from contact with belts, screens, drums, rollers, guides, and machine surfaces. |
| Rapid wear or uneven cleaning | Check alignment, runout, support, motion, temperature, chemical attack, and whether the brush covers the complete working path. |
| Brush loads or redeposits residue | Open the fill pattern or add wash, vacuum, air, scraping, or a collection path so removed carryback, powder, fibers, chips, sticky product, and scale leaves the contact zone. |
Guides that go deeper on this
We have not written a guide specific to this one yet. The material that covers selection, filament, dimensions, maintenance and sourcing is collected in the technical resources library.
Continue Exploring
Recommended Reading & Related Brush Resources
Industrial Filter Element Cleaning Brush
Configure flat, radial, cylindrical, basket, and frame filter cleaning brushes in PBT, PP, or…
See the specification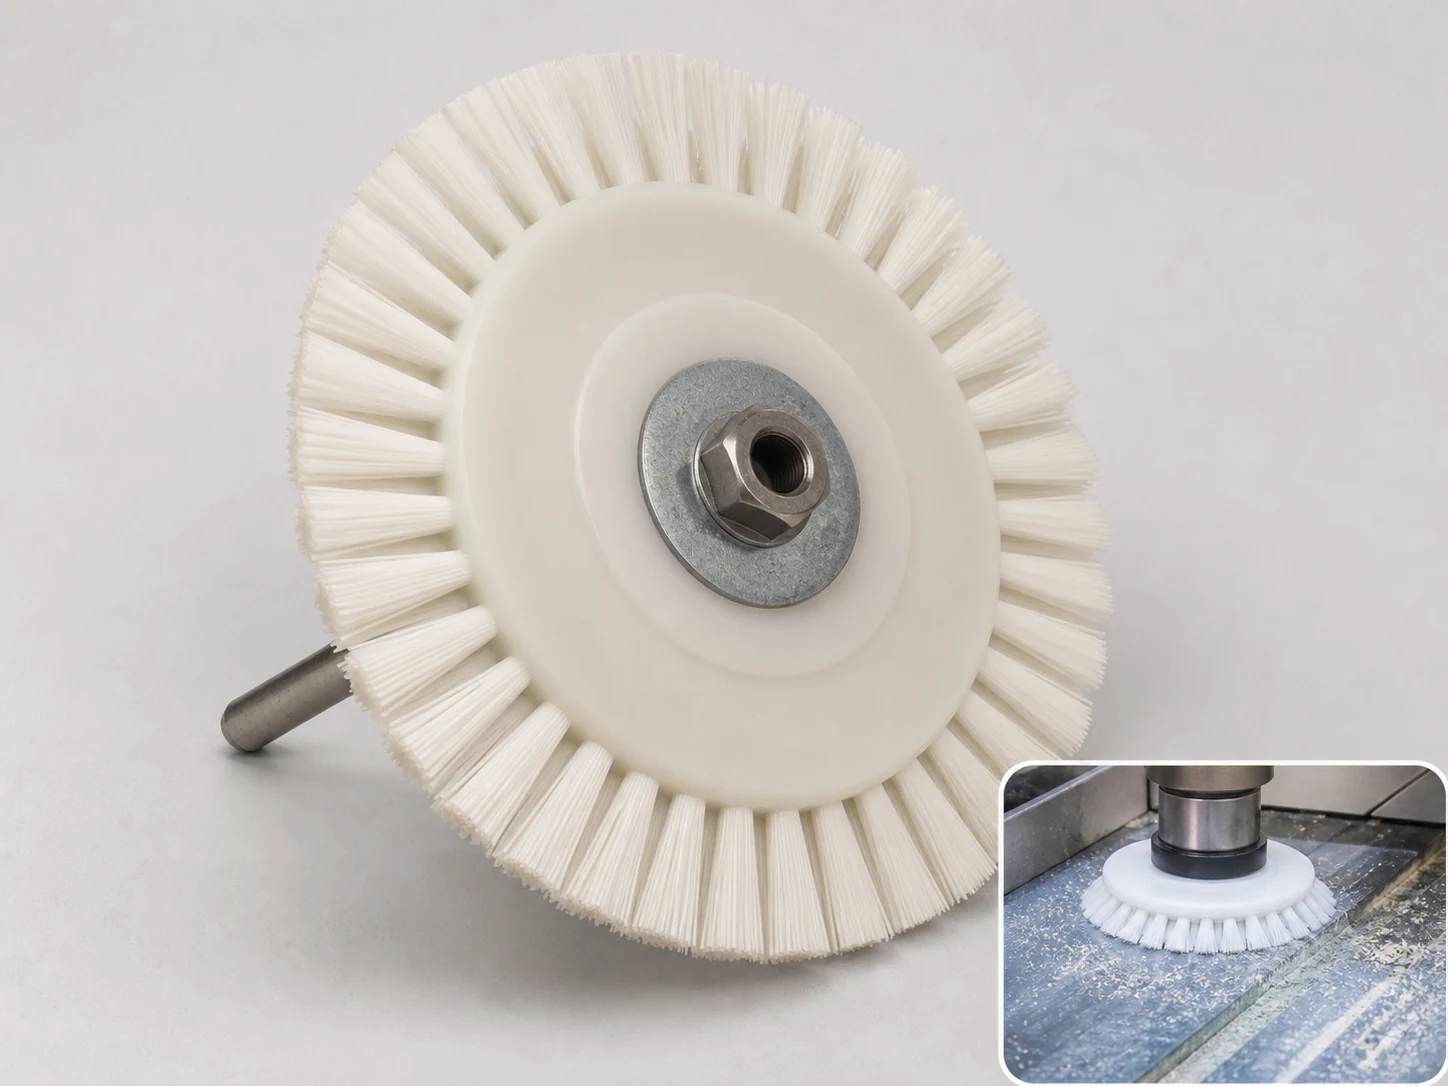
Plastic-Base Industrial Disc Cleaning Brush
Machine-mounted plastic-base disc brush with nylon PA filament for flat-face, edge, and localized cleaning…
See the specification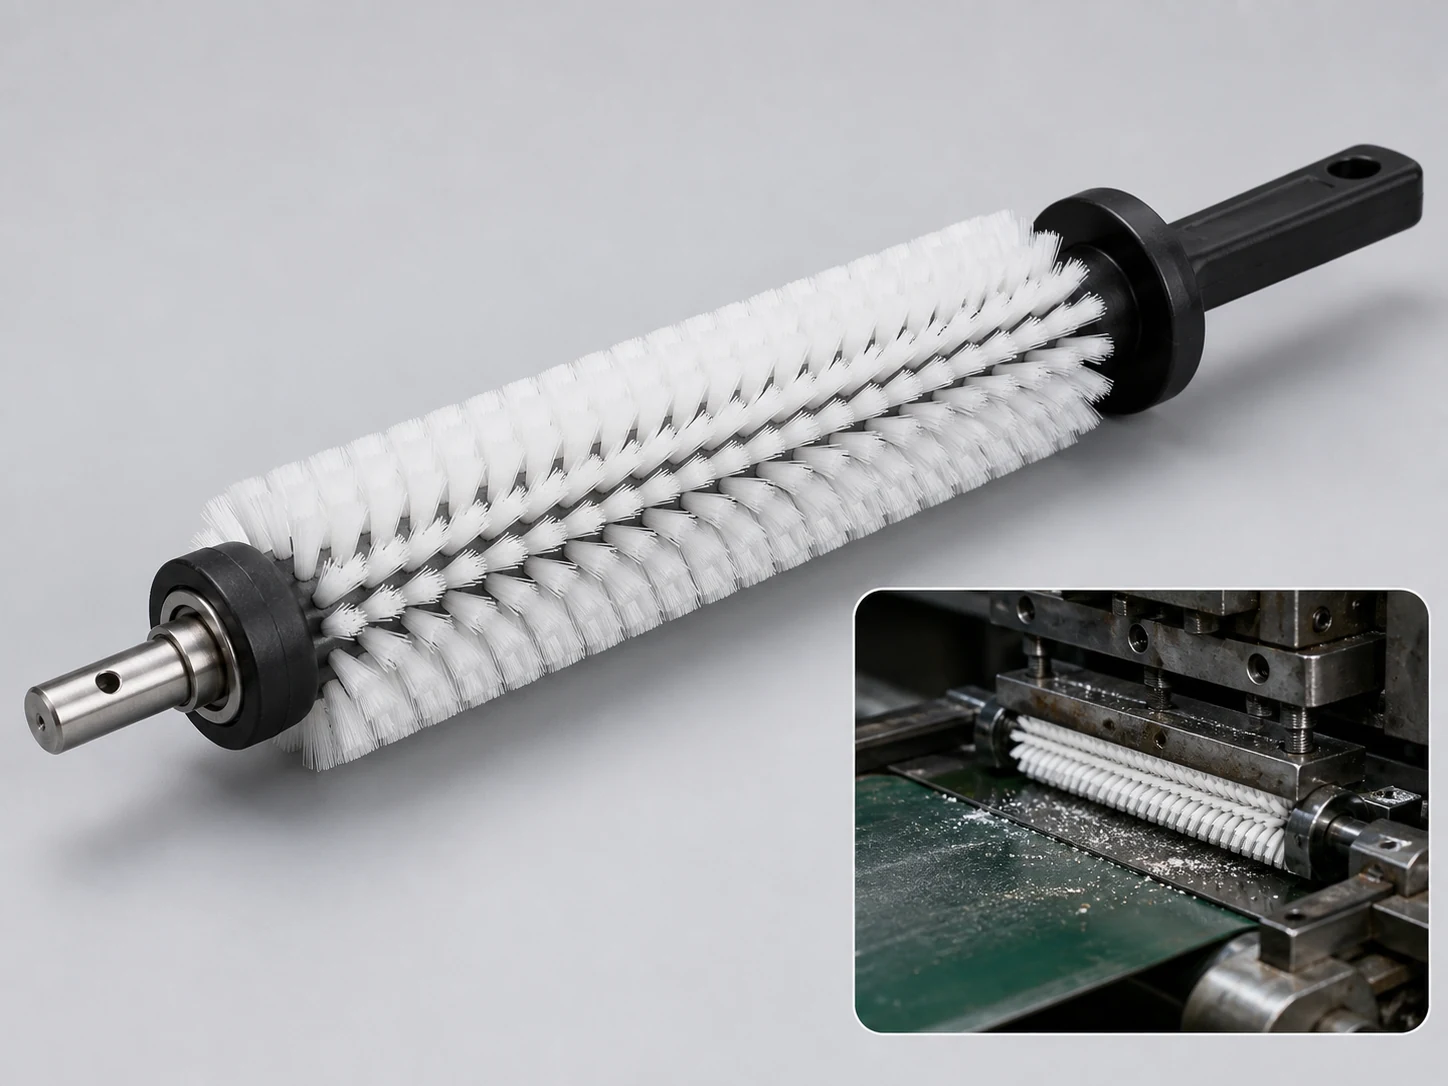
Machine Tool Punch Press
Custom nylon cleaning brush for punch presses. Clears metal chips, slugs, and stamping debris…
See the specification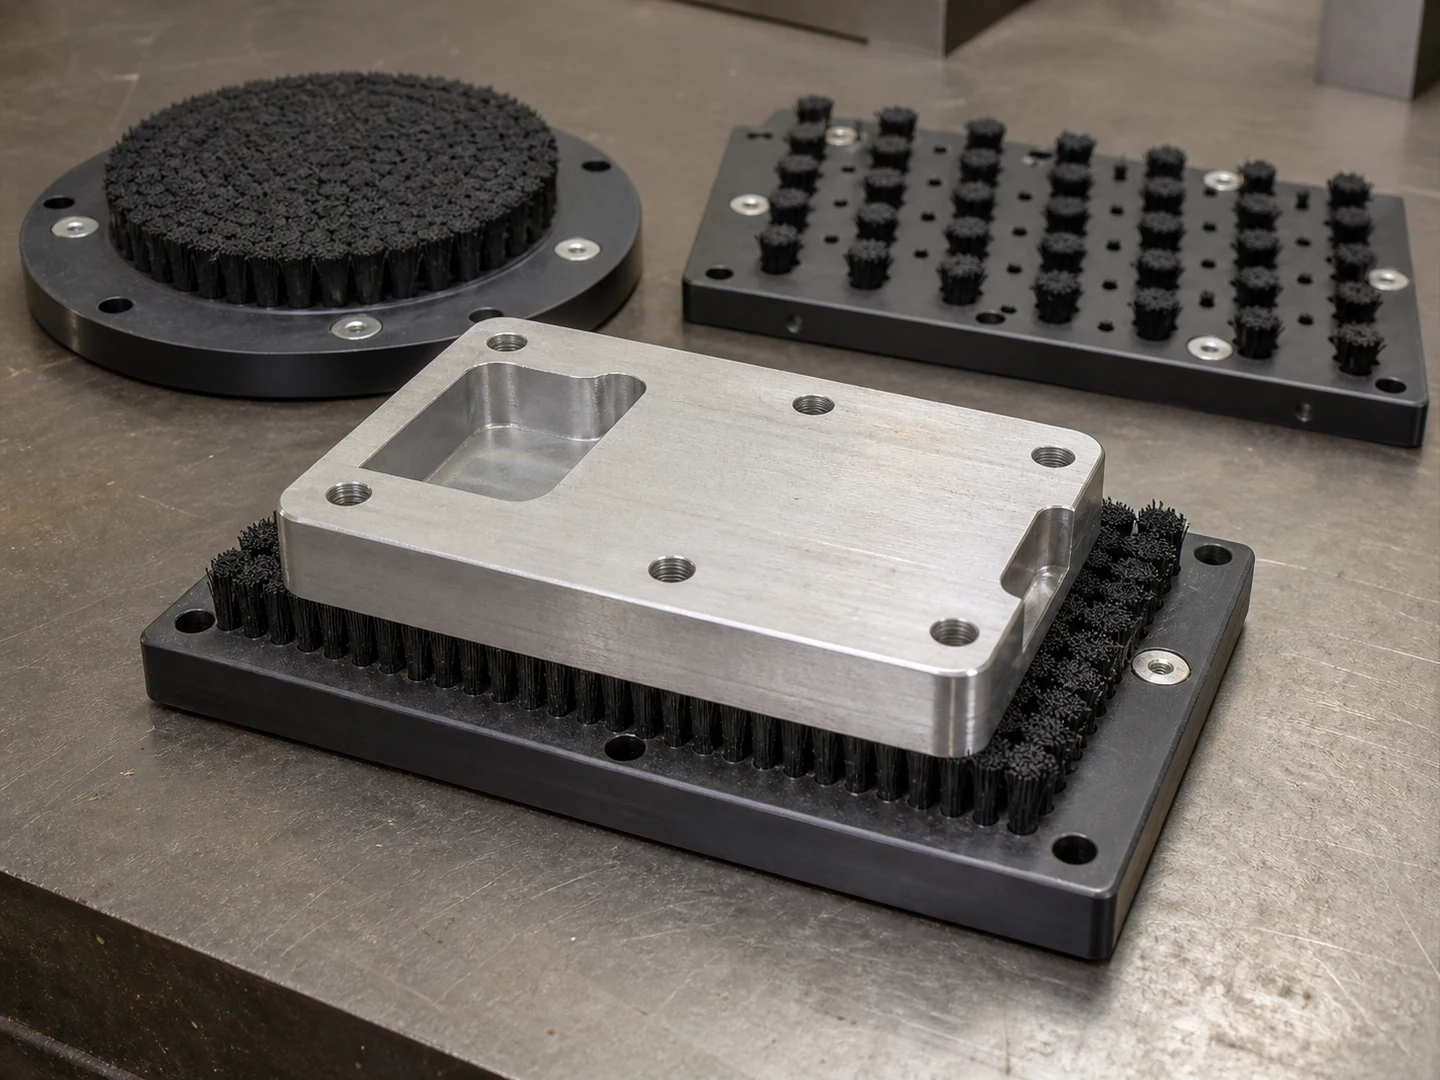
Custom Machine Table Brush Plates
Choose a machine table brush plate when a broad field of bristles must support,…
See how this type is built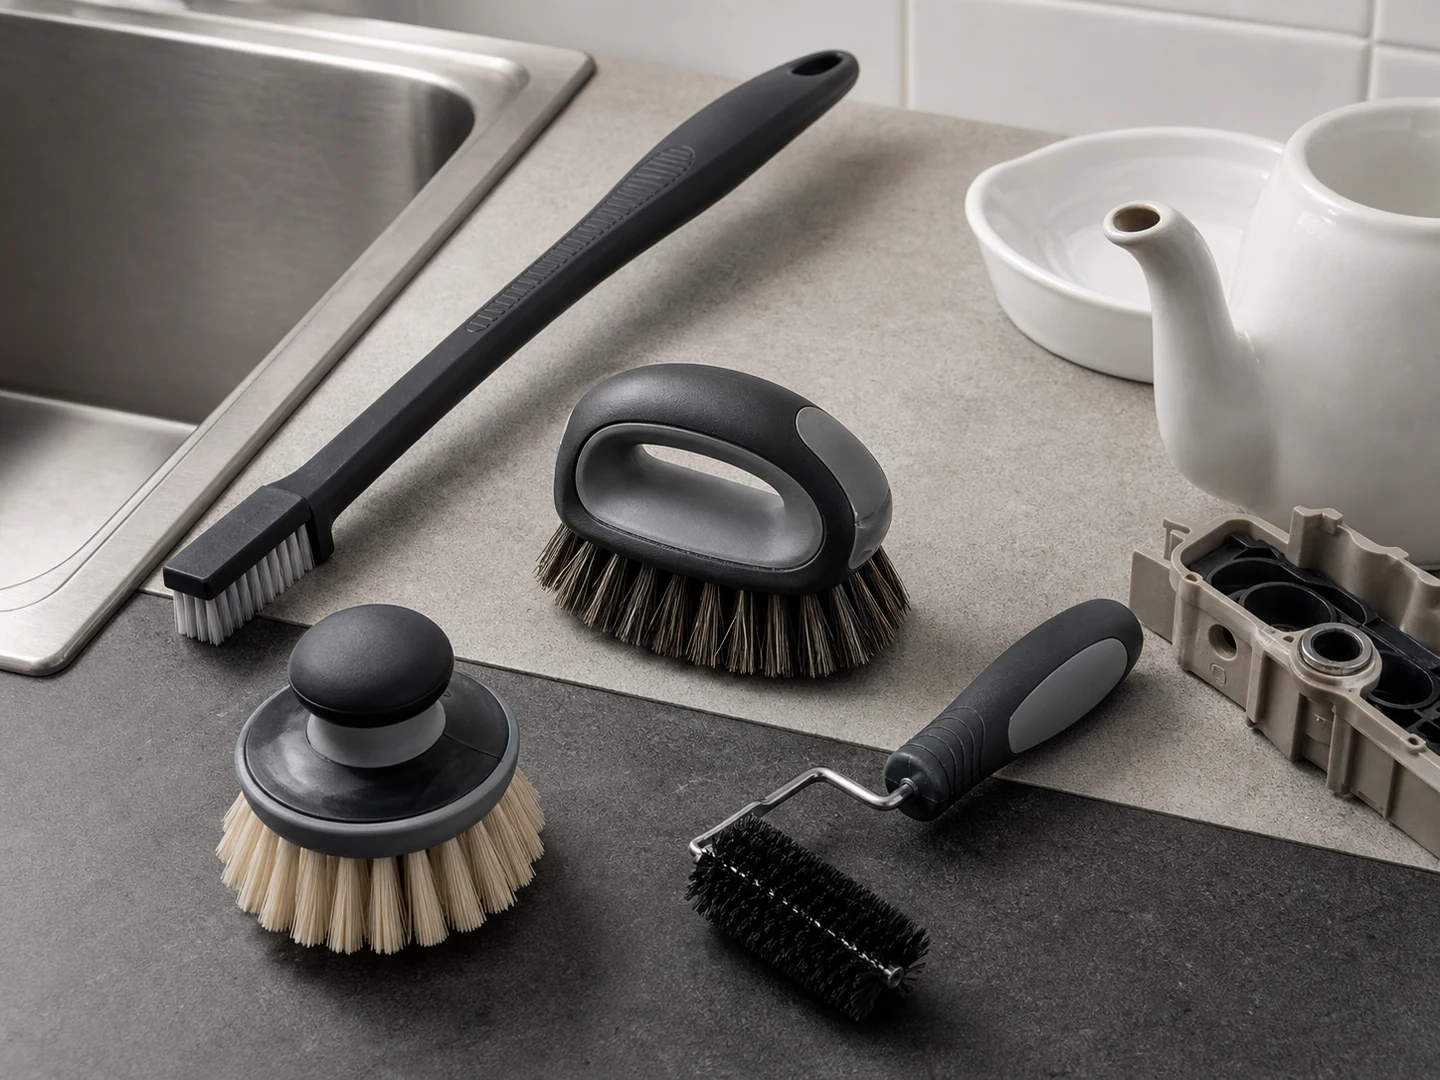
Custom Handheld Detail Brushes
Choose a handheld detail brush when you need direct control in seams, recesses, fittings,…
See how this type is built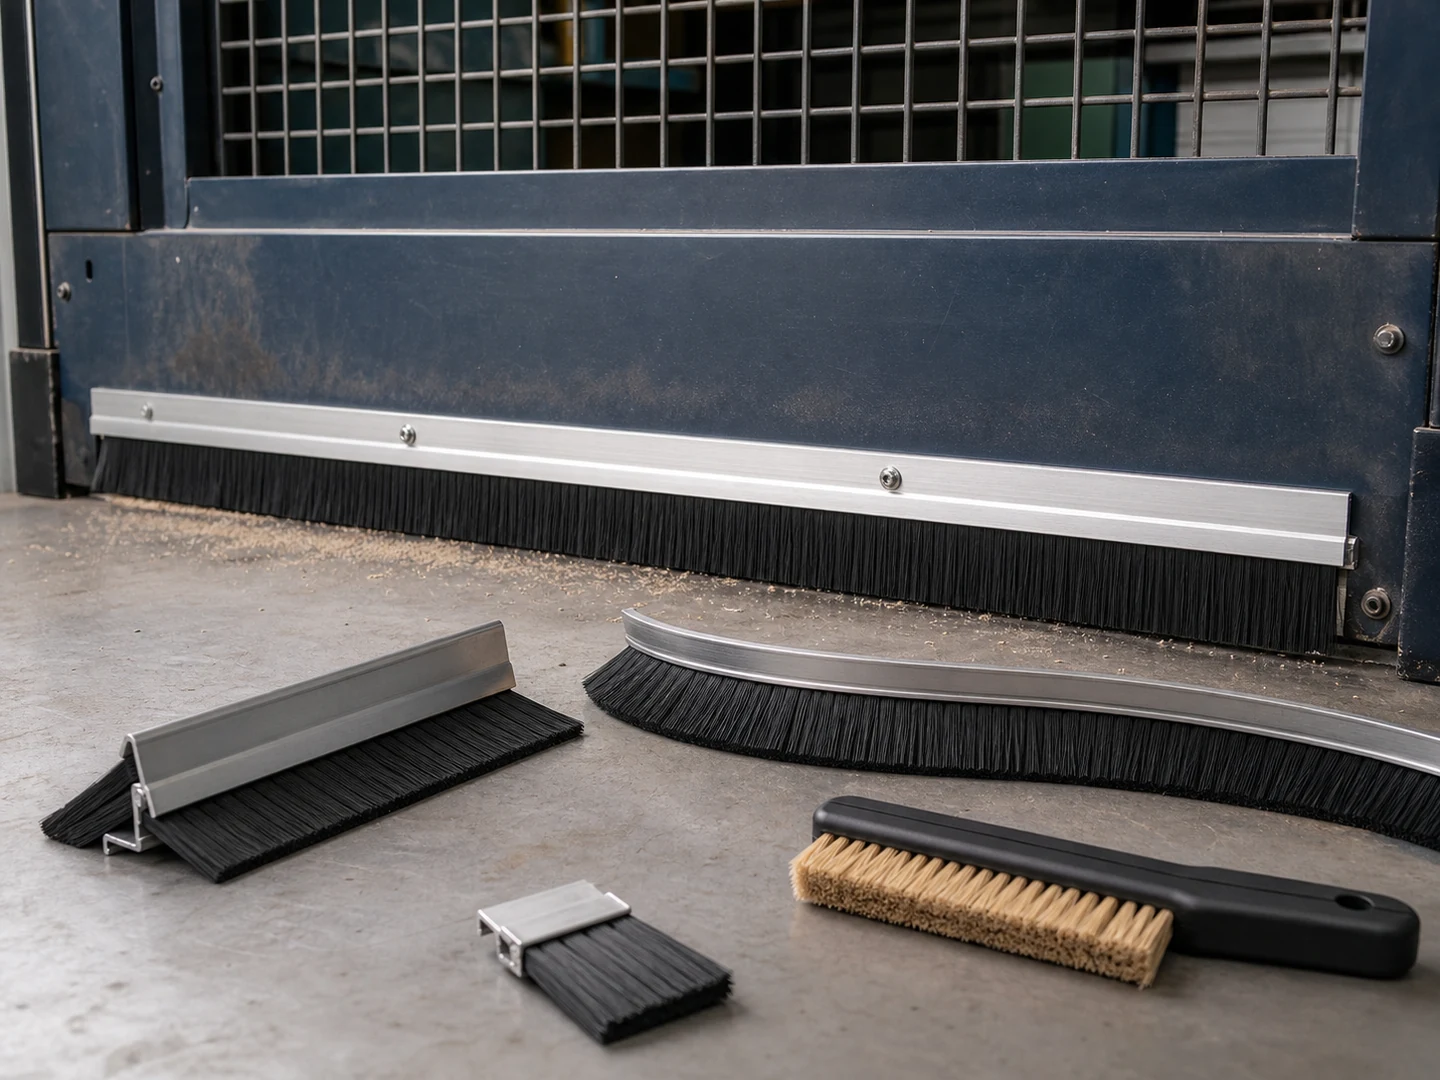
Custom Strip Seal Brushes
Choose a strip seal brush when a continuous line of filament must seal, wipe,…
See how this type is built
Nylon PA
Choose Nylon PA based on its stiffness, recovery, wear, wet-service, chemical, and temperature behavior.
Compare this material
Polypropylene PP
Choose Polypropylene PP based on its stiffness, recovery, wear, wet-service, chemical, and temperature behavior.…
Compare this materialCustom Manufacturing RFQ
Discuss This Application
Share the working surface, residue, dimensions, material direction, interface, quantity and drawing or sample photo.
Custom Brush RFQ
Request a Custom Cleaning Brush Quote
Upload a drawing, product photo, or sample photo and provide the core dimensions and cleaning conditions.
“We need a brush to remove wet residue from a stainless steel conveyor, about 800mm wide. The current brush wears quickly. We can send photos.”
“We sell drinkware and need a cleaning brush to include with the product. Quantity around 5,000 pieces.”