
Material
Aluminum Oxide Abrasive Nylon
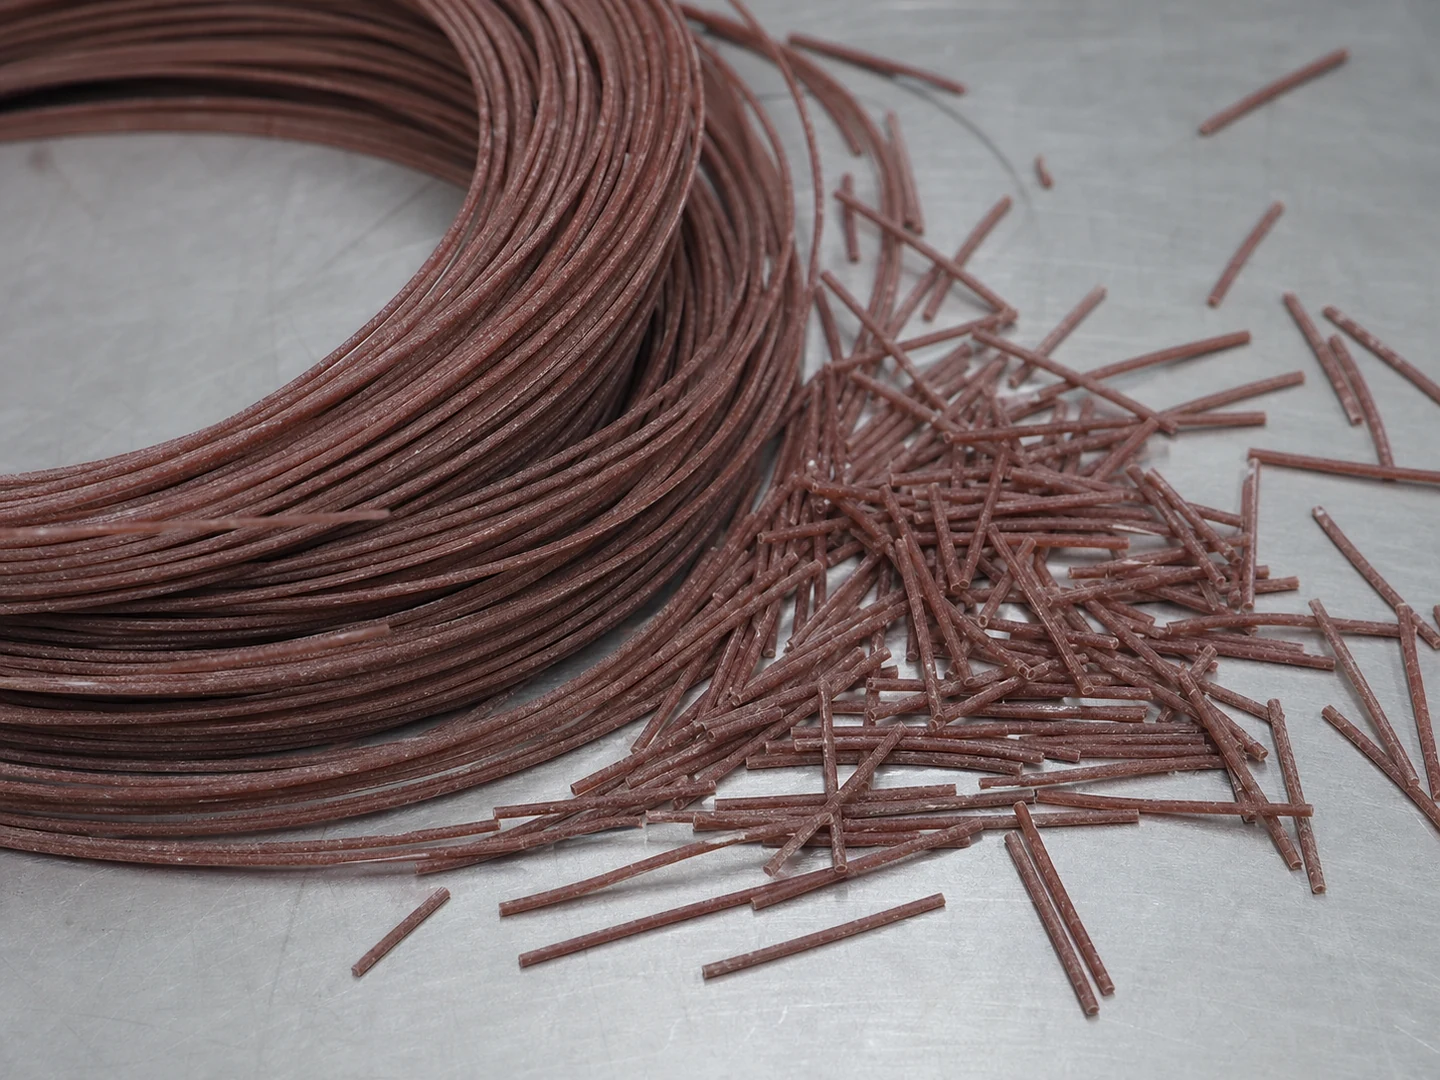
Abrasive-filled polyamide filament
Choose Aluminum Oxide Abrasive Nylon based on its stiffness, recovery, wear, wet-service, chemical, and temperature behavior. To define stiffness, confirm the material together with filament diameter, free trim length, density, grade, and service conditions.
Datasheet values
- Abrasive grit
- 46–600 grit aluminum oxide
- Filament diameter
- 0.20–1.80 mm
- Mohs hardness
- about 9
This abrasive filament distributes aluminum-oxide grit through a nylon base, allowing side and tip contact as the filament flexes.
What is Aluminum Oxide Abrasive Nylon, and what makes it different from other brush filaments?
Aluminum Oxide Abrasive Nylon belongs to the abrasive-filled polyamide filament group, supplied as abrasive filament, drawn in round and rectangular sections and set in straight rows, helical, staggered and zoned fill patterns.
Aluminum Oxide Abrasive Nylon is used in custom cleaning brushes for controlled finishing, cleaning and deburring where a less aggressive cut than silicon carbide is preferred.
The realistic alternatives are Polypropylene PP, PBT and PET Polyester. What separates them here is moisture uptake and working temperature, not headline strength.
Compare Aluminum Oxide Abrasive Nylon with PP, PBT, PET. Change material when wet stiffness, temperature, chemical resistance, conductivity, particle shedding, or surface marking becomes the limiting factor.
What stiffness and contact pressure can I expect from Aluminum Oxide Abrasive Nylon?
Aluminum Oxide Abrasive Nylon is abrasive filament; abrasive grit commonly 46#-5000# and filament diameter 0.3-2.5mm in MW abrasive filament data. It Aluminum Oxide Abrasive Nylon changes brush stiffness through filament diameter, free trim, density, crimp, and contact. Use finer filament and longer trim for conformable contact; use coarser filament, shorter trim, or higher density for stronger displacement or cutting.
Published ranges for the filament itself. Read them as a shortlist tool, not as brush performance.
| Property | Aluminum Oxide Abrasive Nylon | Polypropylene PP | PBT | PET Polyester |
|---|---|---|---|---|
| Shore hardness | Carrier Shore D 70–85; Al2O3 Mohs Hardness Approximately 9 | Shore D 65–75 | Shore D 80–90 | Shore D 80–90 |
| Continuous temperature (°C) | 80–120 | 80–100 | 120–140 | 120–150 |
| Peak temperature (°C) | 140–170 | 120–140 | 160–180 | 170–190 |
| Water absorption, 24 h | 0.3–2.0% (Depending on Nylon Carrier, ISO 62/ASTM D570) | ≤0.03% (24h, ISO 62/ASTM D570) | 0.05–0.20% (24h, ISO 62/ASTM D570) | 0.10–0.30% (24h, ISO 62/ASTM D570) |
| Filament diameter (mm) | 0.15–2.50 | 0.08–3.00 | 0.03–2.00 | 0.04–1.50 |
| Flexibility | Low to Medium Flexibility | Medium Flexibility | Medium to High Flexibility | Medium Flexibility |
The part people get wrong: stiffness is not a property of the material on its own. A 0.50 mm filament on a 15 mm trim is stiffer than a 0.30 mm filament on a 25 mm trim in the same grade. Fix diameter and trim first, then confirm the material.
How does water affect Aluminum Oxide Abrasive Nylon performance?
Aluminum Oxide Abrasive Nylon takes up 0.3–2.0% (Depending on Nylon Carrier, ISO 62/ASTM D570).
PA6 and PA66 absorb moisture; PA610, PA612 and PA12 retain stiffness better in wet service; this moisture response matters in controlled finishing, cleaning and deburring where a less aggressive cut than silicon carbide is preferred.
What this means for your application: the filament grows and softens as it takes on water, and tip pressure goes with it. The reach you measured dry is not the reach you get wet.
A practical check: run one wet cycle and compare tip contact against the dry state. If the wet brush leaves residue behind or no longer reaches the bottom of the bore, change the material rather than the geometry.
What temperature limits apply to Aluminum Oxide Abrasive Nylon?
Continuous service: 90–120°C.
The filament tables quote 80–120°C continuous and 140–170°C peak. The tighter number above is the one to build to, because a brush is loaded while it is hot.
Where it stops working: validate with a sample if the process sits near the top of that band. If the filament takes a permanent set under load, step up to PET Polyester or PBT, which hold a higher continuous temperature.
Diameter, trim length and applied load all shift the real limit, so a thin filament touching lightly survives conditions that would flatten a thick one under pressure.
What chemicals attack Aluminum Oxide Abrasive Nylon?
It stands up to water, oils, mild detergents and dilute alkalis.
What degrades it: strong mineral acids, phenols and strong oxidizers.
Compatibility is a function of concentration, temperature and contact time together. A short rinse in a dilute solution is a different exposure from an overnight soak in a concentrated one, even with the same chemical on the label.
Before you commit to a quantity: Specify the exact Aluminum Oxide Abrasive Nylon grade or alloy, filament or profile size, color, straight or crimped form, working temperature, wet or dry use, chemical exposure, surface finish, and any required material documentation.
What is the practical lower limit for filament diameter?
The floor is roughly 0.15 mm; finer than that and the filament snaps rather than flexes. In practice you are choosing inside 0.15–2.50 mm.
Free trim runs 5–150 mm, and the two interact: a finer filament needs a shorter trim to keep useful stiffness, while a thicker one carries a longer trim and still lands pressure on the tip.
Split the range by duty: roughly 0.15–0.74 mm for light wiping, dusting and surfaces that mark easily, and 0.74–2.50 mm where residue is packed on and point pressure matters more than surface risk.
Tip treatments available on this filament: cut-to-length, controlled end rounding and resin coupling treatment.
In practical brush terms: reaching deep into a bore or crevice is a diameter problem before it is a length problem. A thicker filament on a moderate trim pushes further in before the tips fold over.
What applications typically use Aluminum Oxide Abrasive Nylon?
Controlled finishing, cleaning and deburring where a less aggressive cut than silicon carbide is preferred.
The applications that keep coming back to this grade:
- Heat Exchanger Tube Cleaning
- Pipe Robot Brush Attachment Use
- Hose Cleaning
- CPAP Hose Cleaning
- Surface Finishing
- Polishing
The constructions that usually carry it:
- Custom Tube & Pipe Bore Brushes
- Custom Cup Brushes
If the sample comes back rejected: Aluminum oxide gives a more controlled cut than silicon carbide but may be too slow for heavy scale or large burrs.
How do I specify Aluminum Oxide Abrasive Nylon for a custom brush?
Send the brush type, filament diameter, free trim length, density, contact setting, wet or dry duty, working temperature and the actual cleaning chemistry together. Any one of them on its own leaves the stiffness undefined.
What usually goes wrong at this step:
- Selecting Aluminum Oxide Abrasive Nylon from the material name alone without setting filament diameter, trim length, and density
- Using dry stiffness to predict wet behavior without checking moisture absorption or liquid exposure
- Ignoring trapped abrasive particles, chemical concentration, temperature, or contact motion when assessing surface risk
Reference standards behind the figures on this page: ISO 527-1:2019; ASTM D638; ISO 62:2008; ASTM D570-22; ISO 868:2003; ASTM D2240-15(2021); ISO 4892-3:2024; ASTM G154-23; UL 94; ISO 6344 series.
Source: Perlon — Abrasive Filaments. Public manufacturer or material data supports the material form and performance direction used on this page.
What else does the datasheet specify for Aluminum Oxide Abrasive Nylon?
| Filament cross-section | Round/Rectangular |
|---|---|
| Electrical behaviour | Insulating |
Questions this page is asked
How should aluminum-oxide abrasive nylon be compared on a specified workpiece?
Use representative alloy or substrate, hardness, coating, geometry and incoming surface, then compare controlled brush settings for removal rate, residual burr or oxide, roughness, edge change, dimensions, temperature and debris. Select by the documented process window and required result rather than assuming aluminum oxide is suitable from the workpiece category alone.
What should trigger replacement of an aluminum-oxide abrasive nylon brush?
Trend the required finish, removal rate, burr or oxide residue, critical dimensions, cycle time, heat and debris at defined intervals together with trim wear and filament loss. Replace or revalidate when the process leaves its acceptance band, even if the brush still rotates normally and shows no obvious broken filaments.
Where these figures come from
| Property | Published value | Source |
|---|---|---|
| Hardness and stiffness | Abrasive filament; abrasive grit commonly 46#-5000# and filament diameter 0.3-2.5mm in MW abrasive filament data. | Evonik Retrieved 2026-07-20 |
| Limitations | Aluminum oxide gives a more controlled cut than silicon carbide but may be too slow for heavy scale or large burrs. | Perlon Retrieved 2026-07-20 |
| Temperature resistance | Continuous service: 90–120°C. | Perlon Retrieved 2026-07-20 |
| Water resistance | PA6 and PA66 absorb moisture; PA610, PA612 and PA12 retain stiffness better in wet service; this moisture response matters in controlled finishing, cleaning and deburring where a less aggressive cut than silicon carbide is preferred. | Evonik Retrieved 2026-07-20 |
| Material definition | This abrasive filament distributes aluminum-oxide grit through a nylon base, allowing side and tip contact as the filament flexes. | Perlon Retrieved 2026-07-20 |
Guides that go deeper on this
We have not written a guide specific to this one yet. The material that covers selection, filament, dimensions, maintenance and sourcing is collected in the technical resources library.
Continue Exploring
Recommended Reading & Related Brush Resources
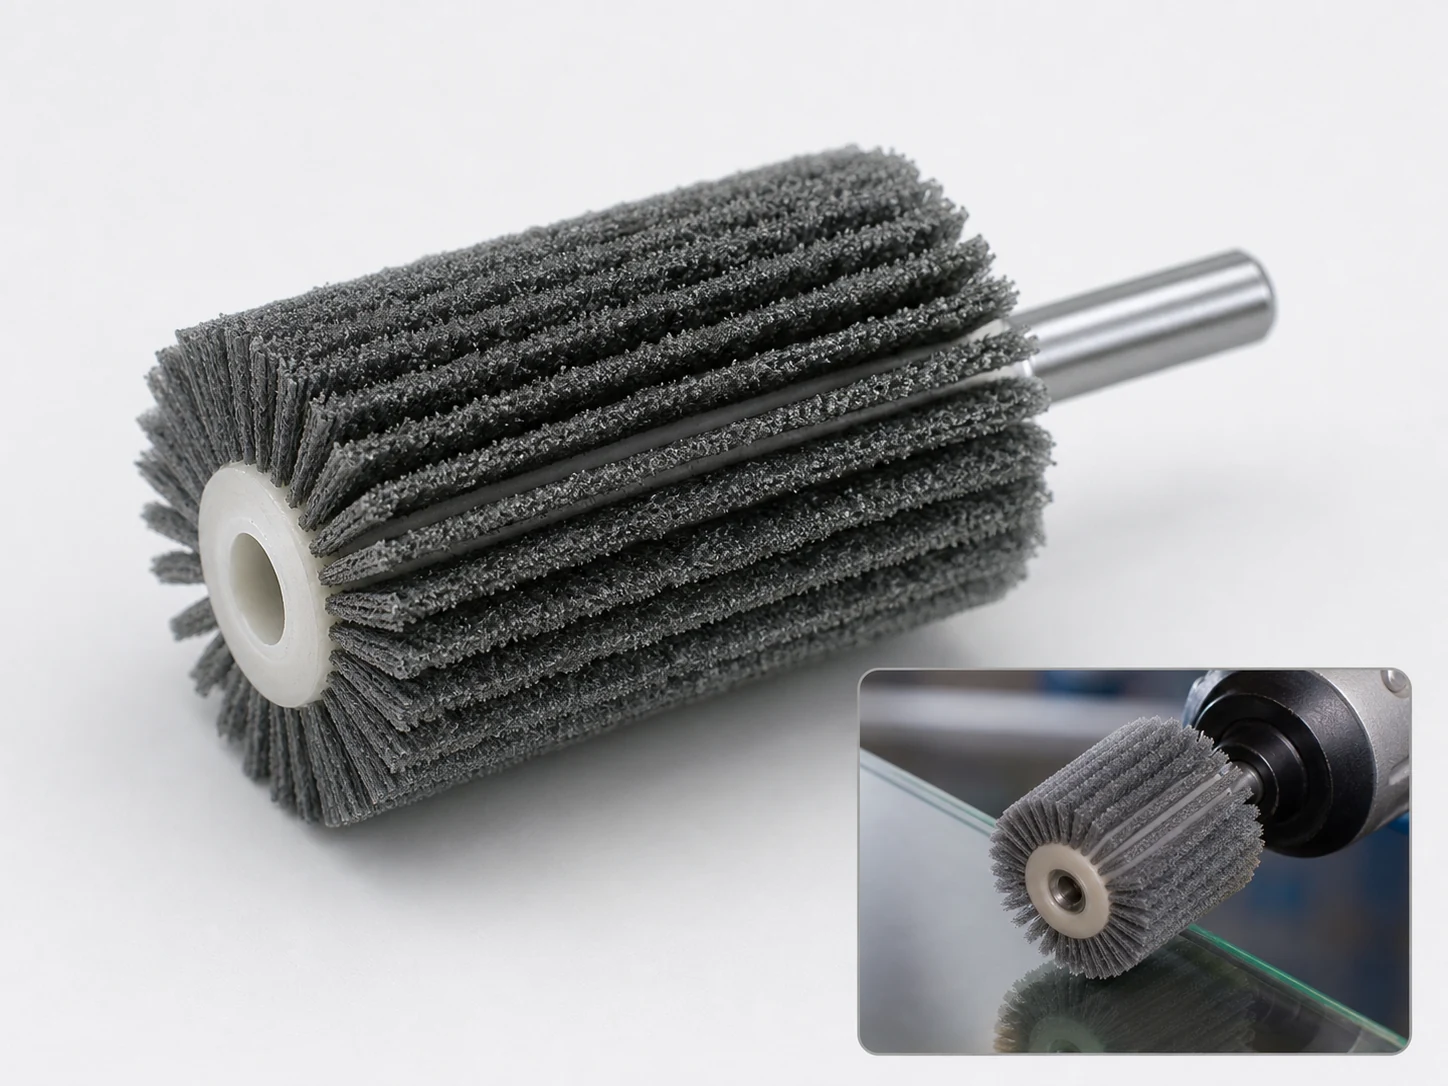
Abrasive Brush Glass
Machine-mounted abrasive nylon brush for glass frosting, edge deburring and residue removal. Silicon carbide…
See the specification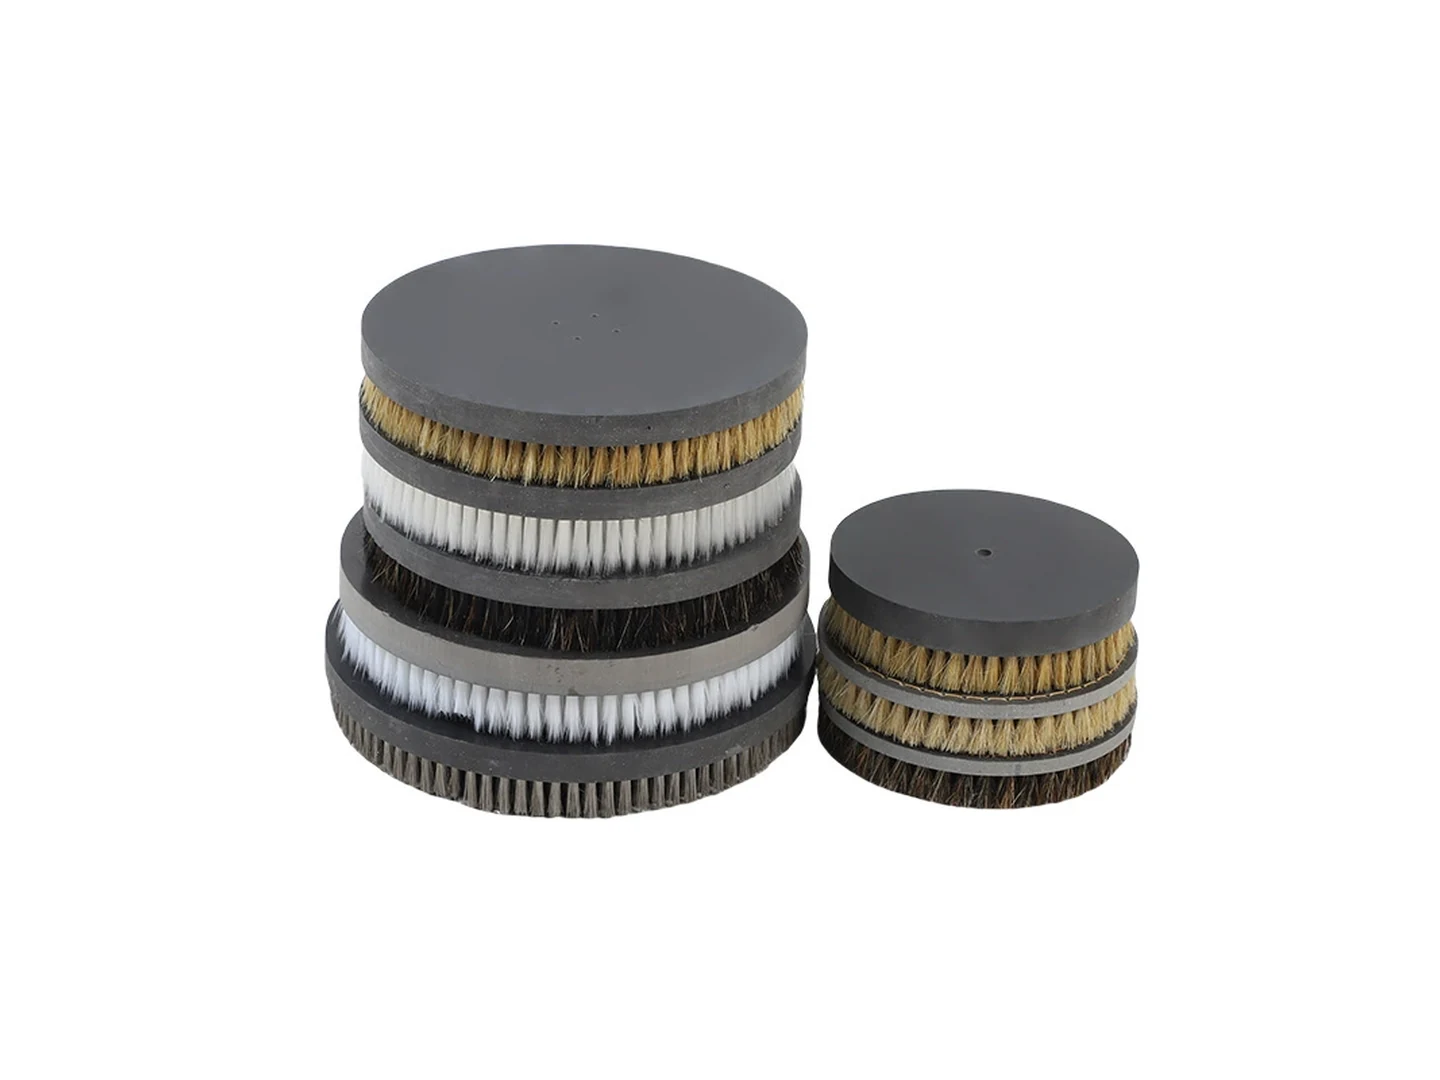
Ceramic Glaze Line Disc Brush
Custom ceramic glaze line disc brushes remove glaze residue, edge burrs, and ceramic fines…
See the specification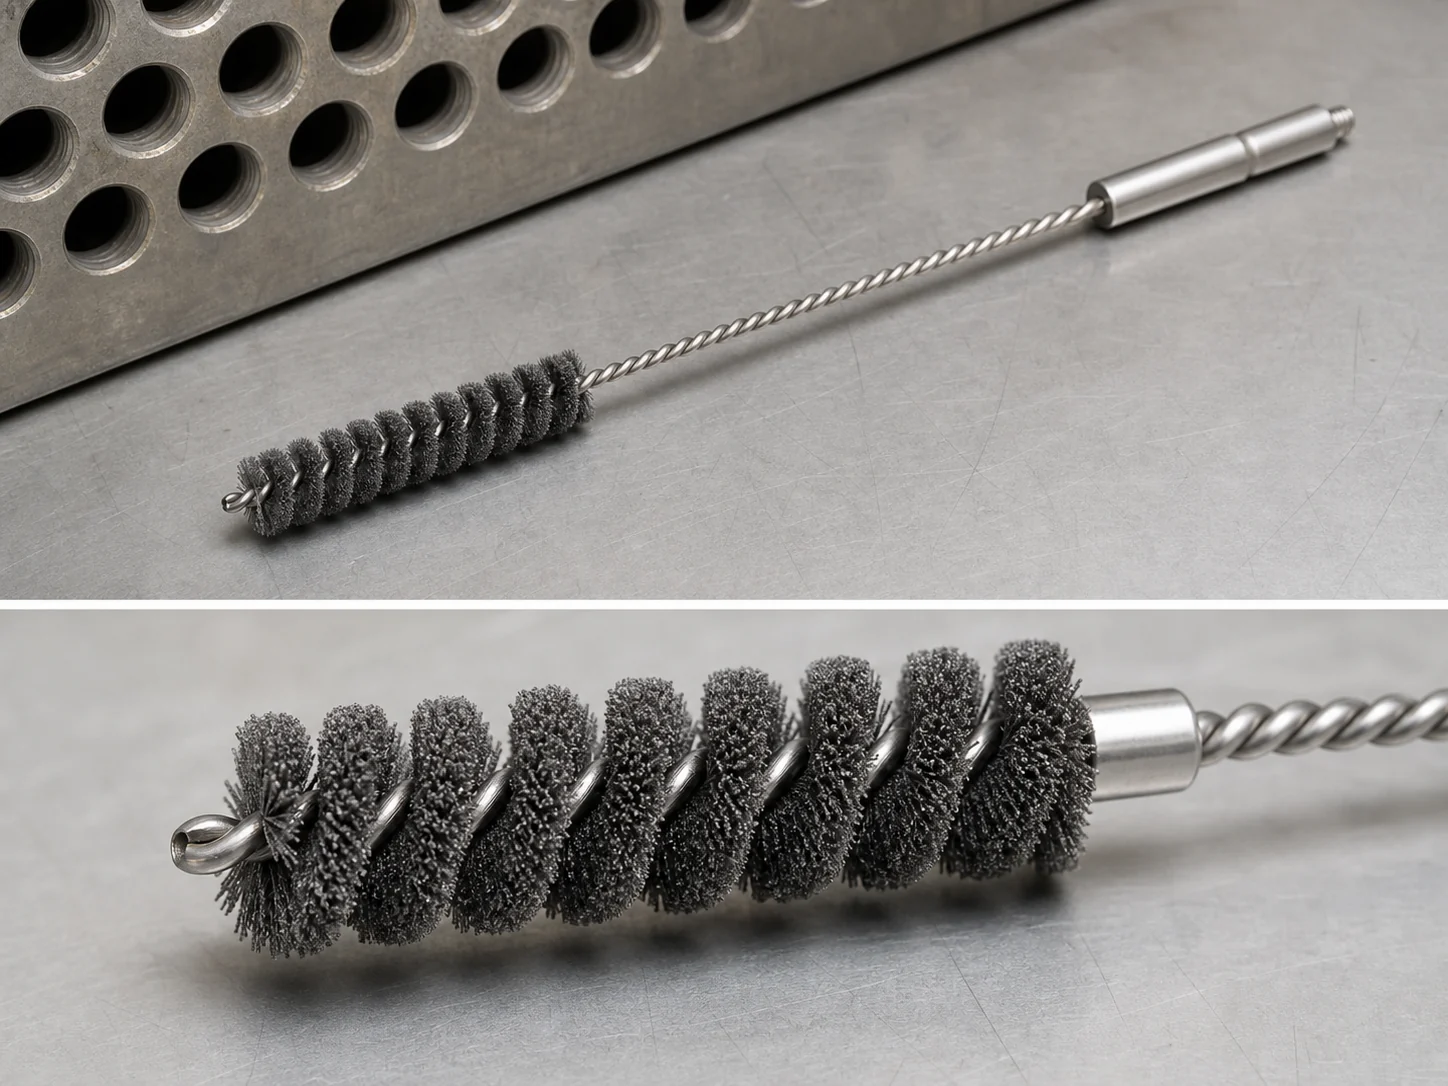
20mm P320 AO Tube Brush
20mm P320 AO tube brush with aluminum oxide abrasive nylon for cleaning heat exchanger…
See the specification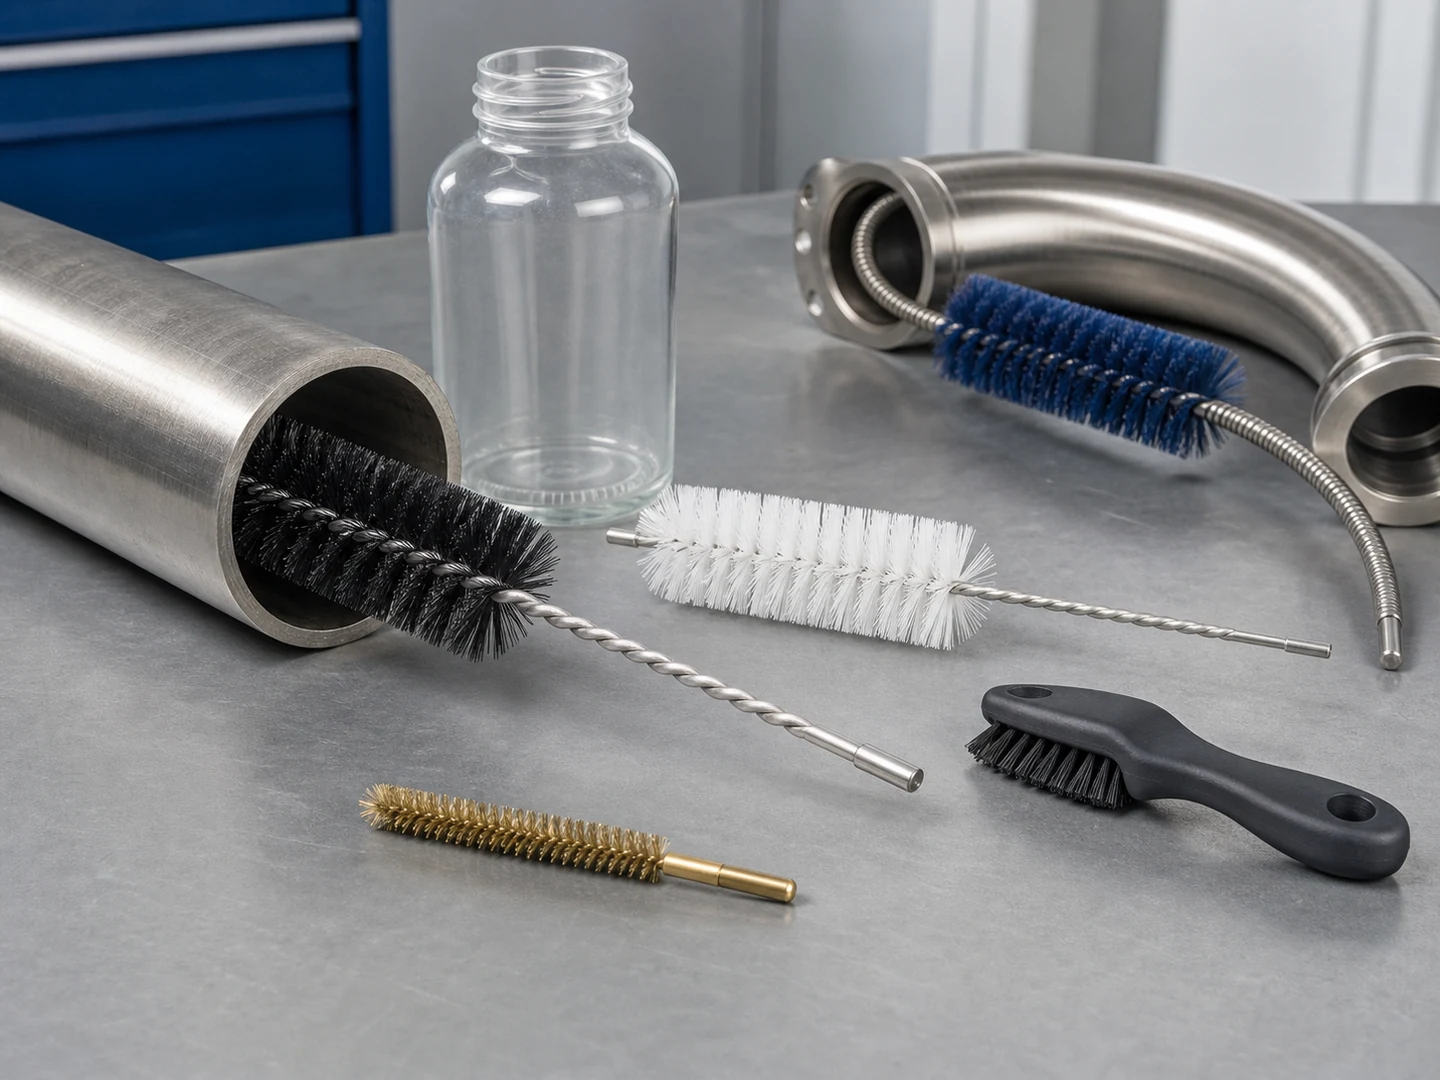
Custom Tube & Pipe Bore Brushes
Choose a tube, pipe, or bore brush when the working surface is inside a…
See how this type is built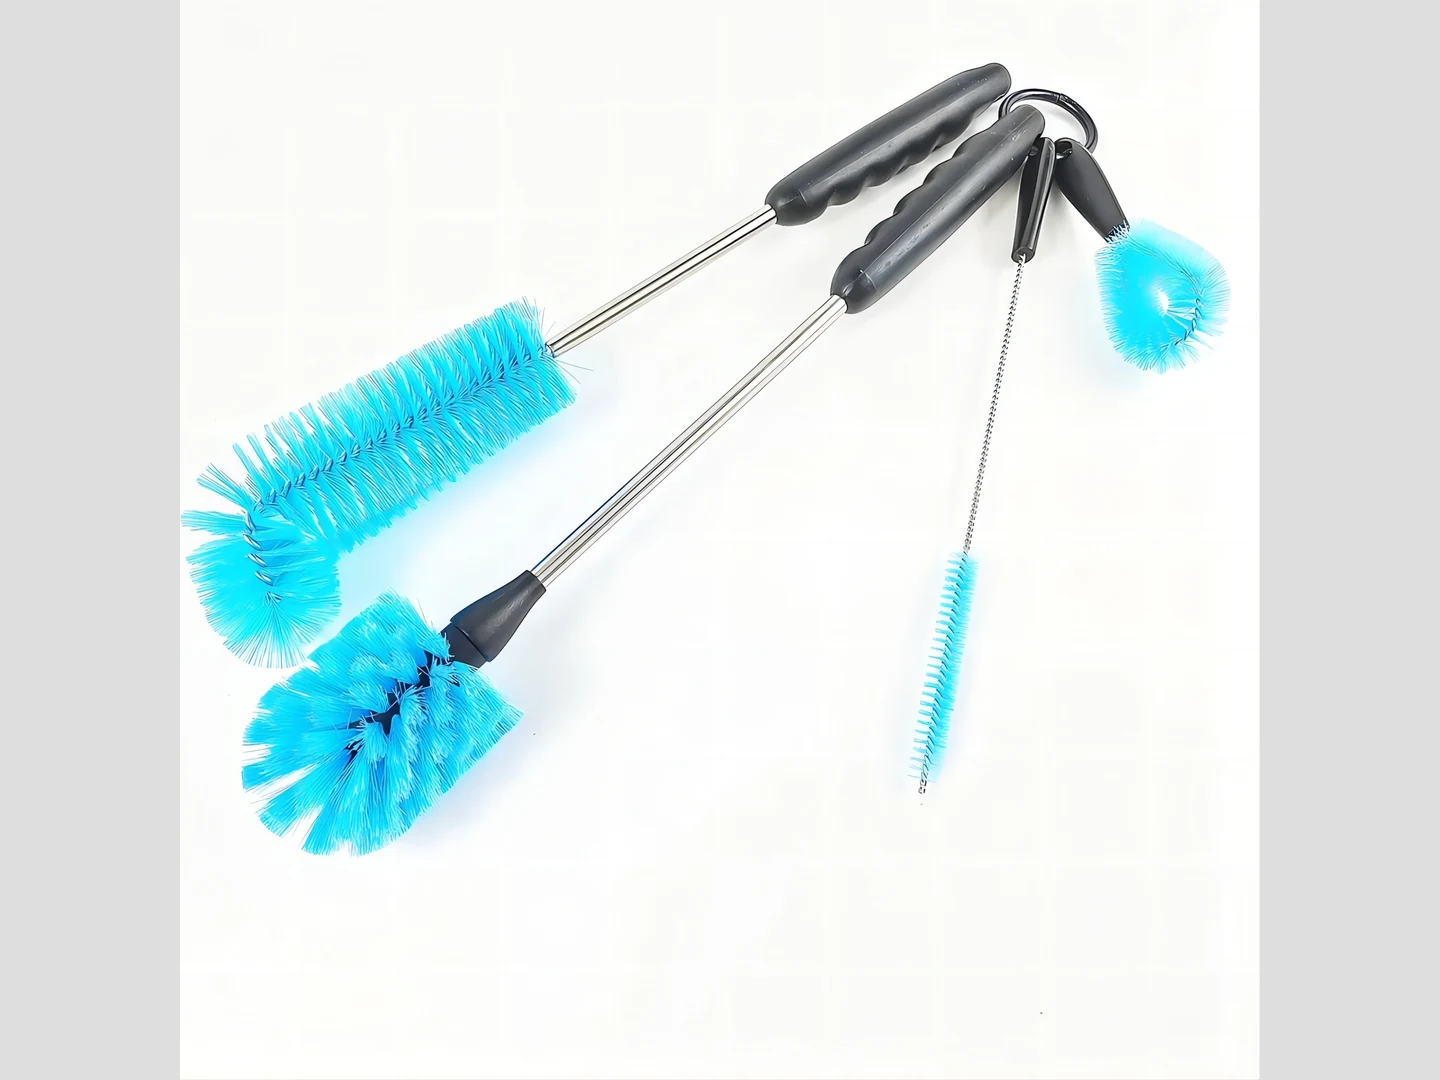
Custom Cup Brushes
Choose a cup brush when a rotating brush face must cover a broader flat…
See how this type is built
Heat Exchanger Tube Cleaning
For Heat Exchanger Tube Cleaning, the brush must reach the working area, disturb or…
See the cleaning job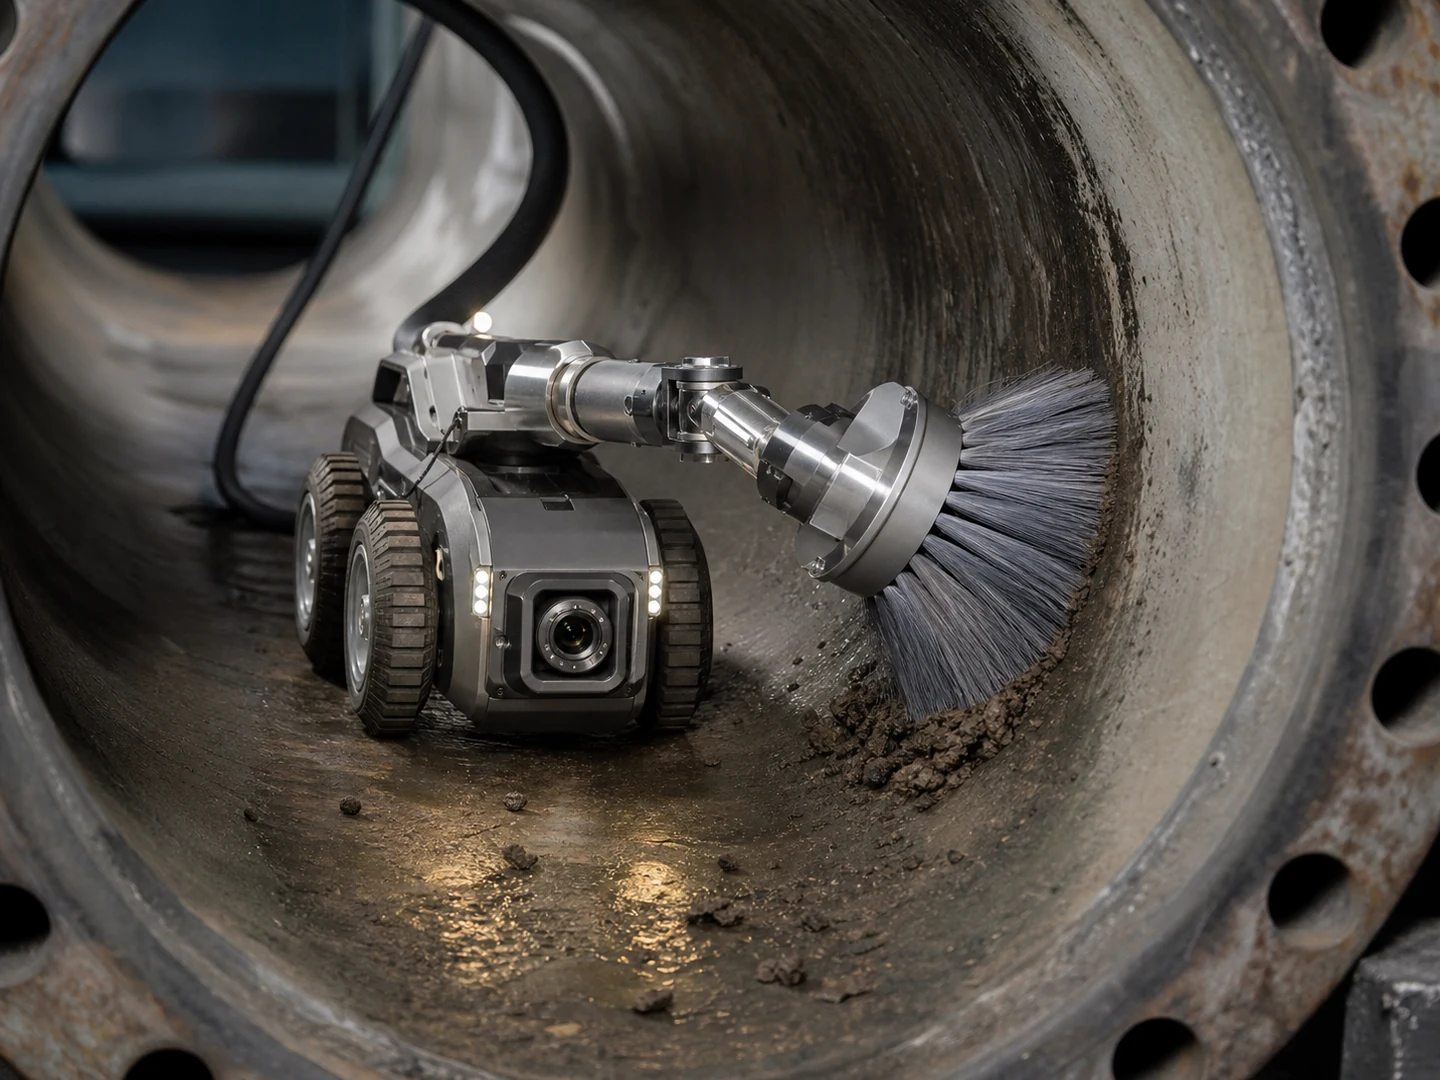
Pipe Robot Brush Attachment Use
For Pipe Robot Brush Attachment Use, the brush must reach the working area, disturb…
See the cleaning job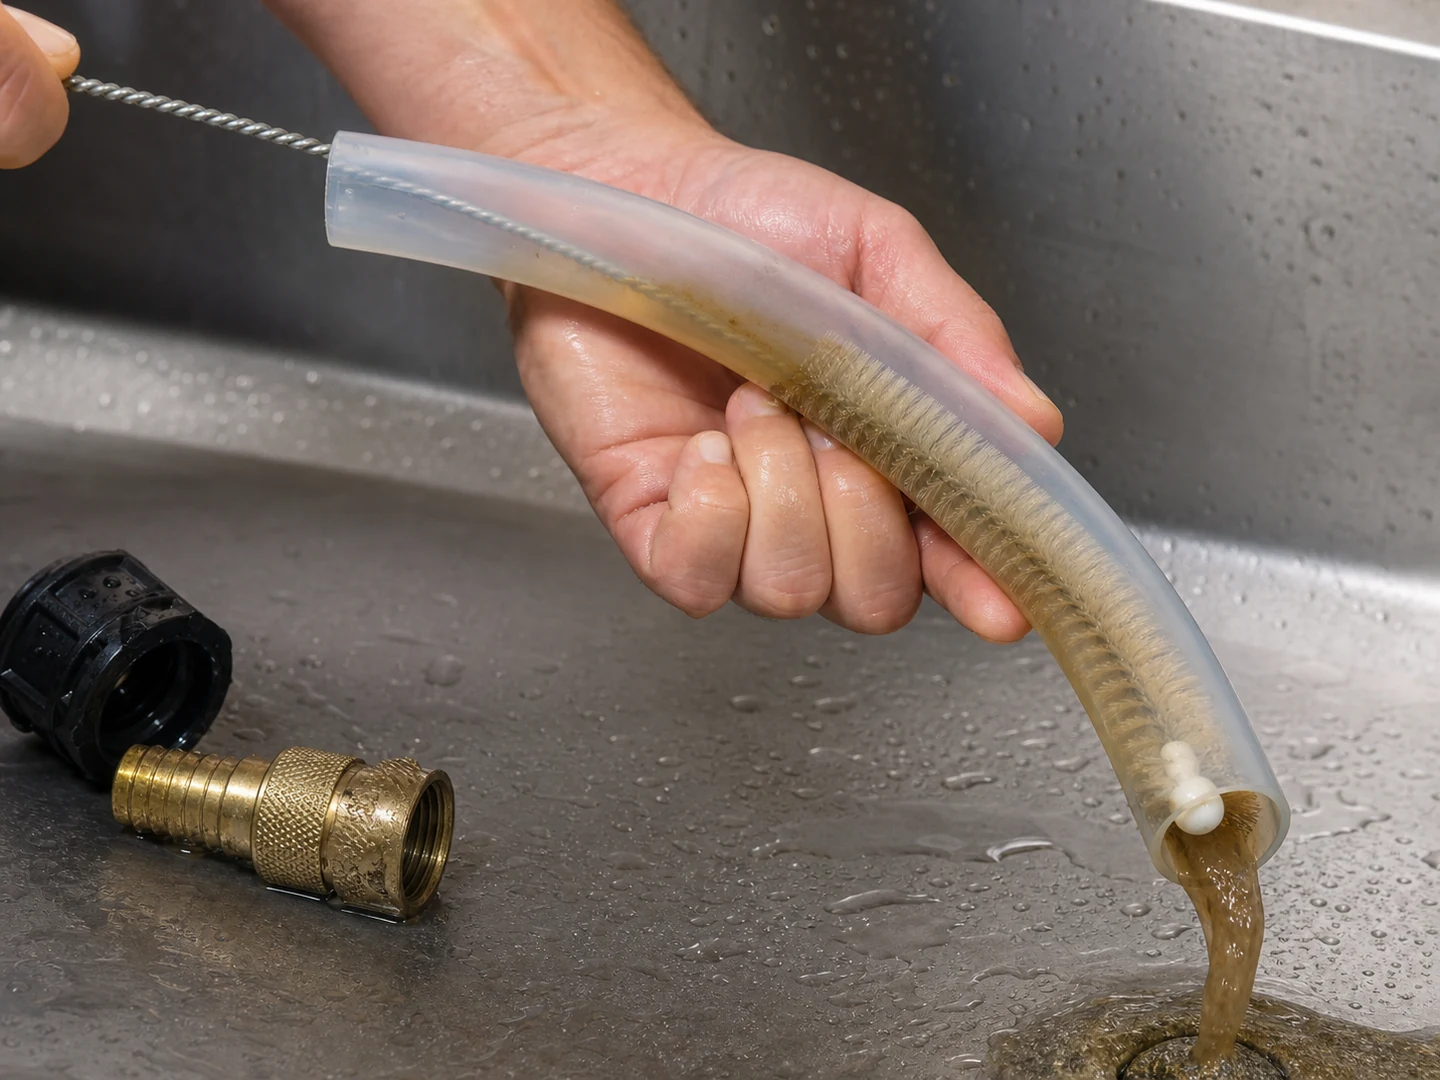
Hose Cleaning
For Hose Cleaning, the brush must reach the working area, disturb or collect oil…
See the cleaning jobCustom Manufacturing RFQ
Discuss This Material
Share the working surface, residue, dimensions, material direction, interface, quantity and drawing or sample photo.
Custom Brush RFQ
Request a Custom Cleaning Brush Quote
Upload a drawing, product photo, or sample photo and provide the core dimensions and cleaning conditions.
“We need a brush to remove wet residue from a stainless steel conveyor, about 800mm wide. The current brush wears quickly. We can send photos.”
“We sell drinkware and need a cleaning brush to include with the product. Quantity around 5,000 pieces.”