
ApplicationIndustrial & Manufacturing
Mold Cavity Cleaning
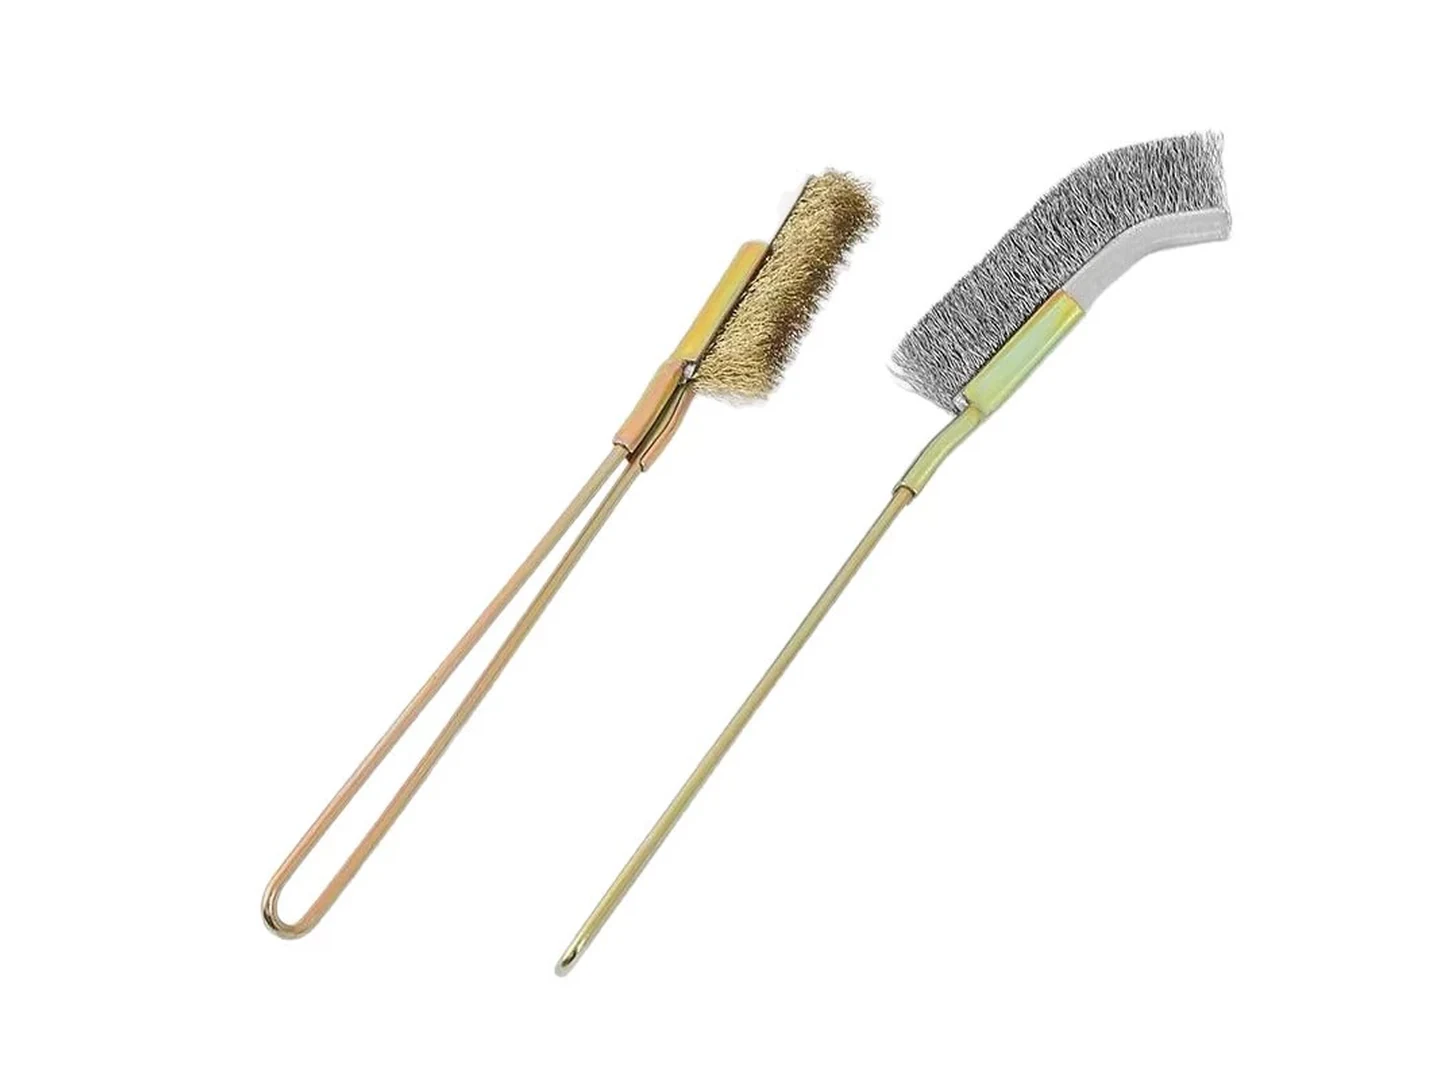
Molds are brushed to take off release agent, carbonized residue and flash without changing the surface that shapes the part. Use brass wire for hardened die-casting and injection molds, nylon or PBT for polished cavities and food molds, and fine pencil-point heads for vents and ejector pins. Long handles reach the cavity while the mold stays in the press.
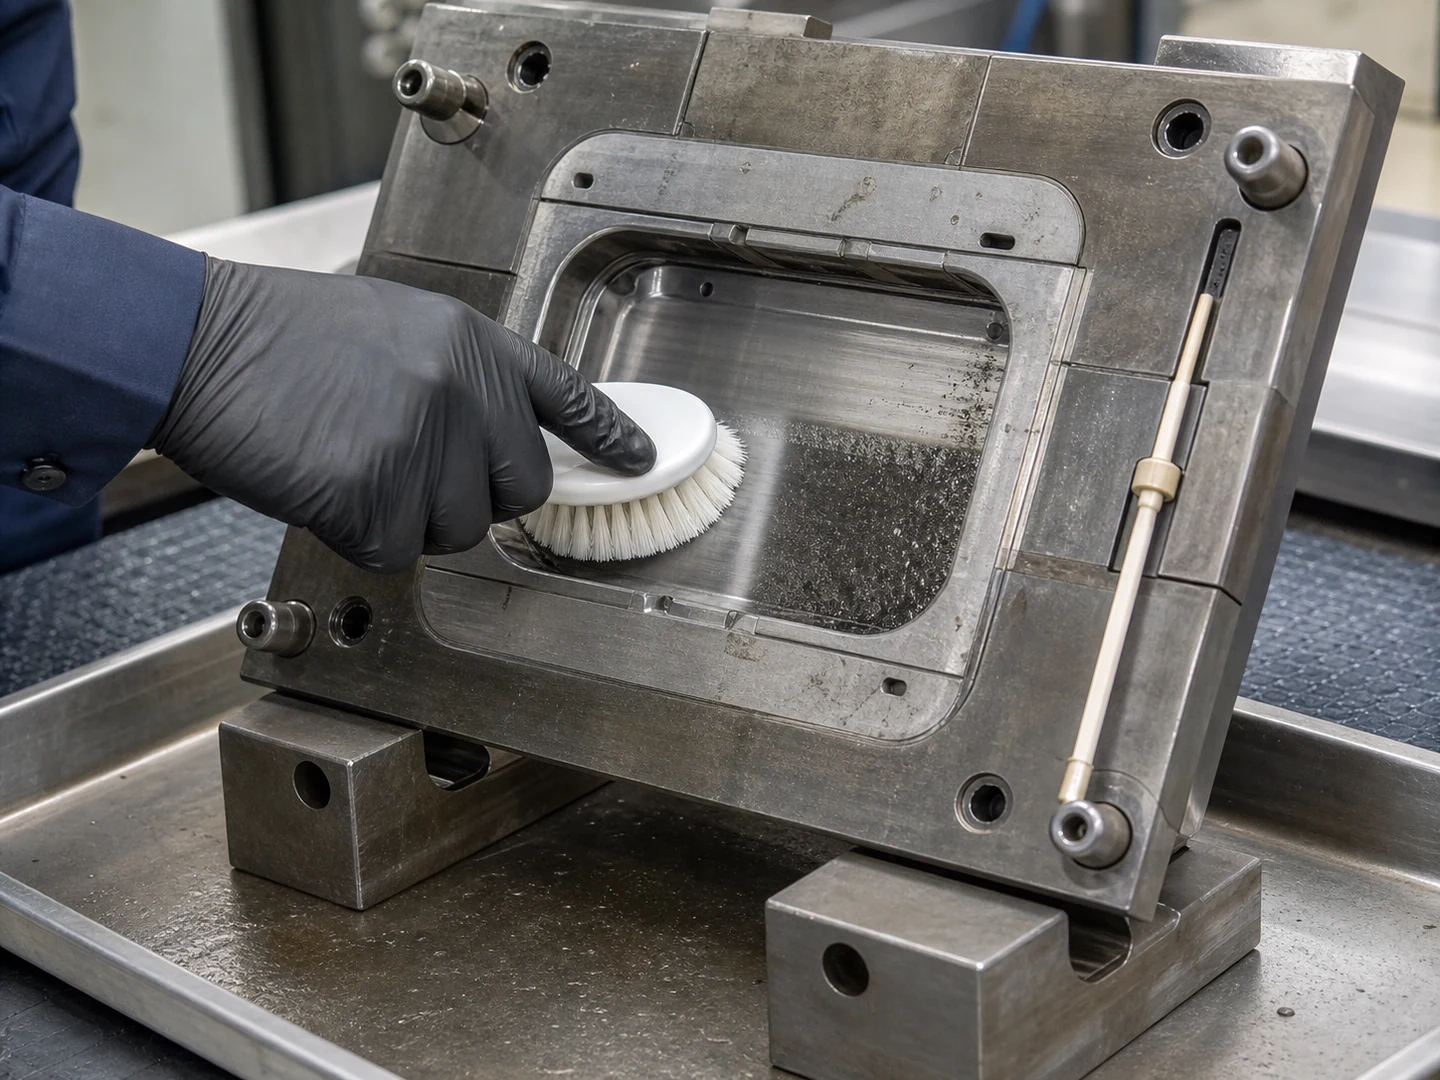
- Cleaning target
- Mold Release Agent/Carbonized Residue/Rubber Residue
- Working environment
- Dry Indoor Area
- Cleaning method
- Dry Brushing / Wet Brushing
- Requirements to check
- Protection of Mold Surface Finish; Solvent-Safety SOP
Catalog brushes made for this job
13 brushes in the catalog
Why is mold cleaning so delicate?
Every shot leaves a little behind. Release agent builds up, outgassing from plastics and rubber deposits in vents and corners, die-casting dies collect baked release and soot, and rubber molds collect cured flash in the parting line. The deposit blocks vents, marks parts and changes dimensions.
But the mold surface is the product. A cavity polished to a mirror gives a gloss part; a textured cavity gives the grain; a vent ground to a few hundredths of a millimeter lets gas out without flashing. Scratch the polish, round an edge or open out a vent, and every part after that is wrong.
So mold brushes are softer than the steel they clean, sized to each feature, and used on molds that are cool enough to handle, in or out of the press.
Which molds and mold features need a brush?
| Part or area | Residue type | Cleaning requirement |
|---|---|---|
| Injection Mold Cavity | Mold-release agent, carbonized residue, outgassing deposit | Reach the cavity walls on an extended handle without marking the polish. |
| Die-Casting Mold | Mold-release agent, soot, oxidized metal film | Fill that tolerates the die temperature and clears release agent and soot. |
| Rubber Mold | Mold-release agent, cured rubber residue, sulfur bloom | Pick cured flash out of the parting line and detail without rounding edges. |
| Composite Mold | Mold-release agent, cured resin, fiber debris | Lift cured resin and fiber debris without scratching the gelcoat or tool face. |
| Vent and Ejector Pin Detail | Mold Release Agent, Carbonized Residue, Rubber Residue | A fine brush that clears the vent depth and the pin clearance. |
Sizes from the mold cleaning brushes we make:
| Parameter | Typical range |
|---|---|
| Head width | 5–50 mm, to the vent, cavity mouth or feature |
| Overall length | 150–400 mm, long-reach handles available |
| Brass wire | 0.10–0.30 mm, 65/35 or 70/30 brass |
| Nylon filament | 0.10–0.60 mm |
| Trim length | 10–30 mm |
| Handle angle | Straight, 45° or 90° |
Which brush suits each mold?
| Cleaning target | Recommended brush type | Why it fits |
|---|---|---|
| Injection Mold Cavity | Handheld Detail Brushes | A cavity is a deep closed form, so a head on an extended handle is what gets down its walls while the mold stays in the press. |
| Die-Casting Mold | A die face holds baked release and soot on a hardened surface, so a hand-guided head lets the operator press where it is needed and stay off the vent lands. | |
| Rubber Mold | Cured rubber flash sits in the parting line and the detail, so a hand-guided head picks it out feature by feature without rounding the mold edges. | |
| Composite Mold | A composite tool is a polished surface that decides the part finish, so contact is placed by hand and kept light enough not to change the gloss. | |
| Vent and Ejector Pin Detail | Vents and pin clearances are the smallest features and the first to block, so a fine head clears them without opening the vent depth out. |
For cavities, an angled or 90° handle reaches the walls with the mold open in the press. For vents and parting lines, a narrow strip or pencil-point head follows the feature. Toothbrush-pattern brass brushes are a common die-casting tool for the die face.
Food and cosmetics molds, such as chocolate and lipstick molds, take round and tapered nylon or PBT heads of 6–15 mm with end-rounded tips for gloss-sensitive polycarbonate.
Which fill is safe on mold steel?
| If the condition is… | Filament to start with | Why |
|---|---|---|
| Hardened die-casting and injection molds | Brass Wire | Cuts release and carbon and is softer than tool steel, up to about 250°C intermittent |
| Polished cavities and textured surfaces | Nylon PA | Cleans without marking polish or grain, up to about 120°C |
| Warm molds, food and cosmetics molds | PBT | Holds up to about 150°C and to cleaning solvents |
| Molds cleaned near static-sensitive parts | Anti-static Filament | Stops dust being drawn back onto the cleaned cavity |
| Grounded cleaning of molds for electronics parts | Conductive Nylon | Takes charge away through a grounded handle |
| Light cleaning and economy brushes | Polypropylene PP | Soft and economical for mold housings and frames |
Keep steel wire off mold surfaces. Brass is softer than tool steel, but it still marks soft alloys and high polish, so use nylon there.
How should a mold be brushed?
- Let the mold cool to a safe handling temperature, or follow the press’s safe-access procedure.
- Apply mold cleaner to soften release agent and residue.
- Brush in the direction of the polish or grain, with light strokes.
- Clear vents and ejector-pin clearances with the fine brush.
- Wipe clean and apply mold protection before storage.
What do we need to quote mold brushes?
- Mold type and surface: polished, textured, hardened die, rubber or composite.
- Feature sizes: vents, cavity mouths, pin clearances.
- Mold temperature and the cleaners you use.
- Handle length and angle.
- Quantity per design. Small brushes start at 500 pieces.
When is a brush not enough for a mold?
Heavy carbonized deposits and blocked vents in production molds are often cleaned off-press by dry-ice blasting, ultrasonic or laser cleaning. Damage to the polish needs re-polishing by a toolmaker. A vent that keeps blocking may need re-cutting or a change of process.
What mistakes damage molds during cleaning?
- Steel wire on polished or textured cavities.
- Scraping vents with metal tools, which opens them out and causes flash.
- Brushing across the polish direction.
- Leaving cleaner on the steel, which can stain or corrode it.
Questions buyers ask about Mold Cavity Cleaning
Why use brass brushes on molds?
Brass cuts release agent and carbon and is softer than tool steel, so it cleans hardened molds without scratching them. Use nylon on high polish and soft alloys, and never steel wire.
How should mold vents be cleaned?
With a fine, narrow brush that follows the vent, after a mold cleaner has softened the deposit. Metal scrapers open the vent out and cause flash.
Continue Exploring
Recommended Reading & Related Brush Resources
Nylon Tire Mold Cleaning Brush
Custom tire mold cleaning brush with PA66/PA6 nylon filament shaped to follow tread grooves, sipes, lettering, and vents.
See the specification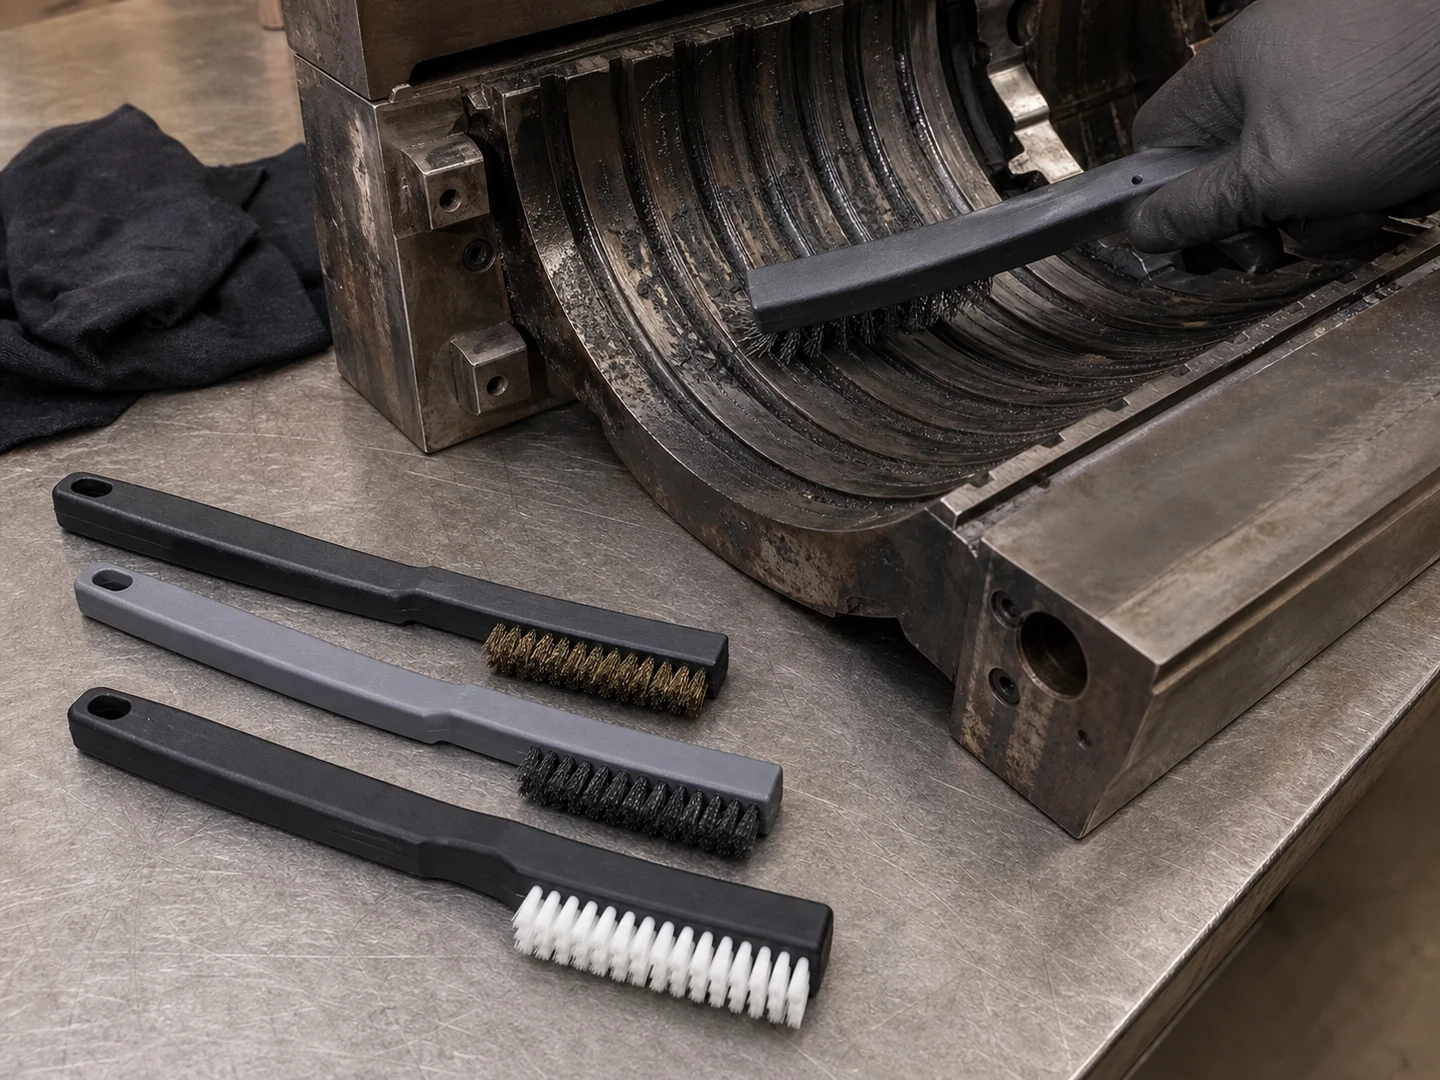
Rubber Mold Cleaning Brush
Rubber Mold Cleaning Brush for mold maintenance: clean release agent, vulcanized flash, carbon, and oils from cavities, vent grooves, and parting lines.
See the specification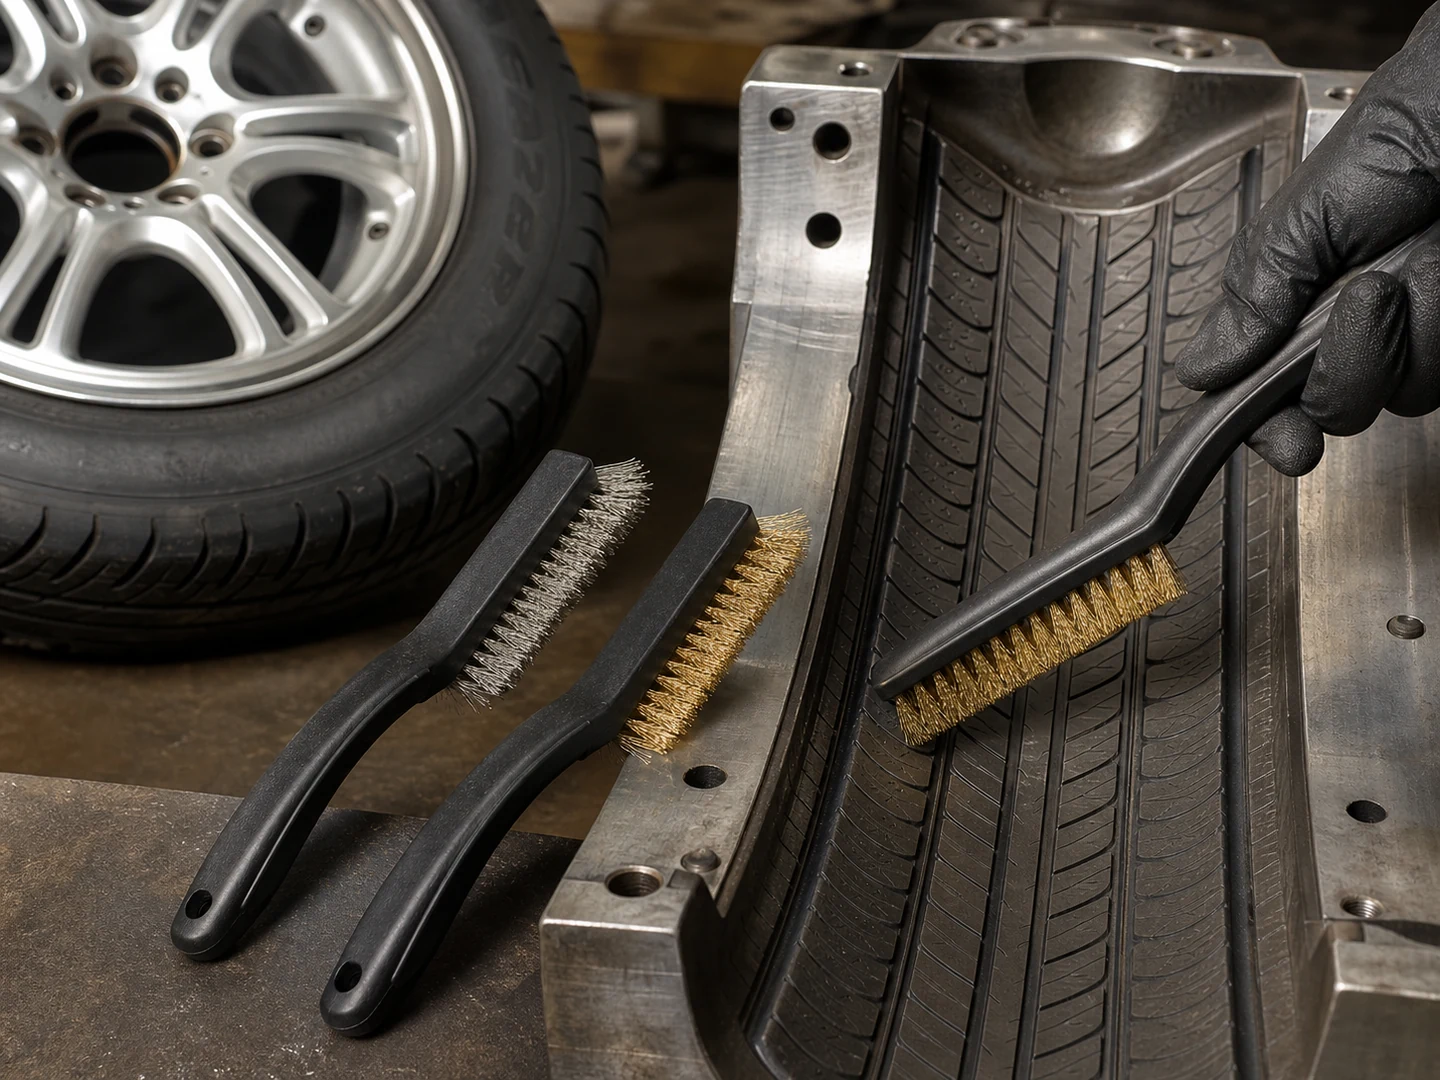
Stainless Steel Brass Mold Tire Brush
316 stainless steel and brass wire mold tire brush in cup, wheel, or end form for tire mold cleaning. Removes cured rubber and release agents.
See the specification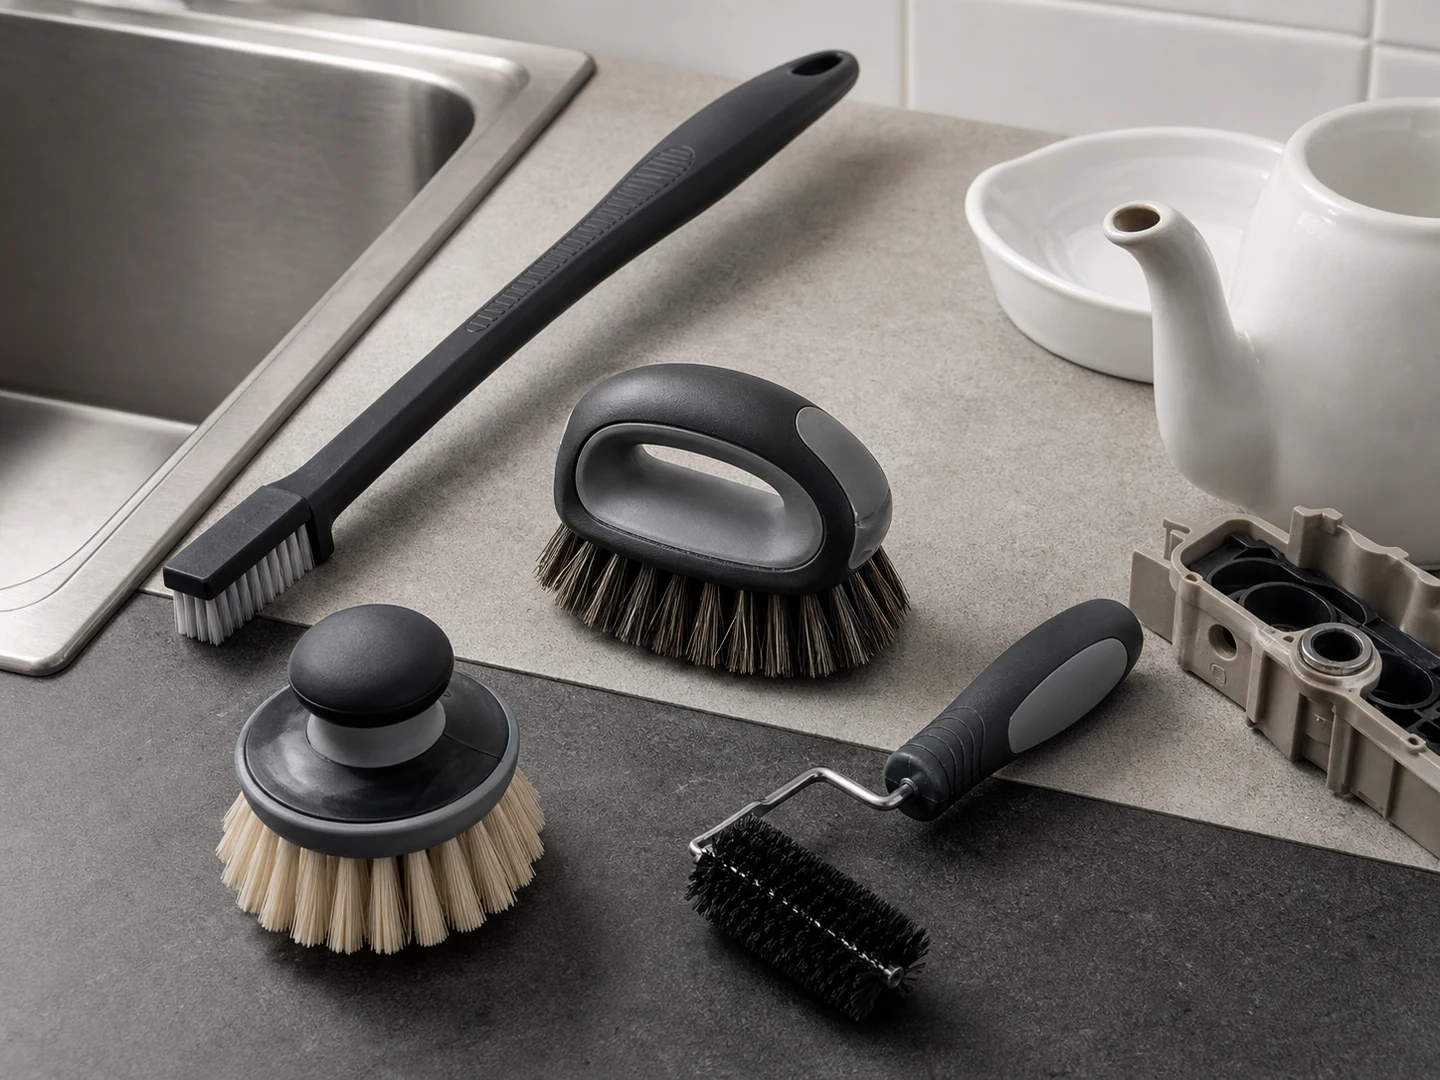
Custom Handheld Detail Brushes
A handheld detail brush puts the operator's hand pressure into a small place: a seam, a grout line, a vent, a connector, a mold vent or a grinder chute.
See how this type is built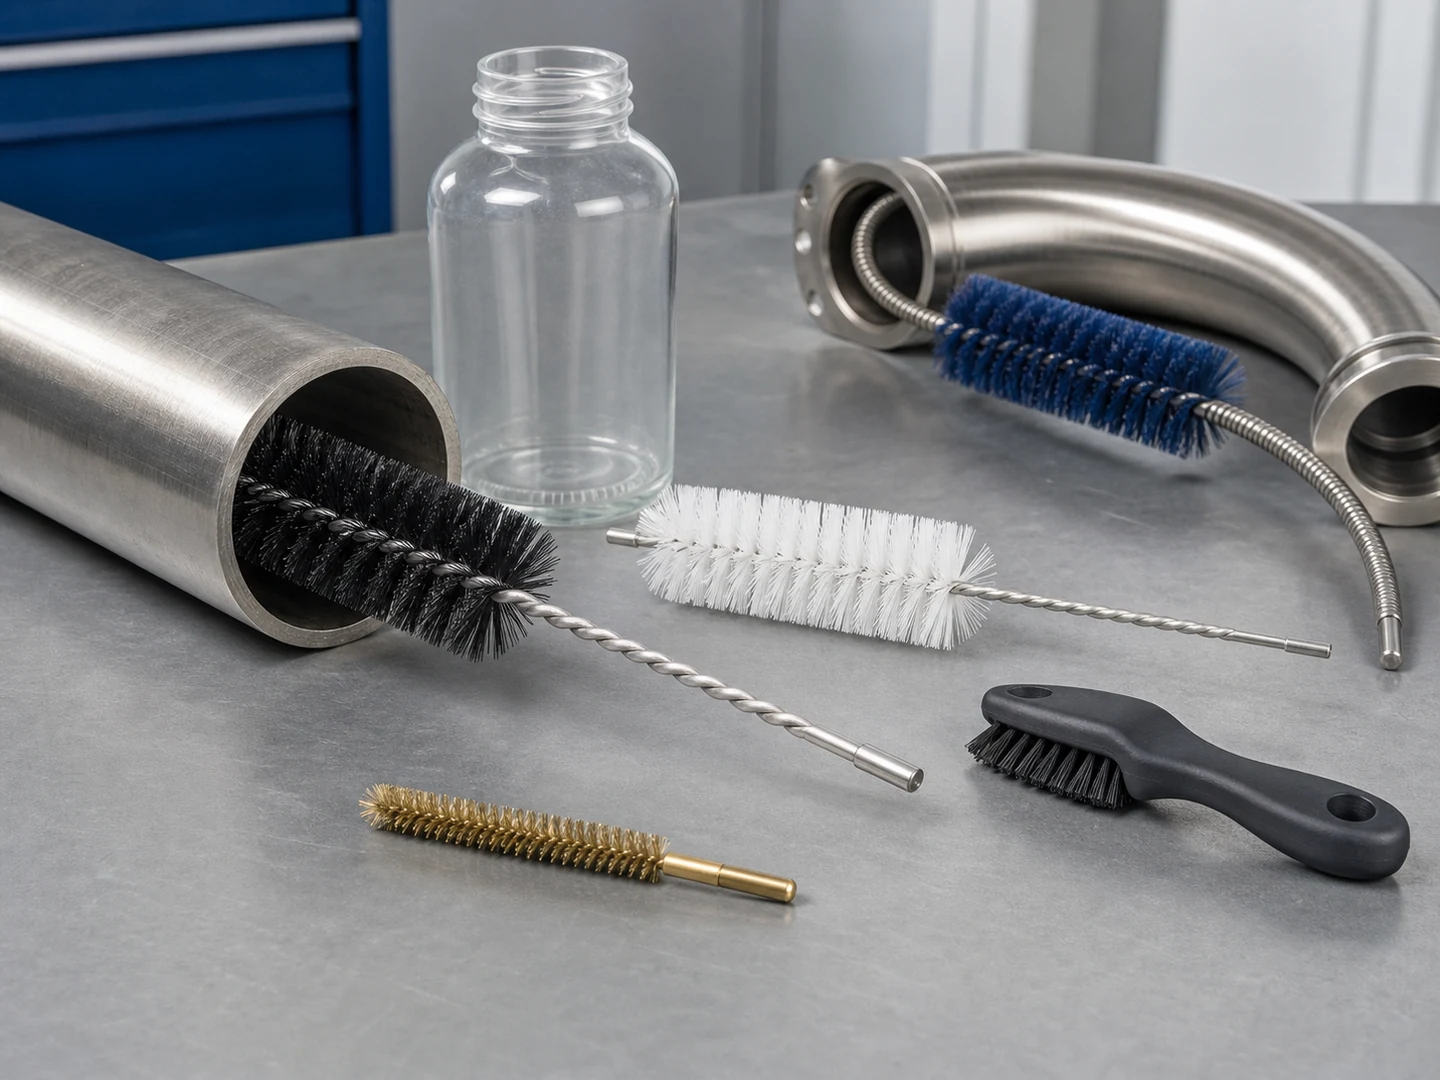
Custom Tube & Pipe Bore Brushes
A tube or bore brush cleans the whole inside circumference of one passage as it is pushed, pulled or turned along it.
See how this type is built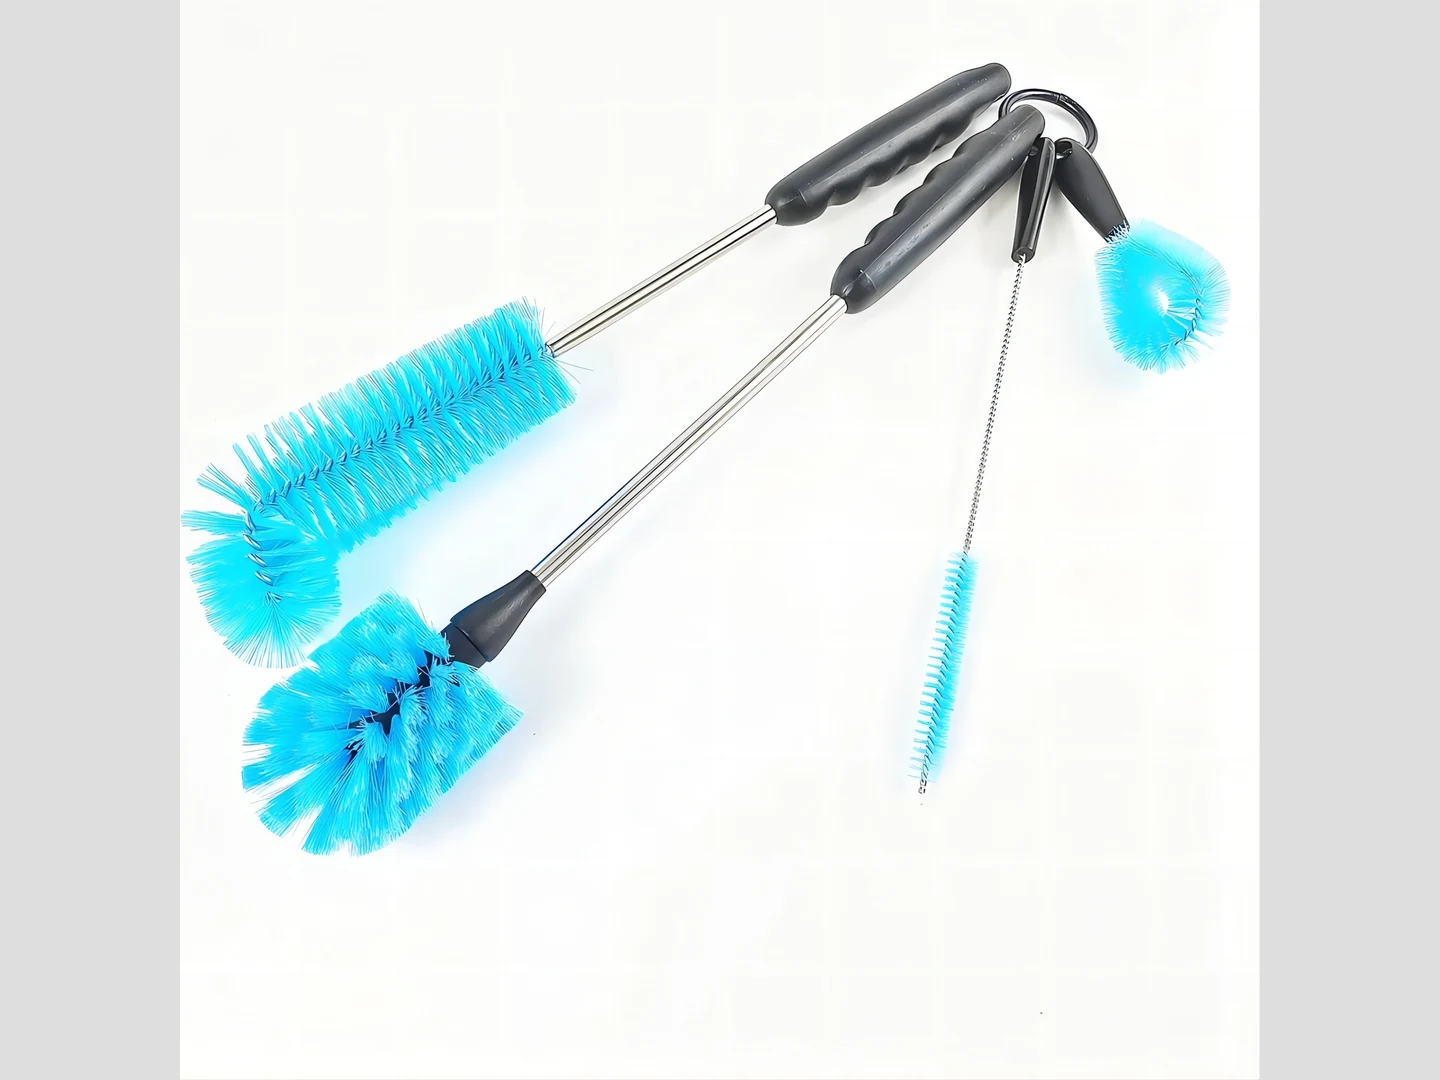
Custom Cup Brushes
A cup brush has its fill set around the rim of a cup-shaped body, so the filament ends form a broad, flat, rotating face.
See how this type is built
Nylon PA
Nylon is the default brush filament: tough, springy and long-wearing, in a stiffness range from soft detail fill to coarse scrubbing fill.
Compare this material
Conductive Nylon
Conductive nylon is nylon filament made conductive with carbon or another additive, so the brush can carry static charge away instead of building it.
Compare this materialCustom Manufacturing RFQ
Discuss This Application
Share the working surface, residue, dimensions, material direction, interface, quantity and drawing or sample photo.
We reply to every request within 24 hours, with a quotation or with the questions we need answered first. If the brush can be made on our existing tooling, we make the sample directly. If it needs new tooling, we quote a sample fee and a tooling fee, and the sample fee is credited against the bulk order. Need an NDA first? We sign yours before you send drawings, and the files you send are never shown to other customers.
- MOQ500 pcs for small hand-held brushes, 100 pcs for medium and large ones
- SampleTypically 3–7 days
- ProductionFrom 7 days after sample approval, by size and quantity
- Payment30% deposit and 70% before shipment above US$10,000; smaller orders on agreed terms
“We need a brush to remove wet residue from a stainless steel conveyor, about 800mm wide. The current brush wears quickly. We can send photos.”
“We sell drinkware and need a cleaning brush to include with the product. Quantity around 5,000 pieces.”