
Nylon Tire Mold Cleaning Brush
OEM / ODM custom manufacturing · made to order
Custom tire mold cleaning brush with PA66/PA6 nylon filament shaped to follow tread grooves, sipes, lettering, and vents.
- Brush type
- Custom Handheld Detail Brushes
- Material
- PA66 NylonPA6 NylonRubber
- Overall length
- 200–500 mm typical for hand use; configurable to mold depth and operator reach
- Temperature
- Up to 120°C for PA66; PA6 generally lower. Short-term contact with warm molds is acceptable; hot-mold cleaning above this range requires a heat-resistant alternative
- Application
- Mold Cavity Cleaning
- MOQ
- 100 pcs
- Lead time
- Within 7 days (up to 100 pcs)
- Sample
- Typically 3–7 days
What can this brush do for you?
Trim follows the cavity, not the other way around
Generic brushes sweep across the high points of a tread pattern and leave residue packed at the base of grooves, sipes, and lettering. The head profile and filament trim on this brush are shaped to match the actual tire-mold geometry, so the filament tips reach into the recessed areas where cured rubber and release agent collect.
Removes deposits that shorten mold life and affect tire quality
PA66 and PA6 nylon filaments cut through release-agent films, rubber crumbs, and carbonized deposits that accumulate between curing cycles. Clearing this contamination restores crisp tread definition, sidewall lettering, and vent function before it creates surface defects or pressure-related scrap.
Cleans without scoring steel or aluminum mold surfaces
Nylon filament is softer than mold steel, plated surfaces, and aluminum body sections. It applies enough mechanical action to remove residue while protecting the exact surface finish that tire appearance depends on. This matters most on polished sidewall plates and fine lettering where wire brushes would leave visible marks.
Opens blocked vents and prevents air-trap defects
Vent holes and spring vents clog quickly with rubber and mold release residue. When air cannot evacuate, the result is trapped-air blemishes, thin lettering fill, and short molded details. A matched vent-cleaning portion of the brush pushes contamination out of these small openings and restores normal venting between production runs.
Works with common mold cleaners and release agents
Both PA66 and PA6 tolerate the mold cleaners, mild alkaline solutions, and hydrocarbon-based release agents typically used in tire mold maintenance. The same brush can be used dry for light deposits or with a cleaning agent for heavier buildup without rapid filament degradation.
Technical Specifications
The following parameters are typical project starting points and can be adjusted to the specific tire mold pattern, groove widths, and cleaning process.
| Parameter | Value / Options |
|---|---|
| Filament material | PA66 nylon or PA6 nylon, selected for stiffness, wear, and chemical resistance |
| Filament diameter | 0.15–0.50 mm for fine lettering, sipes, and vents; 0.50–0.80 mm for open tread grooves and wider cavities |
| Head profile | Custom shaped or trimmed to tread groove, sipe, lettering, bead, and vent geometry |
| Overall length | 200–500 mm typical for hand use; configurable to mold depth and operator reach |
| Handle / mount | Ergonomic PP or TPE handle, aluminum or stainless ferrule, or round/hex shank for power-tool use |
| Maximum continuous temperature | Up to 120°C for PA66; PA6 generally lower. Short-term contact with warm molds is acceptable; hot-mold cleaning above this range requires a heat-resistant alternative |
| Chemical exposure | Compatible with common mold cleaners, mild alkaline solutions, and hydrocarbon-based release agents; project-specific chemical review recommended |
| Color / identification | Custom filament color, ferrule marking, molded handle ID, or project-specific coding |
| Brush type | Custom Handheld Detail Brushes |
| How it is driven | Hand-guided |
| Cleaning target | Tire molds, during mold maintenance |
| Surface or part | Tread segments, sipes, lettering, sidewall plates, bead rings and vents |
| Residue or debris | Cured rubber residue, release-agent build-up and carbonized deposits |
| Mounting / connection | Ergonomic PP or TPE handle, aluminum or stainless ferrule, or round/hex shank for power-tool use |
Medium brush
100 pcs
Minimum order
Worked with two hands or on a pole: chimney, gutter and pond-filter brushes, discs, cups and tank brushes.
Production lead time, once the specification is confirmed
- Up to 100 pcsWithin 7 days
- 101–5,000 pcsWithin 14 days
- 5,001–50,000 pcsWithin 21 days
- Over 50,000 pcsConfirmed with your quotation
Peak season can extend these times; the shipping date is confirmed in writing with your quotation. Sampling and shipping are quoted separately.
This mold maintenance brush uses shaped nylon (PA66/PA6) filament to follow the tread grooves, sipes, lettering, and vent geometry of tire molds while removing cured rubber residue, release-agent buildup, and carbonized deposits without scoring the mold surface.
What is a Nylon Tire Mold Cleaning Brush?
A Nylon Tire Mold Cleaning Brush is a mold-maintenance brush configured specifically for tire mold cavities rather than general workshop use. It contacts the machined surfaces of tread segments, sidewall plates, bead rings, and vent passages, where rubber residue, release agent, and carbonized contamination accumulate during curing.
The working head is shaped so that filament length, density, and angle follow the deeper features of the mold. During use, the operator guides the brush through the same grooves, sipes, and lettering that form the tire surface. Filament tips flex into recesses, wipe away the residue film, and drag loosened particles out of tight corners and vents.
This brush can be supplied as a hand tool with an ergonomic handle or as a shank-mounted configuration for rotary or reciprocating use. It is not a substitute for heavy mechanical cleaning, shot blasting, or chemical stripping. Its role is controlled residue removal that preserves mold detail and venting performance between deeper maintenance cycles.
How do I choose the right one?
Measure the smallest feature you need to clean. The narrowest sipe, lettering stroke, or vent opening sets the filament diameter and grouping. A brush that cannot enter the smallest recess will only clean the high surfaces. Identify the minimum groove width, sipe width, lettering depth, and vent diameter before selecting filament size.
Match filament material to the residue and mold surface. PA66 is stiffer, more wear-resistant, and better for cured or carbonized deposits on steel molds. PA6 is more flexible and less aggressive, making it the better choice for polished sidewall plates, soft aluminum molds, or areas where even faint surface marking is unacceptable. The same material behaves differently as filament diameter changes: finer filament reaches deeper into detail, while coarser filament scrubs wider groove floors more effectively.
Use a shaped trim, not a flat brush. Ask whether the brush should be supplied as a flat utility head or with a profile cut to the mold cross-section. A flat brush will skip the recessed areas that matter most. Provide a mold drawing, 3D scan, or sample tread section so the filament ends can be trimmed to follow groove depth, shoulder angles, and lettering contours.
Decide between hand and power configuration. A hand-guided brush gives the operator direct feel and control on detailed lettering or delicate sidewall plates. A shank-mounted brush used on a rotary or reciprocating tool clears larger tread areas faster but requires controlled speed and pressure. For semi-automated or robot-guided cleaning, specify the exact mounting interface and allowable radial dimensions.
Check the cleaning environment. Cleaning agents, wash temperature, and whether the mold is cleaned warm or cooled all affect material choice. If the mold is cleaned while still hot above approximately 120°C, nylon will soften; either allow the mold to cool before brushing or consider a different cleaning approach.
Know when this brush is not the right choice. Heavy mill scale, deep rust, or thick baked-on carbon that requires aggressive mechanical action generally calls for a brass or steel wire brush. Extremely narrow blind passages may need a needle-style probe or specialized micro-brush. If the contamination is mostly loose dust or blast media, an air blow-off or vacuum step may be more efficient than brushing. This nylon mold brush is the right option when surface preservation, detail access, and consistent residue removal are the priorities.
Can I customize this brush?
Every tire mold pattern is different, so this brush is built around the cavity geometry, groove dimensions, and cleaning process. To define a custom configuration, provide the mold drawing or 3D scan, tread groove widths, sipe dimensions, lettering depth, vent locations, access clearances, cleaning chemical, operating temperature, mounting interface, and expected usage frequency.
We can adjust:
- Head profile and trim — matched to groove depth, sipe geometry, lettering, vents, bead area, or sidewall contour
- Filament type — PA66 or PA6, filament diameter, density, length, and stiffness to match residue and surface sensitivity
- Handle — length, grip material, ergonomic shape, hanging feature, or molded identification
- Shank or mounting — round shank, hex drive, quick-change fitting, or custom stem for power-tool or automated use
- Ferrule and stem material — aluminum, steel, or stainless steel as required by the cleaning environment
- Color and marking — filament color, ferrule marking, pad print, or laser marking for area or mold-type identification
- Packaging — bulk, individually bagged, or labeled sets for mold maintenance programs
Where does this brush work best?
- Passenger car, light truck, truck, bus, and OTR tire mold maintenance operations where tread pattern release is critical.
- Tread segment cavities with deep grooves, ribs, and micro-sipes that collect fine rubber particles and release agent.
- Sidewall lettering, serial numbers, and engraved logos where normal cleaning brushes cannot reach the base of fine characters.
- Bead rings, container mold flanges, and parting line faces where residue disrupts mold closing alignment.
- Vent holes and spring vents that require periodic opening to prevent trapped-air defects and curing pressure problems.
- Mold cleaning stations in tire plants and retread shops where consistent residue removal must be repeated between production cycles.
Which filament survives the cleaning chemicals a nylon tire mold cleaning brush meets?
How small a feature can this brush clean?
With fine filament in the 0.15–0.20 mm range, the brush can enter sipes, lettering strokes, and vent openings down to approximately 1 mm. Features below that size may require a specialized needle probe or micro-brush. Send the smallest groove or lettering dimension and we can confirm whether this construction will reach it.
How can I tell whether the brush is actually removing residue and not just moving it around?
After brushing a test area, wipe the cavity with a clean white cloth or swab. If dark residue continues to transfer after repeated passes, the filament density or stiffness is too low for the deposit, or a cleaning agent is needed. Increasing the contact pressure is not a substitute for the correct filament selection.
Can I use this brush on a rotary or power tool?
Yes, in the shank-mounted configuration. Keep the speed low enough to prevent the nylon filament from overheating, fusing, or glazing at the tips. If the filament ends appear melted, flattened, or shiny, reduce speed or switch to a larger filament diameter that sheds heat more effectively.
How should I store the brush between cleaning cycles?
Hang the brush or store it upright so the filament does not take a permanent set. Keep it away from strong solvents that can attack the handle or ferrule, and inspect the filament before each use for matting, bending, or loss of trim shape. A brush that no longer reaches the bottom of a groove should be replaced or re-trimmed.
Will the nylon filament leave residue inside the mold?
Normal use produces minimal shedding. If you see frequent filament fragments in the mold, the filament is likely being overdriven against a rough surface or being used at too high a temperature. Switch to a coarser filament, reduce pressure, or allow the mold to cool further before cleaning.
Does this brush work on both steel and aluminum tire molds?
Yes. For aluminum molds, select the softer PA6 filament or reduce contact pressure to avoid burnishing or visible surface change. A short test on a non-critical area of the mold is the quickest way to confirm that the selected filament and trim produce the right cleaning result without altering the surface finish.
Continue Exploring
Recommended Reading & Related Brush Resources
Custom Handheld Detail Brushes
A handheld detail brush puts the operator's hand pressure into a small place: a seam, a grout line, a vent, a connector, a mold vent or a grinder chute.
See how this type is built
Mold Cavity Cleaning
Molds are brushed to take off release agent, carbonized residue and flash without changing the surface that shapes the part.
See the cleaning job
PA66 Nylon
PA66 is the firm, hard-wearing nylon: stiffer than PA6 at the same diameter, quicker to spring back and longer-lived under abrasion.
Compare this material
PA6 Nylon
PA6 is the everyday nylon: tough, flexible and economical, with good wear and rebound for scrubbing, tube brushes and strips. Its weakness is water.
Compare this material
Rubber
Rubber is a family of elastomers, not one material.
Compare this material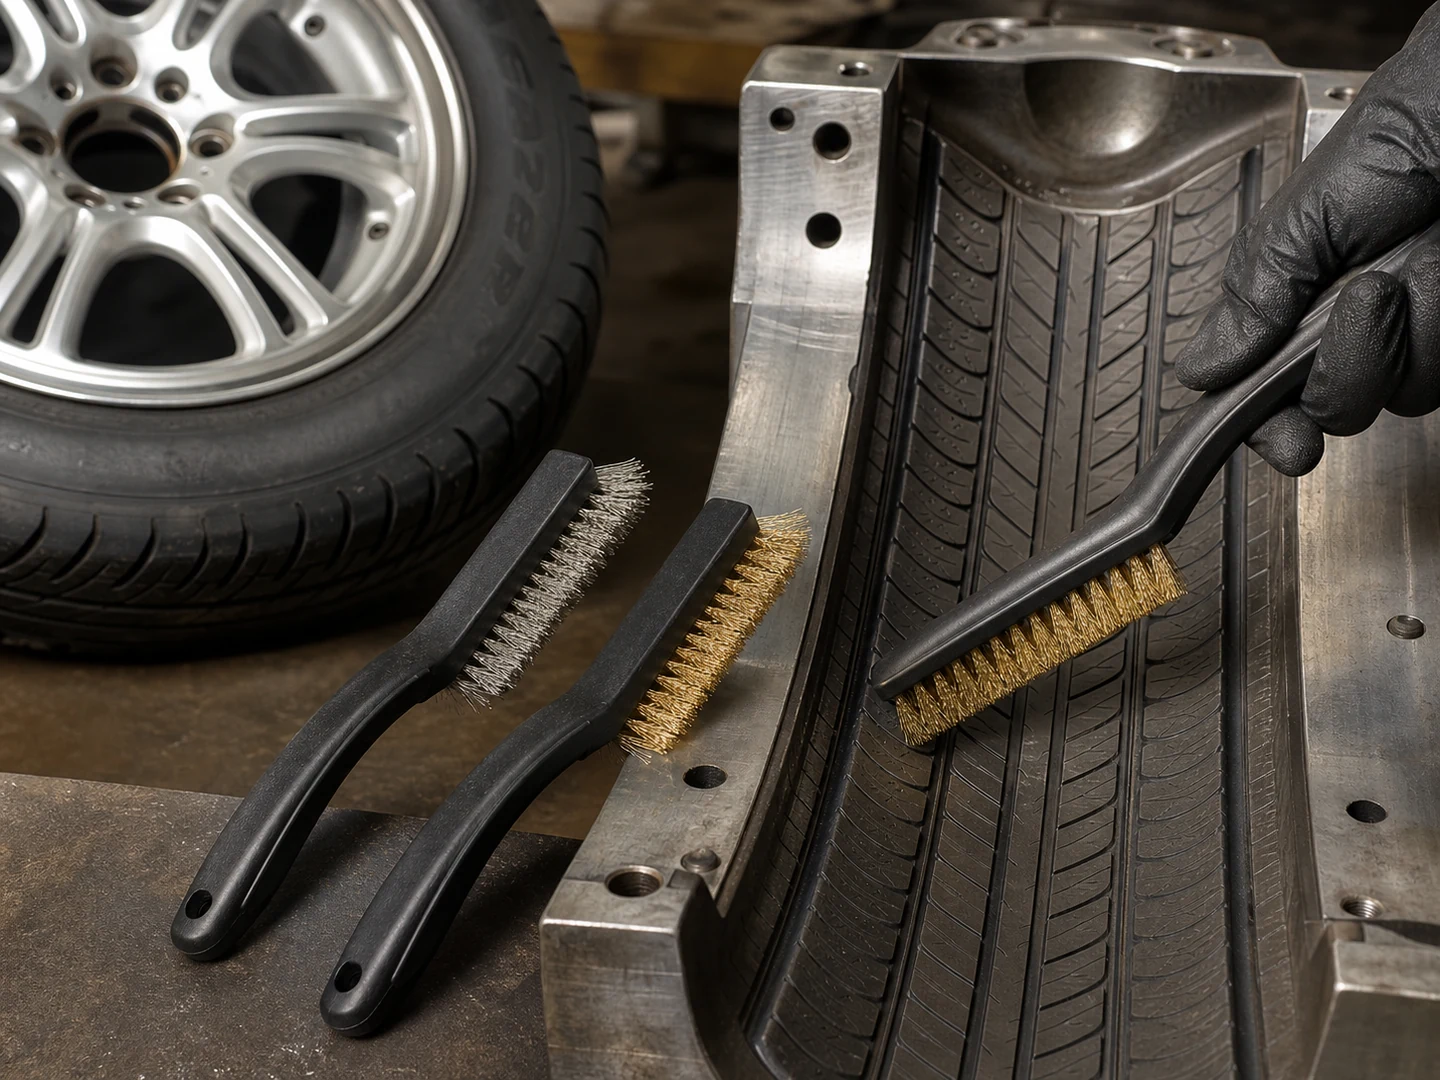
Stainless Steel Brass Mold Tire Brush
316 stainless steel and brass wire mold tire brush in cup, wheel, or end form for tire mold cleaning. Removes cured rubber and release agents.
Compare the specification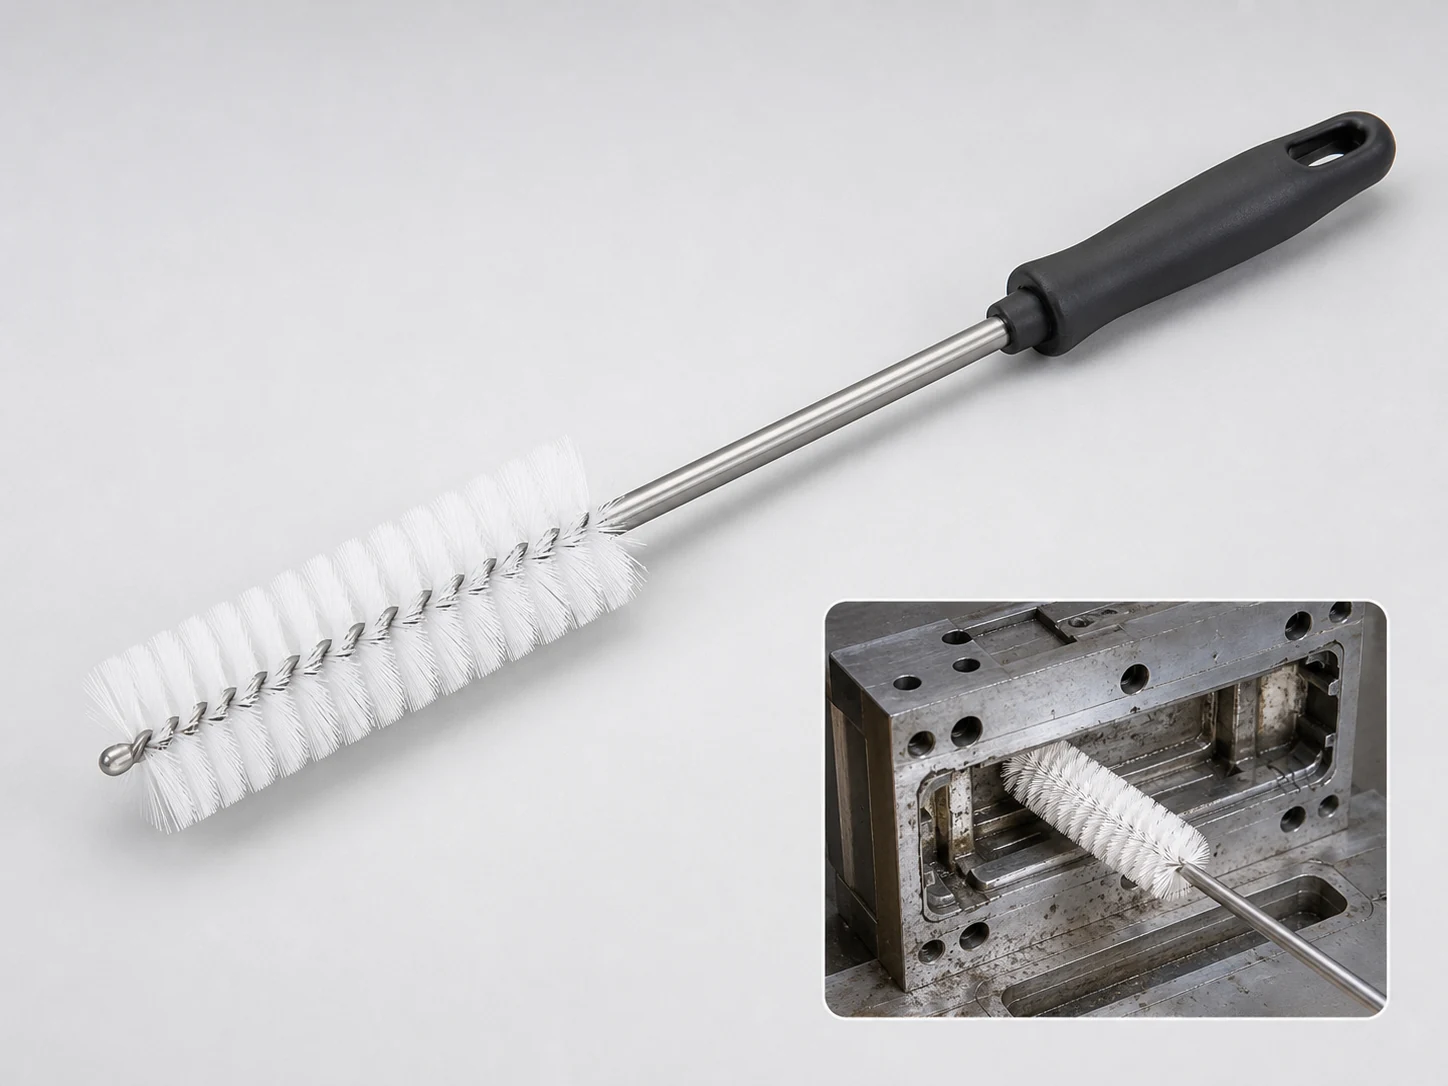
Nylon Mold Detail Cleaning Brush
Head widths 10 to 100 mm and trim 10 to 50 mm reach rib details, vent slots and ejector pockets, lifting release agent without scratching plated steel.
Compare the specification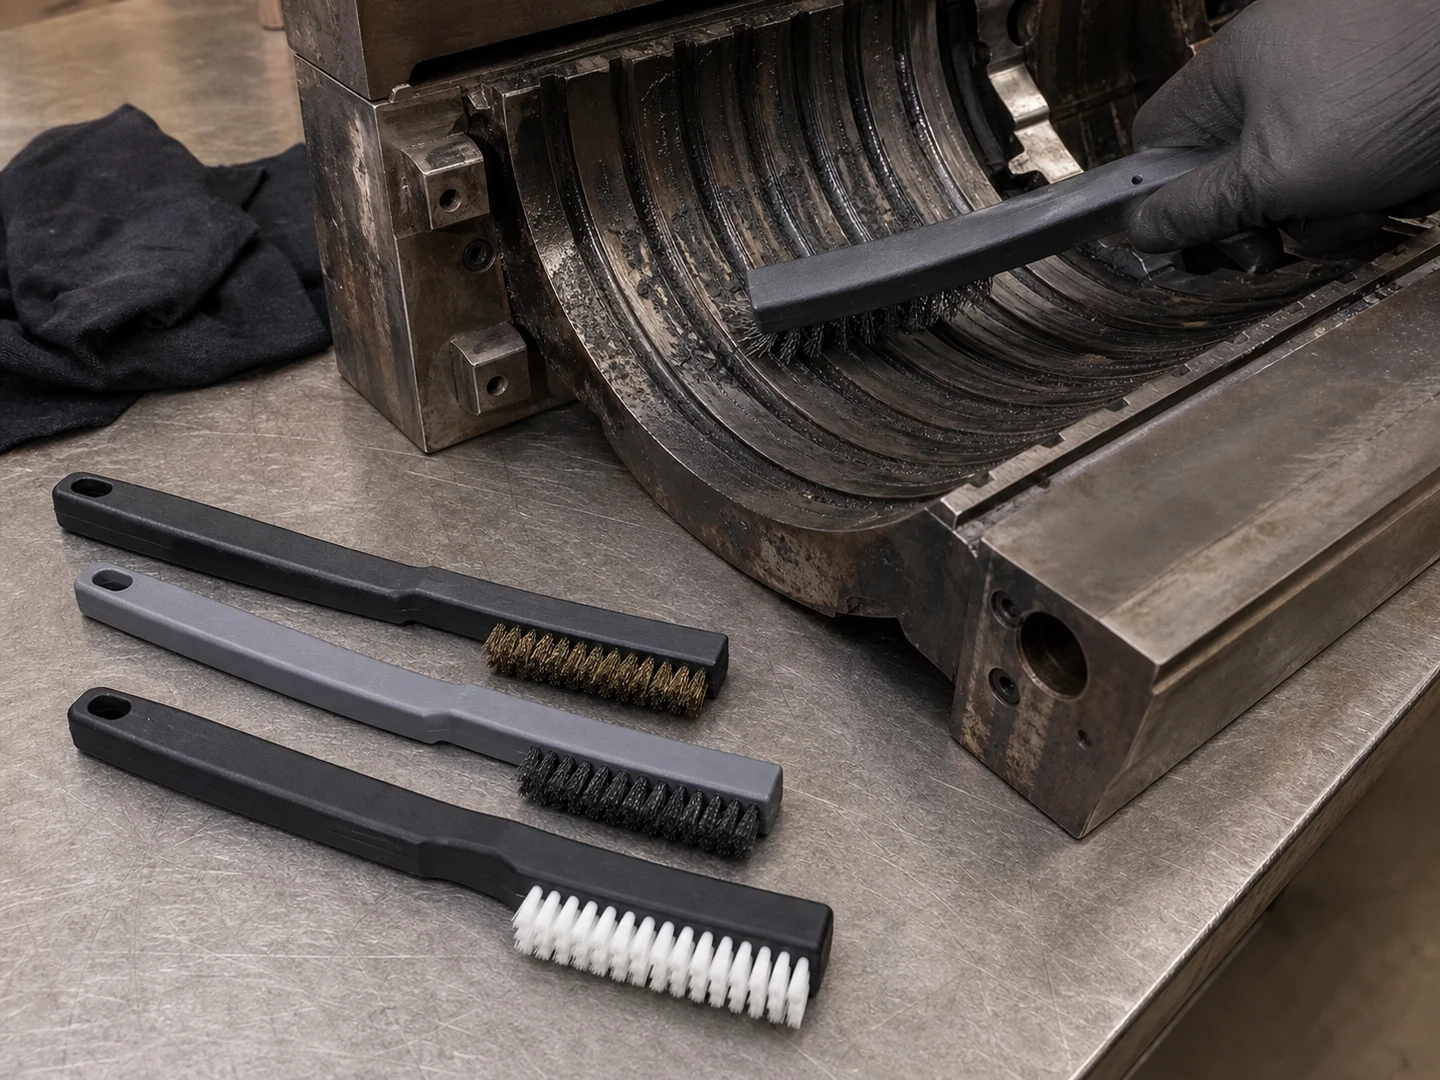
Rubber Mold Cleaning Brush
Rubber Mold Cleaning Brush for mold maintenance: clean release agent, vulcanized flash, carbon, and oils from cavities, vent grooves, and parting lines.
Compare the specificationCustom Manufacturing RFQ
Describe Your Application
For an accurate quotation, please provide the main dimensions, material preference, working surface, residue, quantity, and a drawing or photo.
We reply to every request within 24 hours, with a quotation or with the questions we need answered first. If the brush can be made on our existing tooling, we make the sample directly. If it needs new tooling, we quote a sample fee and a tooling fee, and the sample fee is credited against the bulk order. Need an NDA first? We sign yours before you send drawings, and the files you send are never shown to other customers.
- MOQ500 pcs for small hand-held brushes, 100 pcs for medium and large ones
- SampleTypically 3–7 days
- ProductionFrom 7 days after sample approval, by size and quantity
- Payment30% deposit and 70% before shipment above US$10,000; smaller orders on agreed terms
Have the old brush? Send a photo on WhatsApp
Drawing or photo optional — it speeds things up, it does not gate the enquiry.
“We need a brush to remove wet residue from a stainless steel conveyor, about 800mm wide. The current brush wears quickly. We can send photos.”
“We sell drinkware and need a cleaning brush to include with the product. Quantity around 5,000 pieces.”