
Application
Ceramic Glaze Line & Tile Brush Use
Ceramic Glaze Line & Tile Brush Use is a process-use page rather than a general cleaning category. Select the brush from the required contact function, working surface, motion, and interface, then verify how Ceramic dust / glaze slurry / overspray / kiln debris and Ceramic Production Line / Dusty Industrial Area affect the construction.
At a glance
- Cleaning target
- Ceramic dust / glaze slurry / overspray / kiln debris
- Working environment
- Ceramic Production Line / Dusty Industrial Area
- Cleaning method
- Dry Brushing / Wet Brushing
- Requirements to check
- Process contamination, surface-marking and dust-control requirements
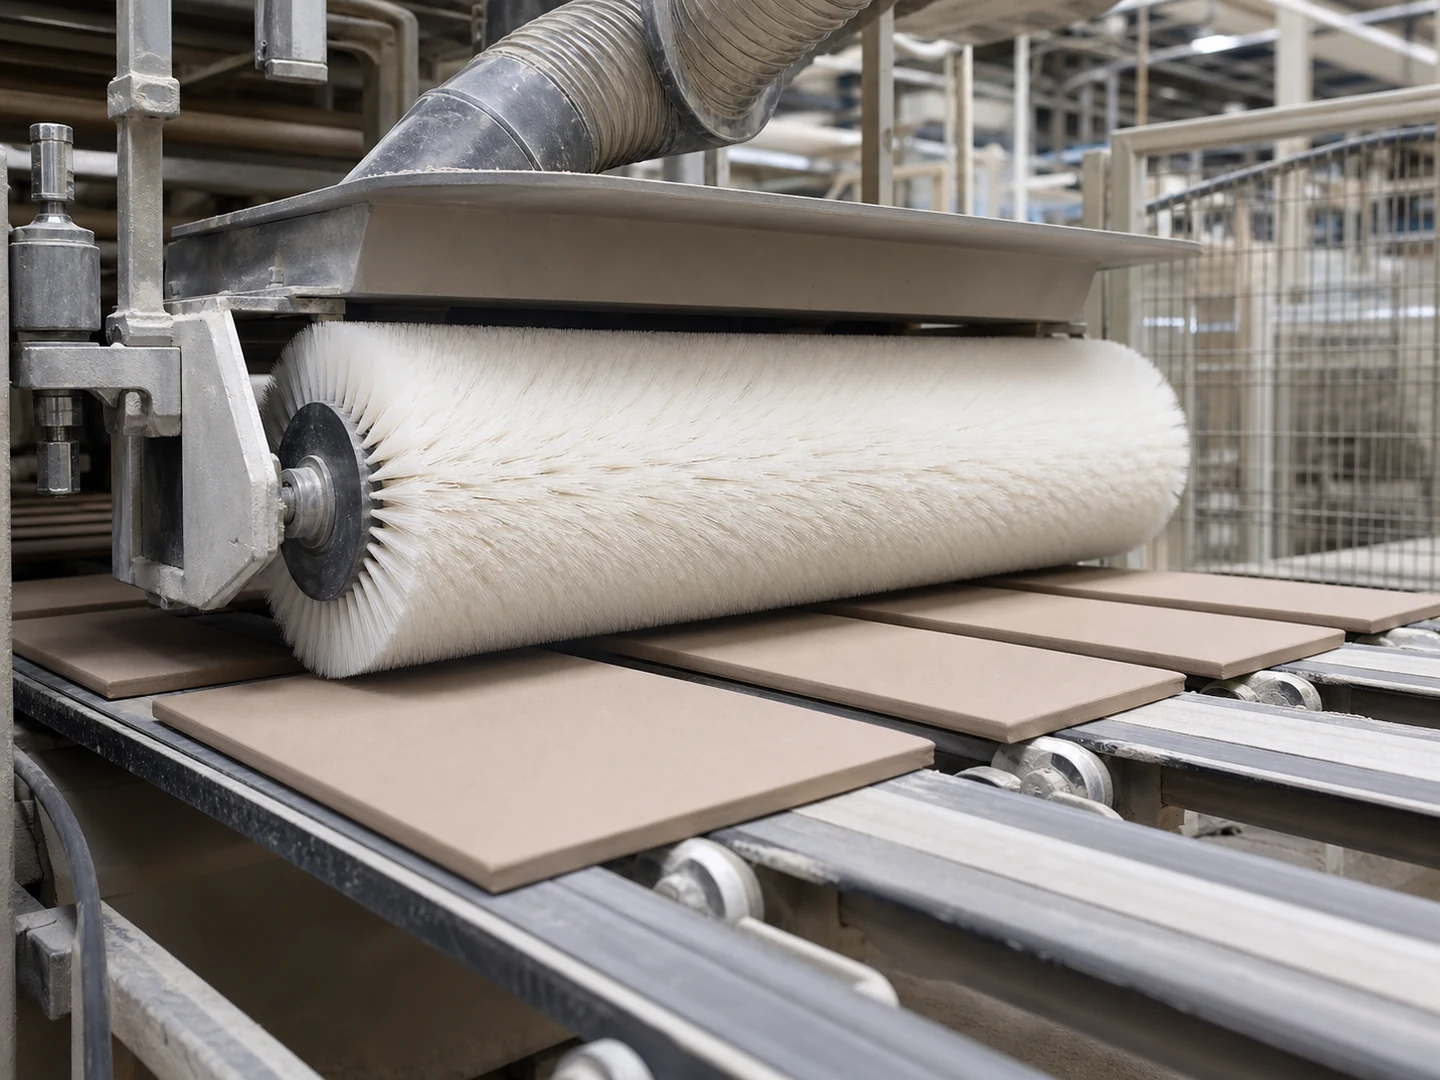
A tile line needs two brush families at once: full-width rollers that transport and dust the ware continuously, and localized abrasive brushes that work edges, glaze residue and oxide.
What makes Ceramic Glaze Line & Tile Brush Use different from other industrial and manufacturing cleaning?
The main difficulty is removing burrs, oxide, glaze, coating, sanding dust, and texture peaks from metal, wood, ceramic, glass, leather, and machined surfaces without damaging the surface, loading the brush, or carrying contamination back into the process.
The work happens in ceramic production line and dusty industrial area against ceramic dust, glaze slurry, overspray and kiln debris.
The part people get wrong: the residue tells you the filament, but the access opening tells you the construction. Get them in that order and the shortlist is short.
What are the most common cleaning targets in Ceramic Glaze Line & Tile Brush Use?
5 targets, each with its own opening, residue and contact requirement.
| Part or area | Residue type | Cleaning requirement |
|---|---|---|
| Green-Body Dust Removal | Dust, powder and compacted fines | The head must reach the working face and apply even contact without marking the surface. |
| Glaze Distribution and Leveling | Ceramic dust, glaze slurry, overspray, kiln debris | |
| Tile Edge | The brush must concentrate contact on a small feature without touching the surrounding surface. | |
| Kiln Roller | The brush must span the working width and hold even contact along the whole face while the surface moves under it. | |
| Ceramic Surface Deburring | The filament must cut at a controlled depth and hold the same profile across the whole contact band, because here the surface the brush leaves is the product rather than a by-product. |
The dimensional envelope those targets impose on the brush:
| Parameter | Typical range |
|---|---|
| Process zone | Glaze-line tile faces, edges, and ceramic/stone finishing stations |
| Brush form | Fickert abrasive brush for continuous polishing heads; roller, disc, or strip only where the machine uses that interface |
| T1 reference | 140 mm Fickert format is used on granite/stone polishing systems |
| T2 reference | 170 mm Fickert format is used on ceramic/artificial-quartz polishing systems |
| Abrasive fill | Diamond or silicon-carbide abrasive filaments in a nylon carrier according to substrate and finish |
| Machine data | Holder type, grit sequence, working length, and line parameters come from the actual polishing machine |
Which brush types work for each cleaning target?
Use full-width rollers or lath/strip brushes for continuous tile-line transport and dust removal; use disc/composite abrasive brushes for localized glaze residue, oxide removal, edge work, texturing, or finish correction. Base diameter, bore, core, shaft and working width on the actual machine drawing.
| Cleaning target | Recommended brush type | Why it fits |
|---|---|---|
| Green-Body Dust Removal | Handheld Detail Brushes | An unfired body marks under any load, so a hand-guided head lets the operator take dust off with the least contact that still moves it. |
| Glaze Distribution and Leveling | Here the brush applies rather than removes, so a hand-guided head is what spreads the slurry evenly and pulls out the ridge left by the pour. | |
| Tile Edge | Wheel Brushes | The edge is a narrow band alongside a finished face, so a wheel brush concentrates contact on that band and stays off the glaze. |
| Kiln Roller | Roller and Conveyor Brushes | Glaze drips fuse to the roller and print into the next tile, so a roller brush riding the shaft removes them while the line keeps running. |
| Ceramic Surface Deburring | Handheld Detail Brushes | A fired face is flat and hard, so a flat head with abrasive filament works the whole area at once and takes the burr down without dishing the surface. |
The layouts this application is normally built in:
- Driven brush — use when burrs, oxide, glaze, coating, sanding dust, and texture peaks needs repeatable scrubbing or controlled relative movement
- Passive or free-running brush — use for loose contamination and lower process complexity on metal, wood, ceramic, glass, leather, and machined surfaces
- Localized hand, strip, or tube brush — use where only an edge, gap, port, or maintenance point needs contact
In practical brush terms: reach first, then residue. A brush that fits but is too soft can be stiffened; a brush that does not fit is simply the wrong tool.
What filament materials work best for Ceramic Glaze Line & Tile Brush Use?
Use soft nylon or natural fiber for dusting and glaze control; choose abrasive nylon, diamond, or ceramic abrasive only for a defined fired-surface finishing step.
| If the condition is… | Filament to start with | Why |
|---|---|---|
| Dust on a green body before firing | Horsehair | lifts dust without leaving a mark in the unfired surface |
| Glaze slurry and overspray on the line | Nylon PA | washes clean and does not carry pigment into the next colour |
| A defined finishing step on fired ware | Abrasive Nylon | cuts the fired surface, and only in a step the process defines |
The constraints this application puts on the filament:
| Constraint | Value for this application |
|---|---|
| Filament hardness | Soft to Medium |
| Maximum service temperature | 120°C |
| Chemical exposure | Water-based glaze, pigments, mild alkaline cleaner and abrasive ceramic dust |
| Cleaning method | Dry Brushing, Wet Brushing |
How do I choose the right brush for my ceramic glaze line & tile brush use equipment?
Two families run on one line: full-width rollers sized to the machine shaft for transport and dusting, plus localised abrasive brushes for edges and glaze.
Work through it in this order:
- Identify the target part and measure the access opening or clearance
- Describe the residue: what it is, how thick it sits, and how strongly it holds
- Choose the construction that can physically reach that target
- Set the filament from surface risk, working temperature and cleaning chemistry
- Fix filament diameter, free trim length and density for the contact pressure you need
- Run one cycle and check the result before committing to a production quantity
Before you commit to a quantity, send the roller length and shaft fitting, the line speed, and the tile format.
When is a ceramic glaze line and tile brush the wrong tool?
Air knives and vacuum extraction remove green-body dust without touching the unfired surface, which is where contact does the most damage. Glaze applied to a set thickness is sprayed or waterfall-applied, because a brush cannot hold that tolerance.
What common mistakes should I avoid in Ceramic Glaze Line & Tile Brush Use?
- Giving tile size instead of the machine’s roller length, shaft fitting and line speed
- Changing brush material while leaving excessive engagement, poor alignment, or no discharge path unchanged
- Copying a worn brush without recording motion, direction, mounting, and the original working diameter
When a brush is running but not cleaning, start here rather than adding pressure:
| Symptom | What to change |
|---|---|
| Residue remains | Increase relative motion or discharge, then change filament diameter or density; do not add pressure before checking loading by burrs, oxide, glaze, coating, sanding dust, and texture peaks. |
| Surface marks or scratches | Reduce engagement, use finer or softer fill, and remove trapped abrasive particles from contact with metal, wood, ceramic, glass, leather, and machined surfaces. |
| Rapid wear or uneven cleaning | Check alignment, runout, support, motion, temperature, chemical attack, and whether the brush covers the complete working path. |
| Brush loads or redeposits residue | Open the fill pattern or add wash, vacuum, air, scraping, or a collection path so removed burrs, oxide, glaze, coating, sanding dust, and texture peaks leaves the contact zone. |
No catalogue item for this yet
Every brush here is made to order, and this one has no catalogue entry so far. Send the working surface, the residue, the access opening and the quantity, and it is quoted through the same specification route as the rest of the range.
Custom Manufacturing RFQ
Discuss This Application
Share the working surface, residue, dimensions, material direction, interface, quantity and drawing or sample photo.
Custom Brush RFQ
Request a Custom Cleaning Brush Quote
Upload a drawing, product photo, or sample photo and provide the core dimensions and cleaning conditions.
“We need a brush to remove wet residue from a stainless steel conveyor, about 800mm wide. The current brush wears quickly. We can send photos.”
“We sell drinkware and need a cleaning brush to include with the product. Quantity around 5,000 pieces.”