
Custom Cleaning Brush
Brass Tube Brush
Brass fill expands into thread roots and cross-hole intersections, clearing chips and carbon while limiting scratch risk on aluminum and copper.
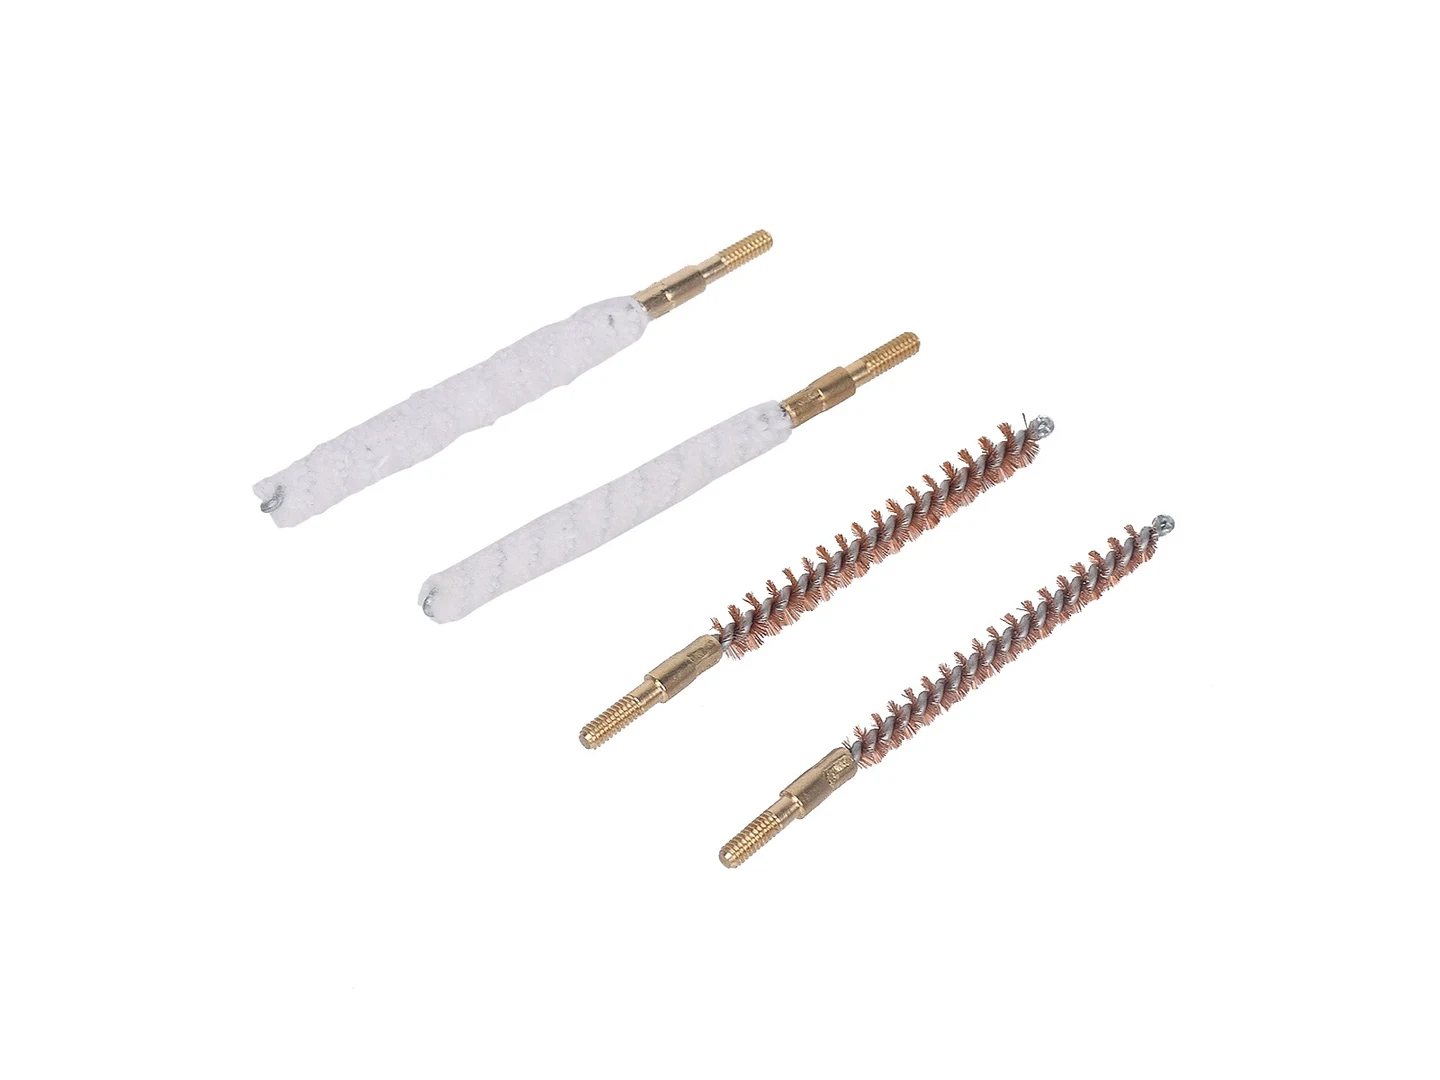
Small brush
500 pcs
Minimum order
Held in one hand: tube, bottle, detail and swab brushes — including long-handled ones with a small head.
Production lead time, once the specification is confirmed
- Up to 500 pcsWithin 7 days
- 501–50,000 pcsWithin 14 days
- Over 50,000 pcsWithin 21 days
Peak season can extend these times; the shipping date is confirmed in writing with your quotation. Sampling and shipping are quoted separately.
A brass tube brush is a wire-fill cleaning tool for bores, tubes, ports, blind holes, threads, and cross-drilled passages. The brass wire fill removes chips, carbon, oil, coolant residues, and light corrosion films while limiting the scratching risk to softer parent materials such as aluminum, copper, brass, and coated surfaces.
What can this brush do for you?
Reaches thread roots and cross-hole intersections
In threaded ports and manifolds, the open brass fill expands into the thread root and the transition where two drilled holes meet. Because the brush is cylindrical, it works the complete internal contour instead of only the visible entry area. Removing chips from these intersections before assembly prevents jamming, thread galling, and seal damage.
Cuts process residue without cutting into soft base metal
Brass is softer than hardened steel and most stainless grades but firmer than typical carbon, varnish, oil film, and coolant residue. The wire tips scrape away attached deposits from aluminum, copper, brass, and precision bores without the deep scoring a stainless fill can produce. That is the reason brass is selected on sealing surfaces and reusable machined parts.
Reduces spark risk around fuel and hydraulic residues
A brass wire fill is the safer choice for maintenance around fuel lines, injection ports, hydraulic oil, and solvent vapors because brass-on-metal contact produces a much lower spark hazard than steel-on-metal contact. This is not a substitute for proper purging and ventilation, but it removes one ignition variable from the service procedure.
Works by hand or on a rotary drive
The brush can be built with a plain end, loop, ring, threaded connection, or drill shank. Hand versions offer controlled pressure in small ports and sensitive assemblies. Driven versions speed up carbon and varnish removal in production and rebuild operations. The stem construction changes the access and torque path without changing the cleaning action of the brass fill.
Long fill sections keep continuous contact inside the bore
Brush section lengths from 25 to 127 mm give continuous wire coverage along the tube wall. An operator can clean the full working length in one or two strokes instead of working one small ring at a time, and the fill flexes over internal steps and cross-hole edges rather than stopping at them.
What is a Brass Tube Brush?
A brass tube brush is a cylindrical cleaning brush in which brass wire filaments are captured in a spiral around a twisted metal stem. It is made to be inserted into a bore or tube and rotated or stroked so the wire ends contact the internal wall, thread roots, chamfers, and cross holes. The fill cleans by wire-tip contact and spiral drag: each wire behaves like a short resilient spring that scrapes surface deposits while flexing over the base material instead of cutting into it.
In most configurations, the stem is a twisted steel wire core that also holds the brass filament bundle. Single-stem brushes use one twisted core and are lighter for smaller bores; double-stem designs use two cores for more fill stability in larger diameters. End connections include a plain cut end, loop, ring, threaded shank, or drill arbor depending on whether the operator drives the brush by hand or with a rotary tool.
This is a surface-cleaning tool, not a material-removal or deburring cutter. Brass tube brushes remove process deposits and soft to moderate films while leaving the original bore geometry intact. For hard scale, weld spatter, or heavy rust, another fill type is more appropriate. The brass fill is also consumable: it wears intentionally in use and should be replaced when the wire ends lose their edge or the diameter falls below contact size.
Technical Specifications
The values below are the standard production range. Brush outside diameter, filament diameter, section length, overall length, and stem end are selected to the bore geometry and cleaning process.
| Parameter | Value / Options |
|---|---|
| Brush outside diameter | 3.2–50.8 mm |
| Filament material | Brass wire |
| Filament diameter | 0.08–0.25 mm |
| Brush section length | 25–127 mm |
| Overall length | 152–406 mm |
| Stem construction | Single stem, double stem, twisted core, or flexible extension |
| Stem end | Plain, loop, ring, threaded, drill shank, or customer-specified connection |
| Stem material | Galvanized carbon steel standard; 304 stainless steel optional |
| Fill density | Standard or dense, selected by deposit type and bore clearance |
| Contact fit | Near-size to light interference for wire fill; heavy oversize increases torque and shortens brush life |
| Operating condition | Oil, fuel, coolant, and common degreaser exposure; low-to-medium rotary speed for power use |
| Brush type | Custom Tube & Pipe Bore Brushes |
| How it is driven | Hand-guided |
| Cleaning target | Bores, tubes, ports and passages in softer metals and coated parts |
| Surface or part | Bore walls, thread roots, chamfers, blind holes and cross holes |
| Residue or debris | Chips, carbon, oil, coolant residue and light corrosion film |
| Mounting / connection | Threaded Removable / Fixed |
Where does this brush work best?
- Hydraulic manifolds and valve bodies — clean ports, spool bores, threads, and cross-hole intersections after machining, removing chips, cutting oil, and oxidation film before assembly.
- Threaded pipe ends and fittings — clean NPT and BSP tapered and straight thread roots where old sealant, rust film, and contamination remain. Brass removes the residue without changing the thread form.
- Heat exchanger and condenser tubes — wipe sludge, light scale, and raw-water film from tube IDs before inspection or re-tubing. Brass is generally safer than steel fill on copper-alloy tubes.
- Engine and fuel system service — carburetor ports, injector bores, oil galleries, and brake cylinder bores where fuel or oil residues are present and spark risk must be controlled.
- Blind holes and oil passages — clear drilling chips, coolant residue, and fine metal particles from machined cross holes and bottom areas ahead of final flushing and assembly.
- Small-bore instrument and maintenance work — tubes, ports, and chambers where a brass wire fill provides controlled deposit removal without aggressive surface damage.
How do I choose the right one?
Measure the bore ID and thread root, not just the call-out size
A threaded port has a major diameter, minor diameter, and thread root. Choose the brush OD for the area the wire must actually contact. For blind holes, measure the full depth. For cross-drilled passages, measure from the access side to the farthest intersection. A wire fill should be near-size to lightly oversized for the bore. If the brush will not enter without bending the core, the OD is too large; if it slides through with no contact, the OD is too small to clean.
Match filament diameter to surface and residue
Fine 0.08–0.15 mm brass wire is more compliant and better for soft aluminum, copper, precision bores, and fine thread roots. Heavier 0.18–0.25 mm wire is more aggressive and removes heavy carbon and varnish faster, but it leaves more visible contact marks. If surface finish is controlled, always test on a scrap part before committing the production brush.
Choose stem style around access and motion
Single-stem construction is lighter and easier to enter restricted passages; double-stem construction supports a larger or longer fill and handles more working pressure in bigger bores. If the passage bends, choose a flexible extension and a shorter brush section. If the brush will be driven by a drill or machine, specify the shank and keep the speed controlled. For hand service, a loop or ring end gives better operator grip and a hanging point at the workbench.
Check the deposit, not just the bore size
Brass works on oil, coolant, carbon, chips, light rust, and process films. It is not the right choice for heavy scale, hard rust, or sintered build-up. If the deposit needs sharp aggressive cutting, use stainless steel or abrasive nylon fill. If the job is only wiping light oil with no marking allowed, a nylon or horsehair tube brush may be the better tool.
| Condition | Brush choice |
|---|---|
| Fine thread in aluminum or copper part | 0.08–0.12 mm brass wire, near-size OD, hand use |
| Carbon or varnish in straight steel or iron bore | 0.15–0.20 mm brass wire, slight interference, optional drill shank |
| Curved internal passage | Flexible extension, shorter brush section, smaller OD |
| Hard scale or heavy rust | Switch to stainless steel or abrasive fill; brass will wear rapidly |
| Cosmetic surface with no marking allowed | Use nylon or horsehair fill, or test fine brass on scrap first |
Can I customize this brush?
Each brass tube brush can be adjusted to the bore and process. We will need the bore ID, thread or taper detail, internal depth, cross-hole positions, access path, drive method, base material, deposit type, and cleaning fluid. A drawing or sample part shortens the specification time.
We can adjust:
- Fill dimensions — brush OD, section length, and overall length matched to bore depth and access clearance
- Wire — filament diameter, wire hardness, fill density, and section construction
- Stem — single or double stem, twisted core, core diameter, galvanized or 304 stainless steel, and flexible extension for curved passages
- End connection — loop, ring, eye, threaded shank, hex connection, drill shank, or quick-change interface
- Handle — manual handle, knurled grip, ergonomic form, loop, or hanging feature for handheld versions
- Drive configuration — designed for hand use, low-speed drill, or machine-driven operation
- Marking, color, and packaging — pad-printed identity marking, color coding, bulk packing, or individual project packaging
Which filament lasts longest on a brass tube brush?
What is the difference between single-stem and double-stem construction?
Single-stem brushes use one twisted core and are lighter and easier to guide through smaller bores and restricted access. Double-stem construction holds a larger, more stable fill for bigger diameters or heavier working pressure. If the bore entry is narrow, single-stem is often easier; if you need more wire mass and longer wear in a straight bore, double-stem is the stronger choice.
Will a brass wire brush scratch stainless steel or aluminum?
Brass is softer than hardened steel and most stainless grades, so it normally leaves burnishing or light contact marks rather than deep scoring. On aluminum or polished parts, even light pressure can still leave visible marks. For controlled surfaces, use fine 0.08–0.12 mm filament and trial the brush on a scrap part. If absolutely no marking is allowed, switch to nylon or horsehair fill.
Can I run this brush on a drill?
Yes, when the stem end is configured as a drill shank and the speed is kept low-to-medium. High RPM plus heavy feed generates heat, flattens the wire ends, and shortens brush life. Short passes with light pressure usually clean carbon and varnish faster than forcing the brush to dwell against the bore wall.
How do I inspect a brass tube brush before use?
Check the twisted core for bends or unwinding, the fill for loose or broken filaments, and the OD against the measured bore. Pass the brush through a clean tube once and observe whether the fill contacts the full internal section. If the diameter has worn below near-size contact, replace the brush rather than increasing pressure to compensate.
Does brushing replace flushing or rinsing?
No. Brushing loosens and removes attached deposits, but loose debris still has to be carried out by solvent flush, air blow, rinse, or vacuum. After brushing, flush the passage and verify the result by checking the outflow or wiping a clean white cloth through the bore until no residue transfers.
When should I not use a brass tube brush?
Do not use brass fill for thick hardened scale, heavy rust that requires steel wire, or strongly bonded sintered deposits. Avoid it in systems where brass color or metal particle contamination is unacceptable. For high-purity or no-metal-contact applications, specify a nylon, PBT, or other polymer fill with a compatible stem material.
Guides that go deeper on this
Continue Exploring
Recommended Reading & Related Brush Resources
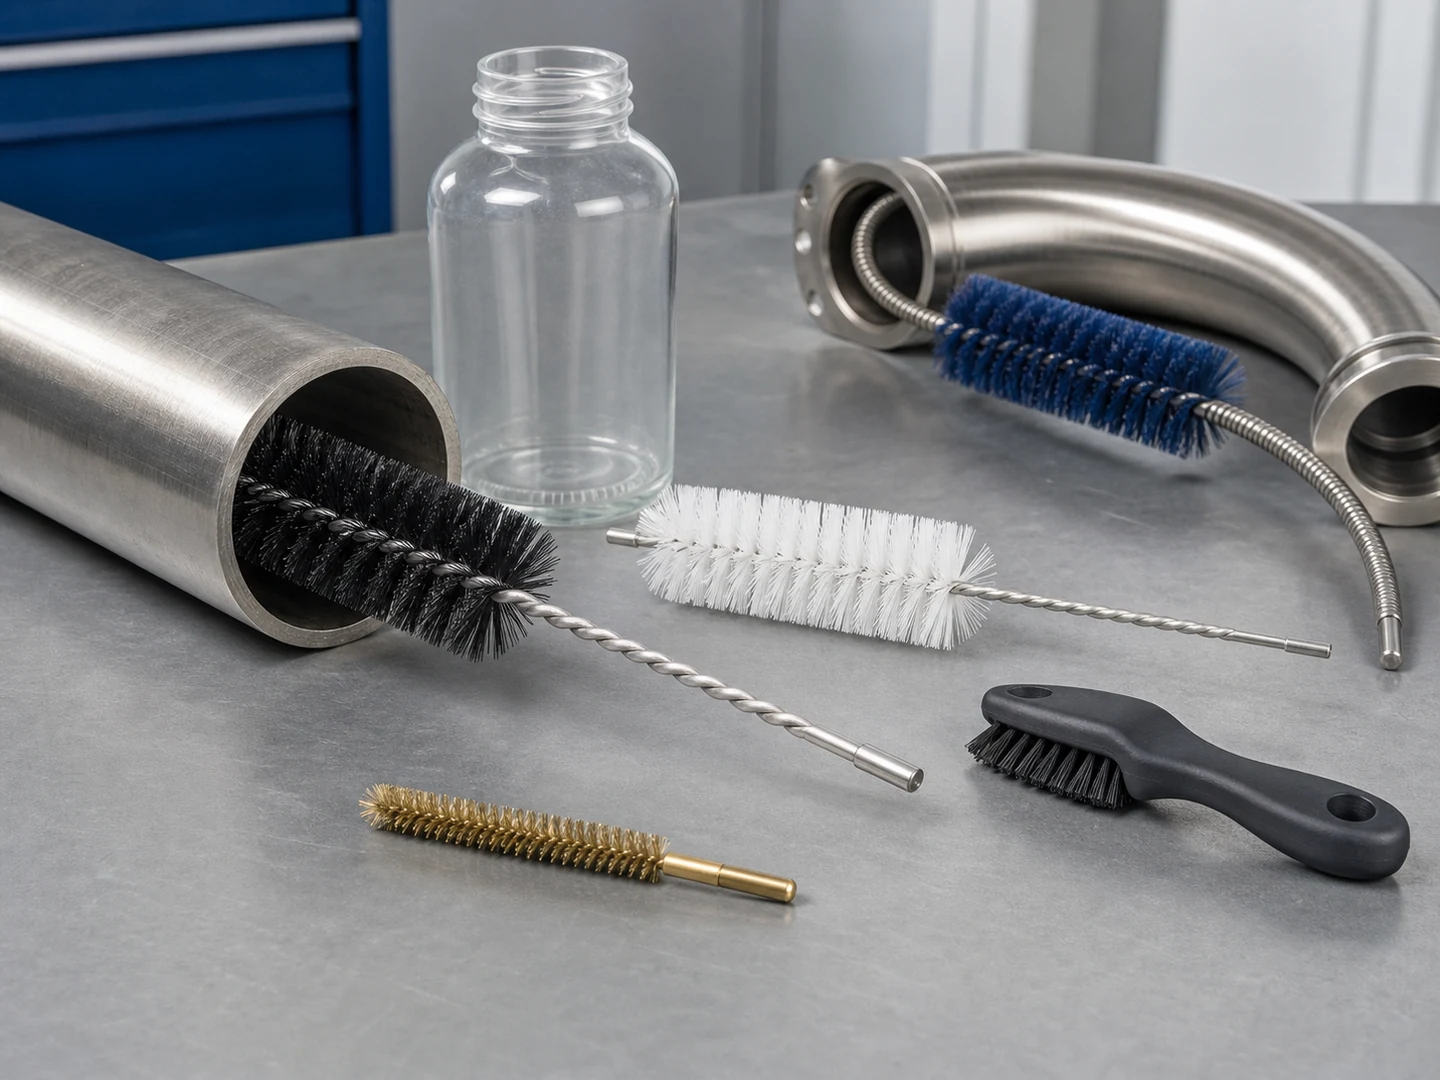
Custom Tube & Pipe Bore Brushes
A tube or bore brush cleans the whole inside circumference of one passage as it is pushed, pulled or turned along it.
See how this type is built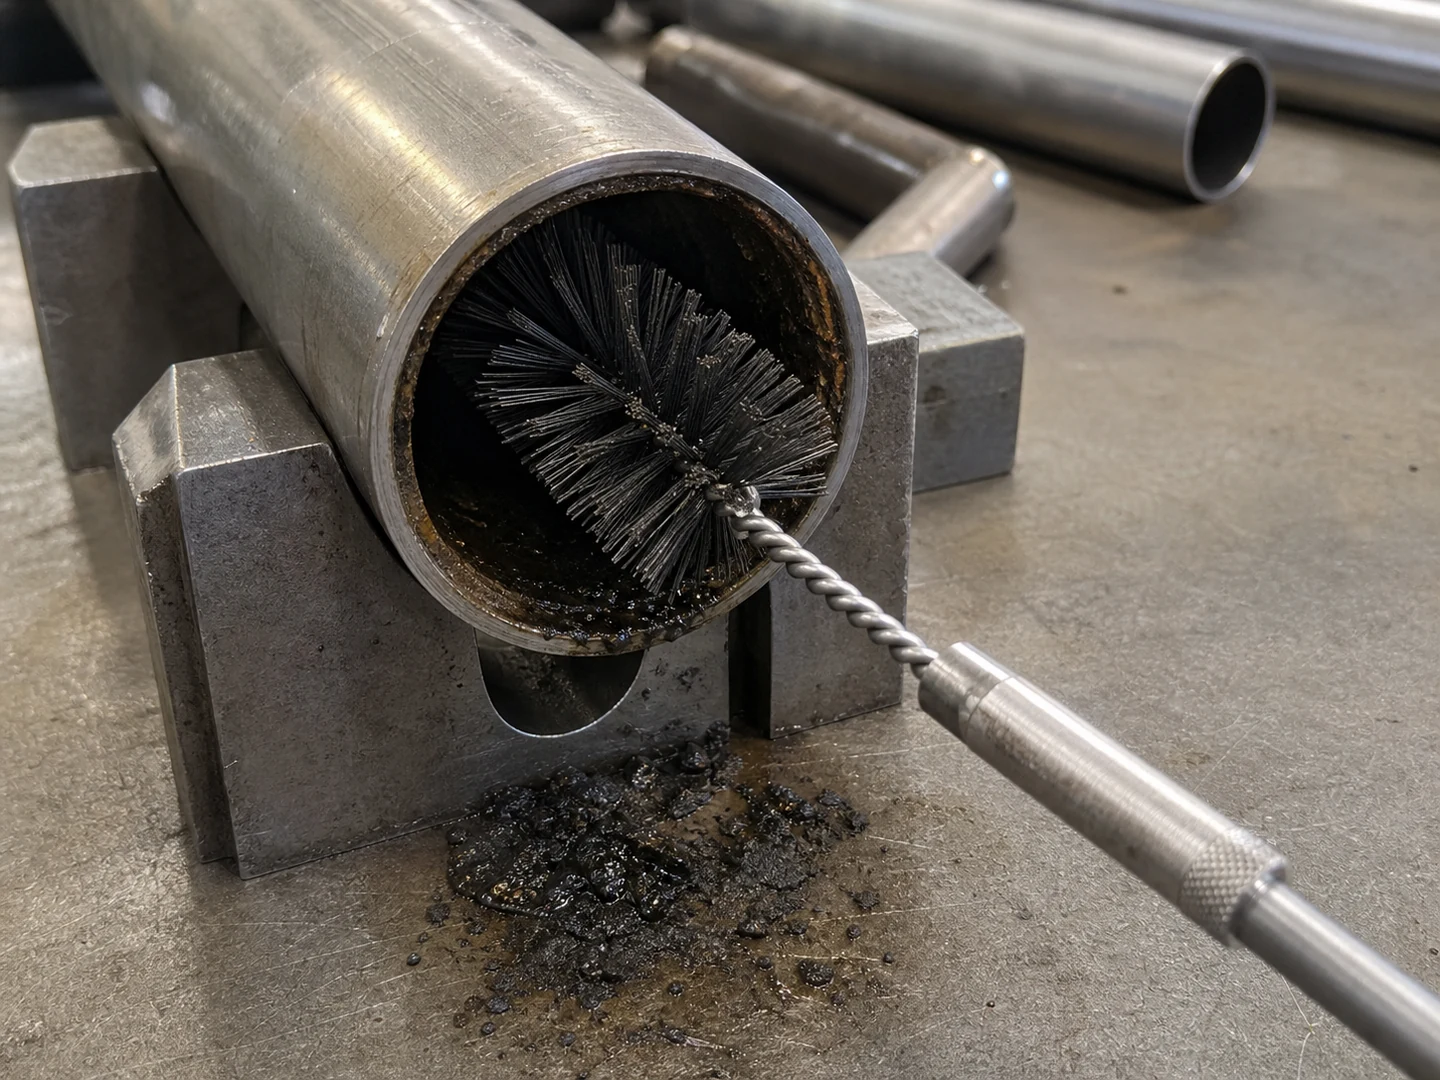
Tube & Pipe Cleaning
Tube and pipe brushes are twisted-wire bore brushes sized to the inside diameter: near-size to wipe, 5–20% oversize with nylon or PBT to scrub.
See the cleaning job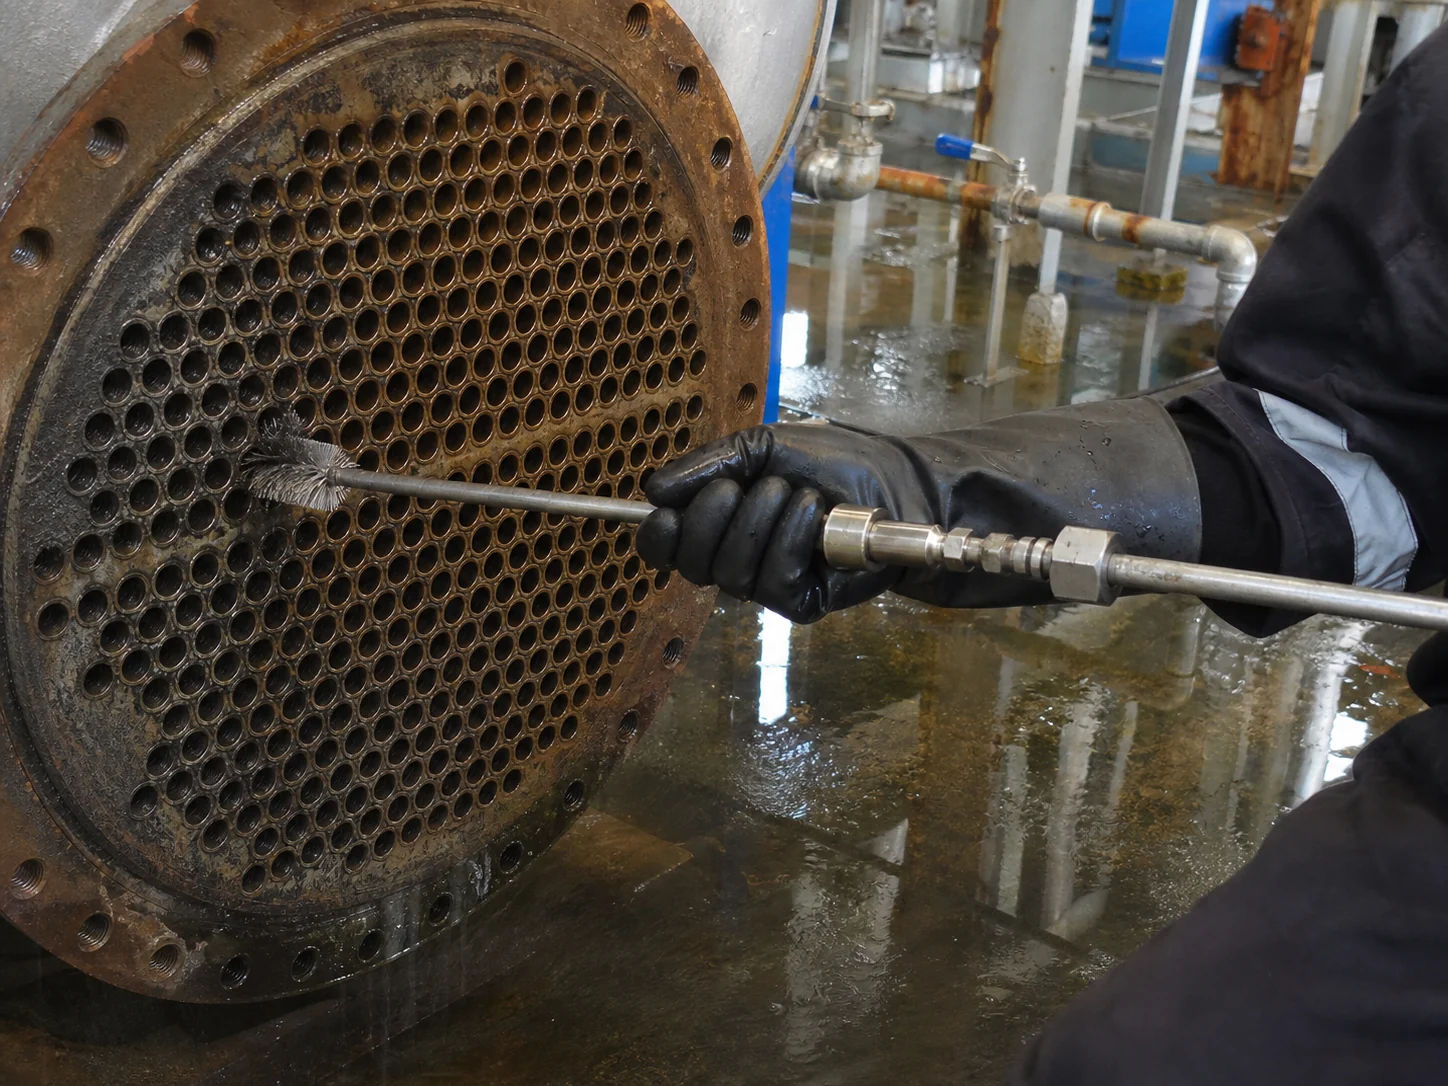
Heat Exchanger Tube Cleaning
A heat exchanger tube is judged by how much clean wall it gets back, because even a thin layer of scale or biofilm costs heat transfer.
See the cleaning job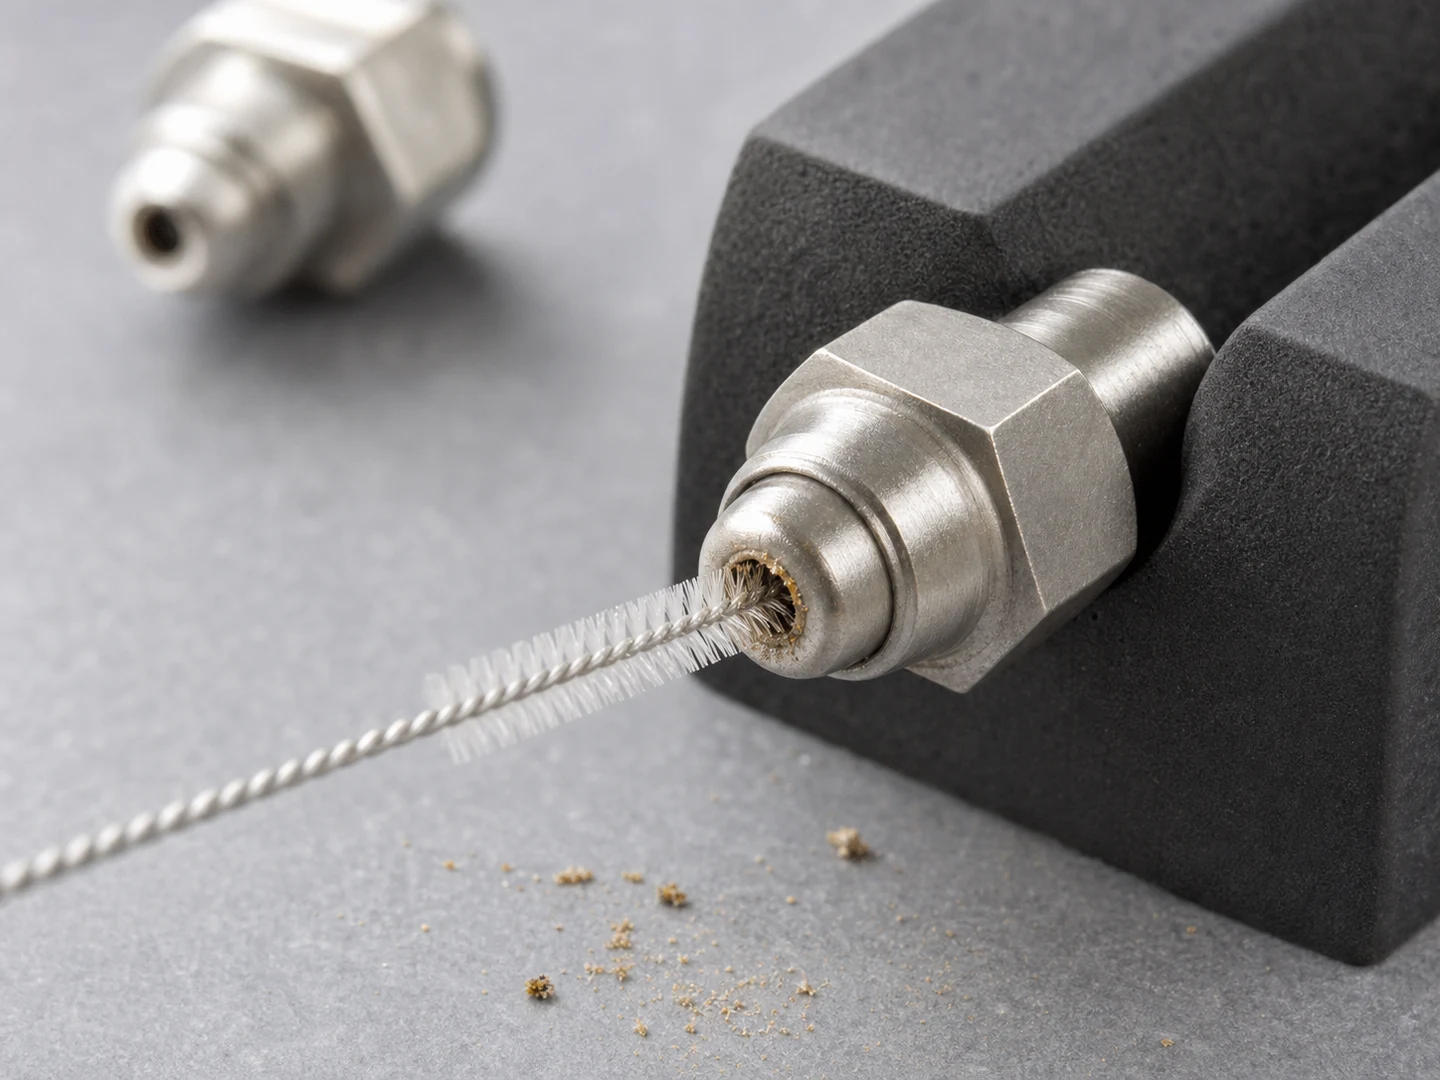
Nozzle Cleaning
A nozzle brush must clean the deposit without changing the orifice, because the orifice size sets the spray, the flow or the fuel-air ratio.
See the cleaning job
Brass Wire
Brass wire is softer than steel, so a brass brush removes carbon, release agent, oxide and light rust from steel surfaces with far less marking.
Compare this material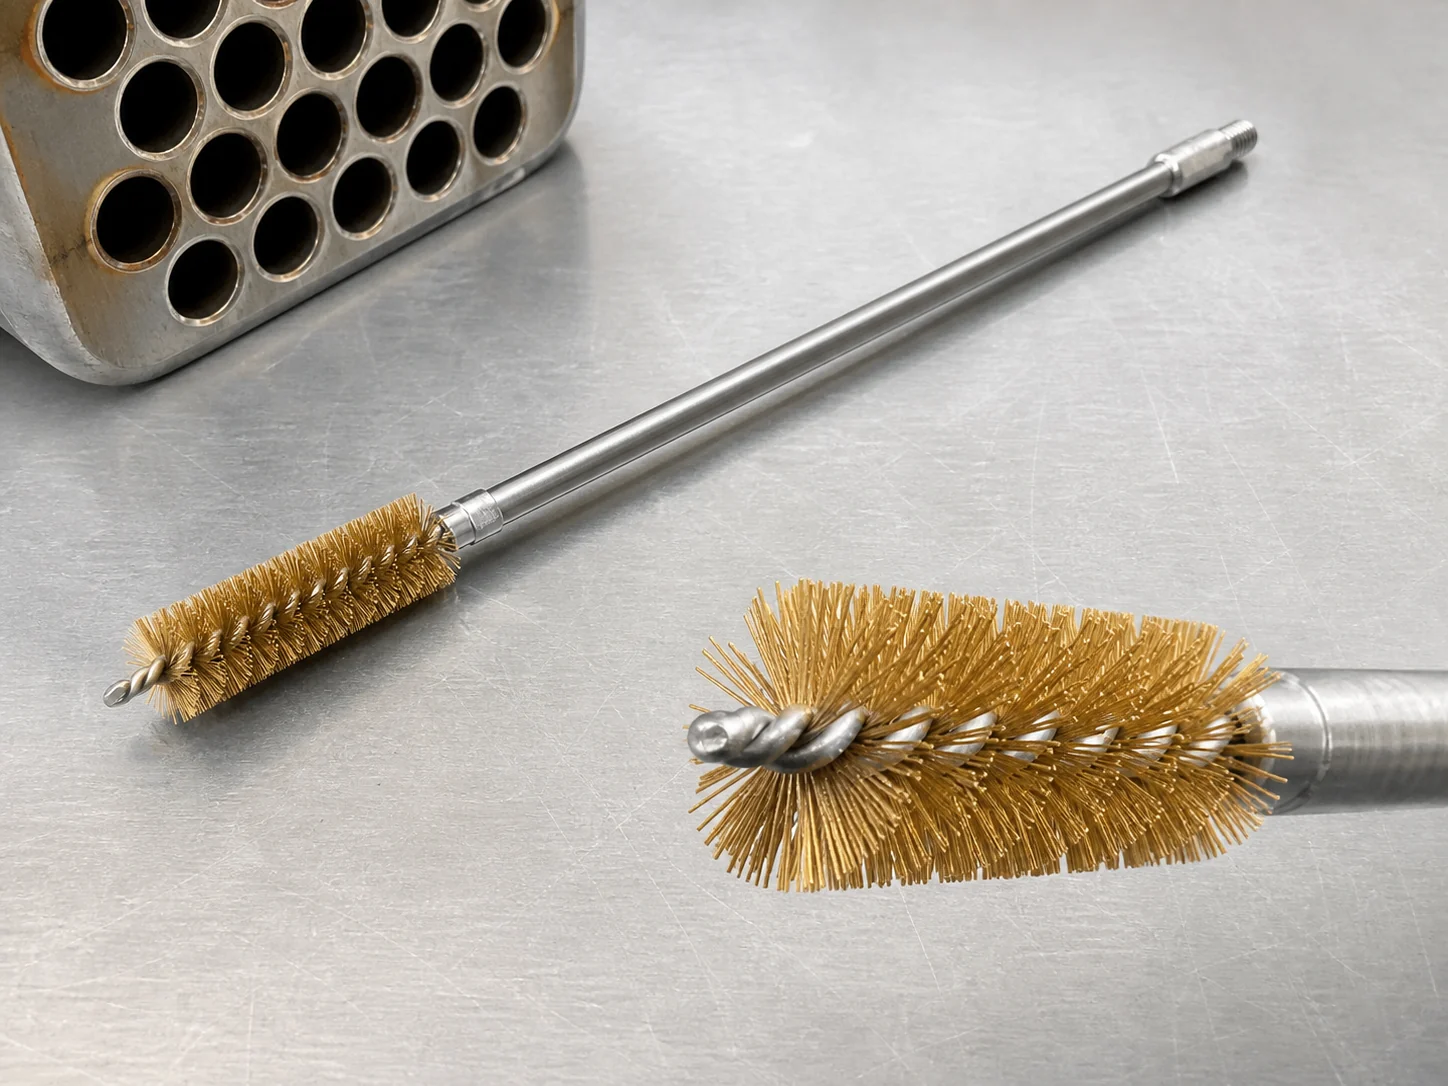
15mm Brass Tube Brush
15mm brass tube brush with waved wire fill and threaded 304 stainless steel handle for small-bore heat exchanger and condenser tube cleaning.
Compare the specification
Pastry Tube Brush
Custom pastry tube brush for piping tips and nozzles. Food-contact PBT/nylon fill, stainless wire core, hot-wash and autoclave options, sized to tube ID.
Compare the specification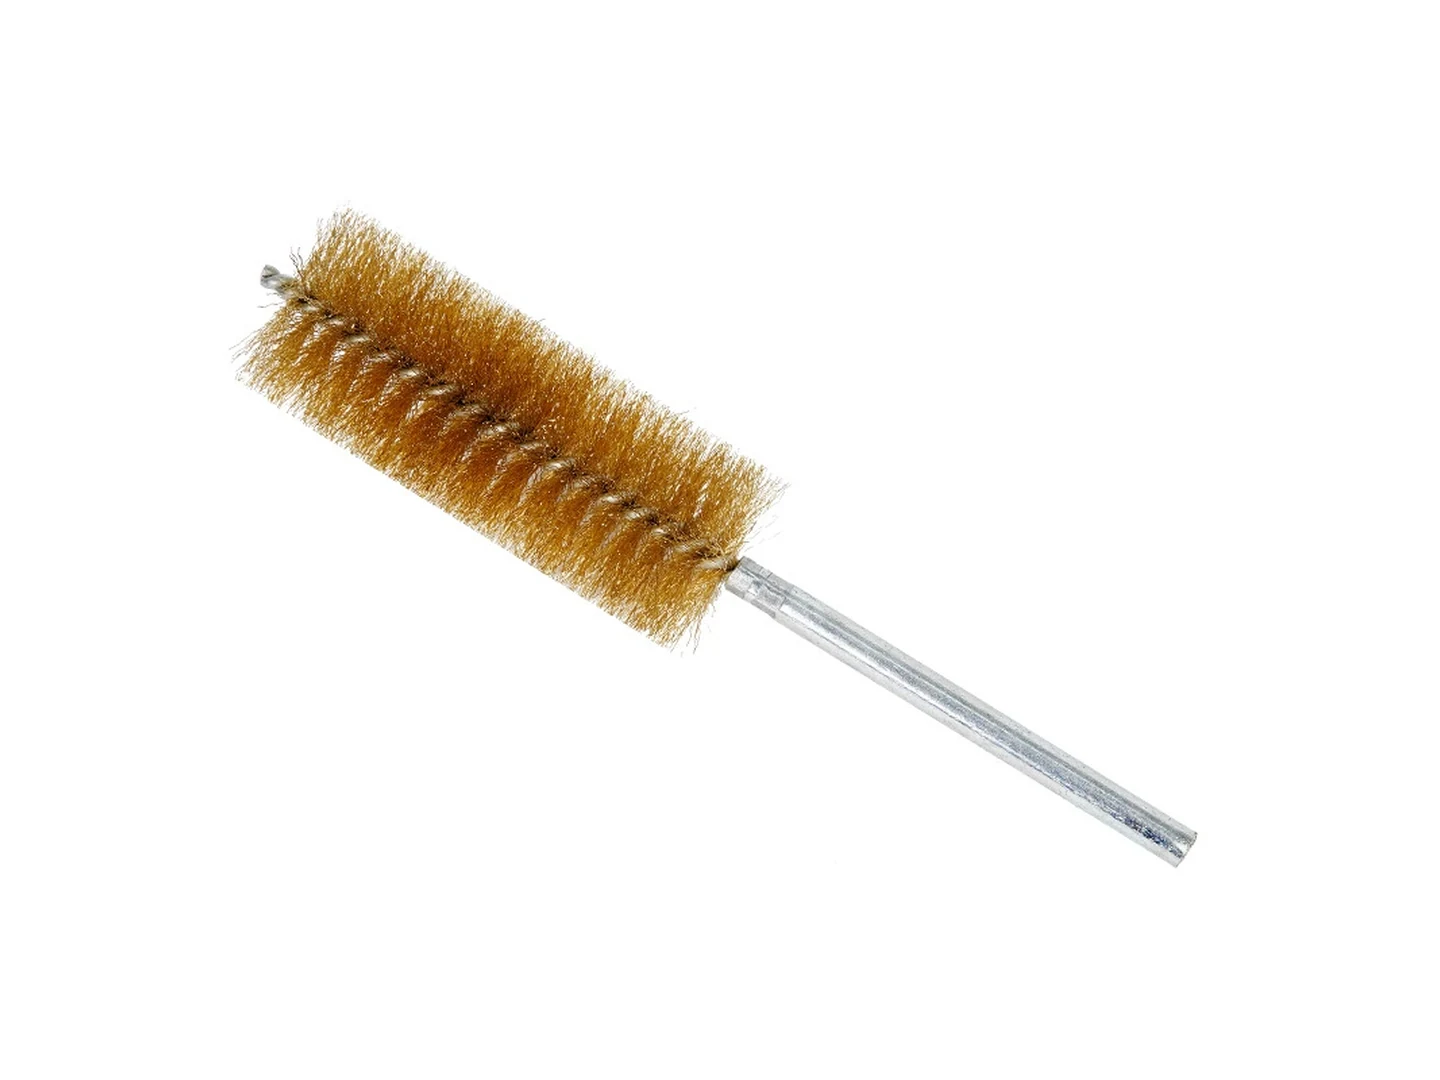
Brass Safety Brush
Manual non-sparking brass safety brush removes rust, scale, paint and corrosion from valves, flanges, threads and tools in ignition-risk environments.
Compare the specificationCustom Manufacturing RFQ
Describe Your Application
For an accurate quotation, please provide the main dimensions, material preference, working surface, residue, quantity, and a drawing or photo.
We reply to every request within 24 hours, with a quotation or with the questions we need answered first. If the brush can be made on our existing tooling, we make the sample directly. If it needs new tooling, we quote a sample fee and a tooling fee, and the sample fee is credited against the bulk order. Need an NDA first? We sign yours before you send drawings, and the files you send are never shown to other customers.
- MOQ500 pcs for small hand-held brushes, 100 pcs for medium and large ones
- SampleTypically 3–7 days
- ProductionFrom 7 days after sample approval, by size and quantity
- Payment30% deposit and 70% before shipment above US$10,000; smaller orders on agreed terms
Have the old brush? Send a photo on WhatsApp
Drawing or photo optional — it speeds things up, it does not gate the enquiry.
“We need a brush to remove wet residue from a stainless steel conveyor, about 800mm wide. The current brush wears quickly. We can send photos.”
“We sell drinkware and need a cleaning brush to include with the product. Quantity around 5,000 pieces.”