
ApplicationIndustrial & Manufacturing
Metal Acid Pickling & Degreasing Line Brush Use
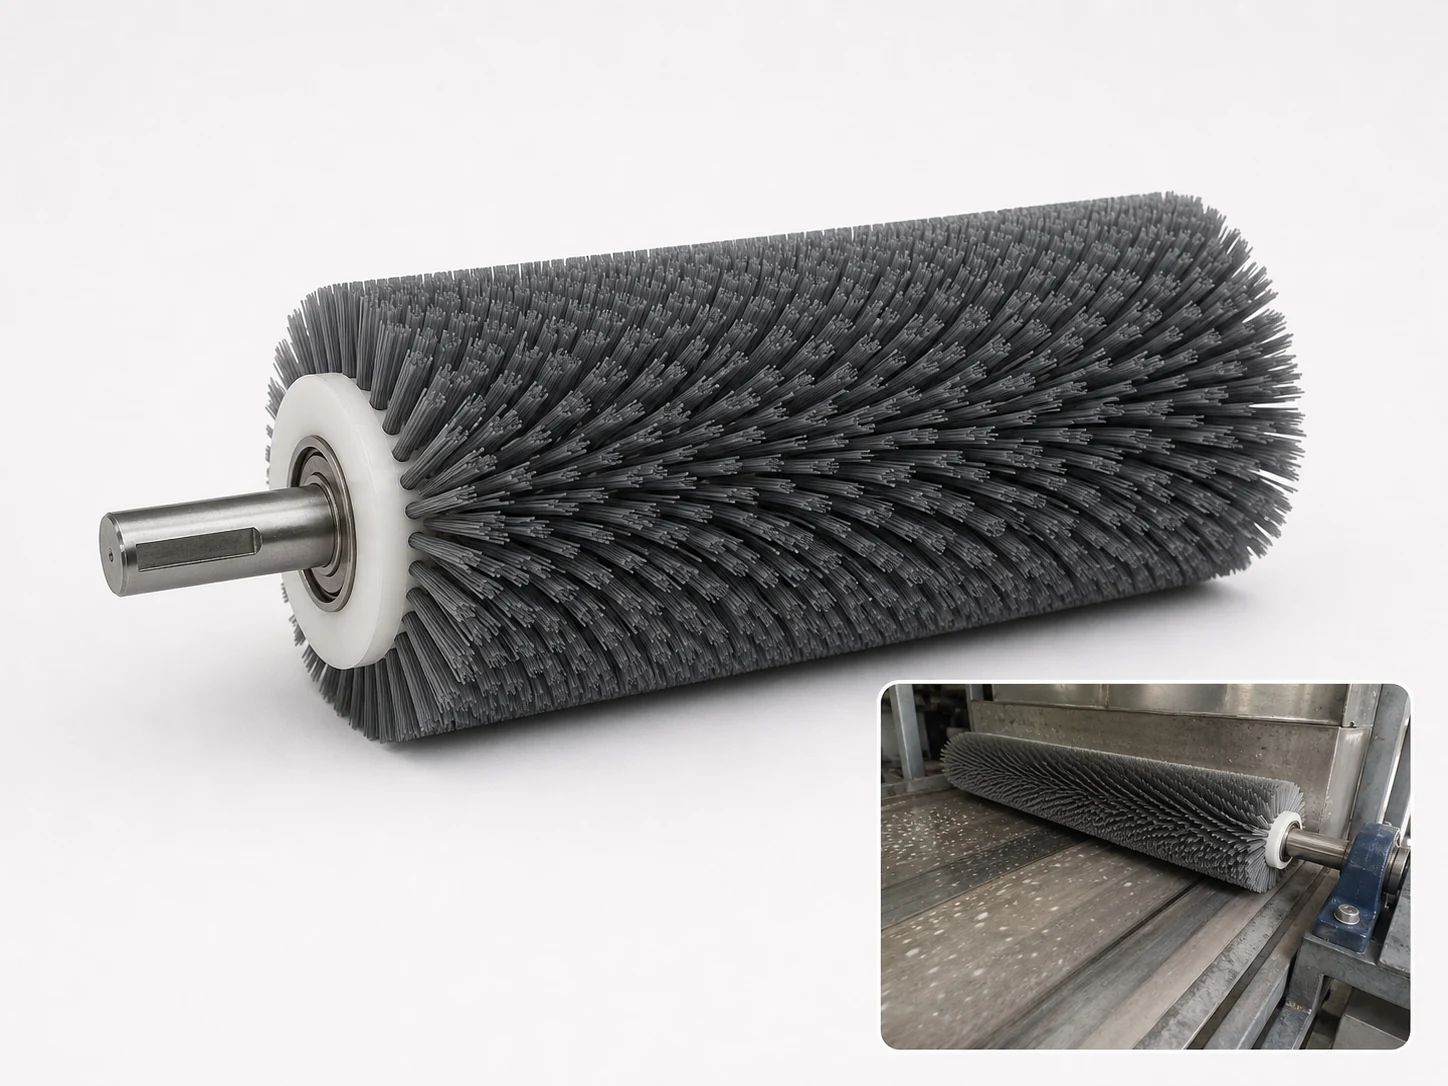
On a pickling or degreasing line the brushes run in the process liquid all shift, so the chemistry and temperature decide the fill before the residue does. Use PP for strong mineral acid up to about 80°C and PBT up to about 120°C. Silicon carbide abrasive nylon scrubs off smut, and strip brushes wipe the strip as it leaves the rinse.
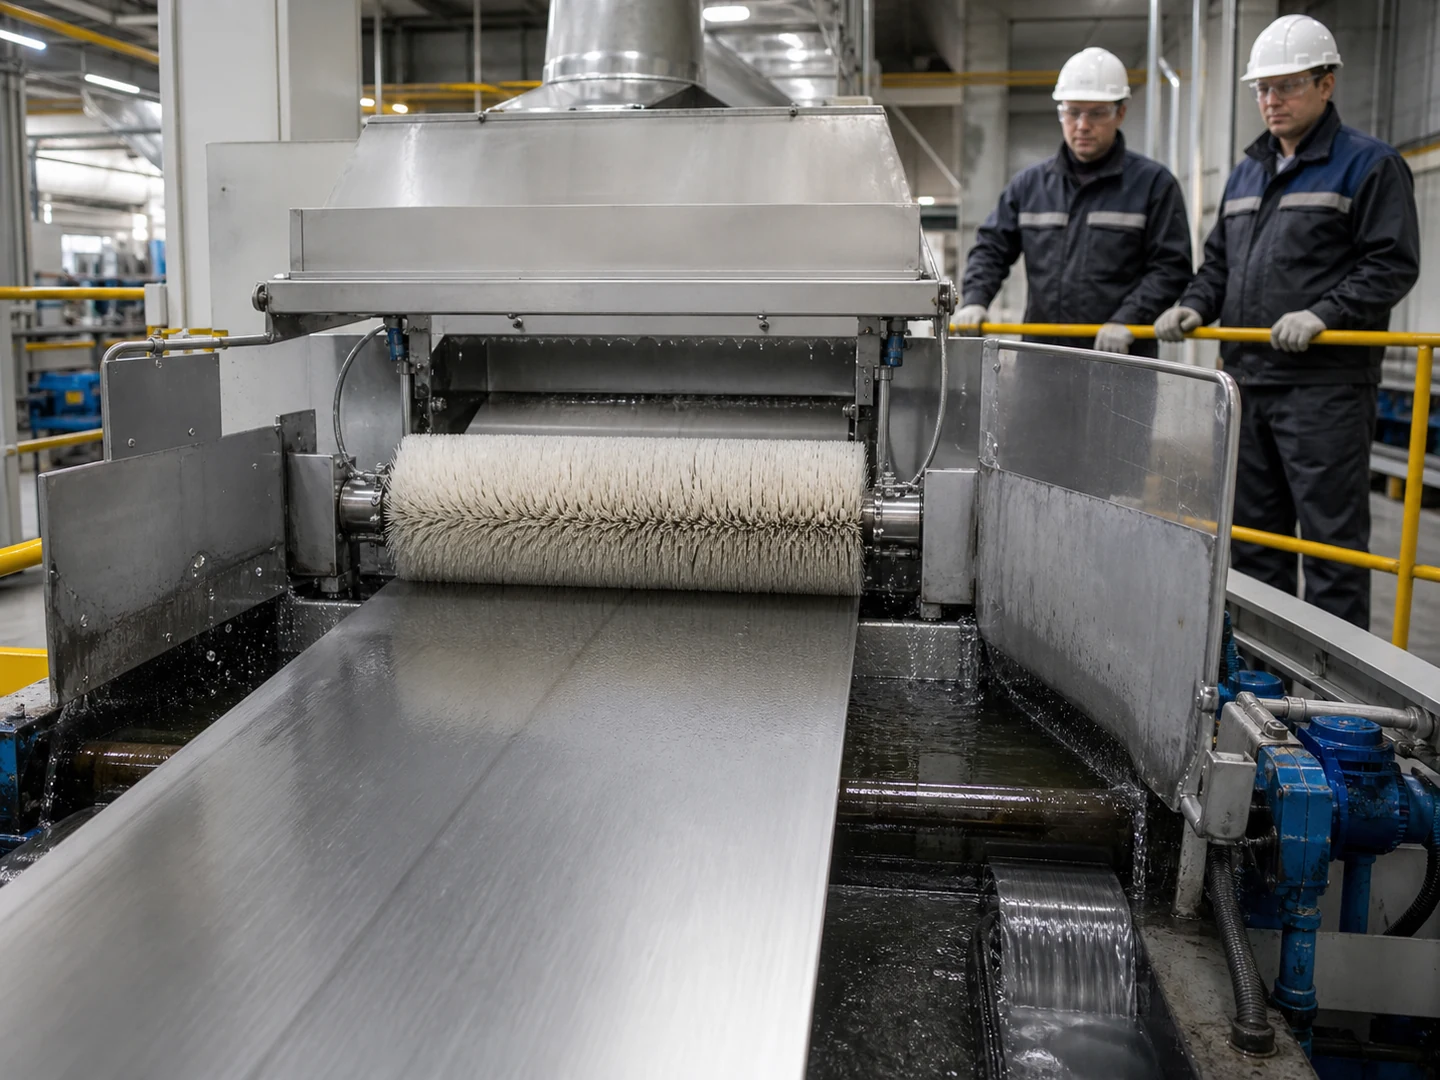
- Cleaning target
- Oxide scale / oil / acid residue / metallic sludge
- Working environment
- Chemical Processing Line / Corrosive Wet Area
- Cleaning method
- Wet Brushing / Immersion-Assisted Cleaning
- Requirements to check
- Chemical-resistance documentation and corrosion-compatible materials; process-specific EHS controls
Catalog brushes made for this job
7 brushes in the catalog
What makes pickling line brushes different?
Acid loosens oxide scale, but it does not take all of it off. Smut, the dark film of fine particles left after pickling, stays on the strip. Sludge collects on the bath rollers and prints back onto the strip as it passes. Brush rolls running against the strip, wet, at line speed, are what remove them.
The brush lives in the bath or in its spray. A fill that is fine in water can soften, swell or break down in hot hydrochloric or sulfuric acid. A steel core can corrode until the roll runs out of true. So the first question for a pickling brush is not the residue; it is the acid, its strength and its temperature.
Ahead of the acid, the degreasing section has the opposite chemistry: hot alkali to take off rolling oil. The brushes there are chosen to that.
Where are brushes used on a pickling line?
| Part or area | Residue type | Cleaning requirement |
|---|---|---|
| Coil Surface Scrubbing | Loosened scale and smut on the strip | Span the strip width and scrub off loosened scale while the strip runs. |
| Oxide Scale Removal | Oxide scale after the acid | Hold an even load on the moving strip so scale comes off across the width. |
| Acid Bath Roller | Metallic sludge on rollers in the bath | Fill and core that resist the acid while clearing sludge from the bath rollers. |
| Degreasing Line Brushing | Rolling oil and fines before pickling | Remove rolling oil and fines ahead of the acid with alkali-resistant fill. |
| Strip Wiping and Rinsing | Acid and rinse water carried on the strip | Wipe acid and rinse water off the strip as it leaves the bath. |
Sizes from the pickling line brushes we make:
| Parameter | Typical range |
|---|---|
| Roller outside diameter | 100–500 mm |
| Working face length | Strip width plus edge allowance, from the line drawing |
| Trim length | 40–120 mm |
| Synthetic filament diameter | 0.20–1.50 mm |
| Stainless wire diameter | 0.20–0.45 mm |
| Continuous service temperature | PP about 80°C, PA612 about 100°C, PBT about 120°C |
Which brush suits each position on the line?
| Cleaning target | Recommended brush type | Why it fits |
|---|---|---|
| Coil Surface Scrubbing | Roller and Conveyor Brushes | The strip runs continuously through the line, so a roller brush spanning its full width scrubs loosened scale and smut off the face as it passes. |
| Oxide Scale Removal | Scale the acid has loosened still has to be worked off under load, so a roller brush set against the moving strip takes it off evenly across the width rather than one patch at a time. | |
| Acid Bath Roller | A bath roller picks up sludge and prints it back onto the strip, so a roller brush riding on it keeps that transfer surface clean while the line runs. | |
| Degreasing Line Brushing | A degreasing line runs continuously, so a full-width roller brush turning against the strip puts the same contact band on every meter instead of leaving the work to dwell time alone. | |
| Strip Wiping and Rinsing | Strip Seal Brushes | After the rinse the strip carries a liquid film that has to be broken across the full width in one continuous line of contact, so a fixed strip brush set across the pass does it without another driven shaft. |
Scrubber rolls usually run in pairs, one above and one below the strip, often against a backup roll. A spiral fill pushes loosened smut and liquid toward the strip edges.
Cores are coated steel, 304 or 316 stainless, or polymer, chosen so the core lasts as long as the fill in that bath.
Which fill survives which bath?
| If the condition is… | Filament to start with | Why |
|---|---|---|
| Strong mineral acid, up to about 80°C | Polypropylene PP | Resists hydrochloric and sulfuric acid; the standard for pickling duty |
| Smut scrubbing after the acid | Silicon Carbide Abrasive Nylon | The grit cuts smut and leftover scale off the strip |
| Hotter, stiffer duty where nylon is approved | PA612 Nylon | About 100°C; use only after the chemistry has been reviewed |
| Mechanical descaling on stainless lines | AISI 316 Stainless Steel Wire | Takes scale off stainless without leaving carbon steel |
| Alkaline degreasing ahead of the acid | Nylon PA | Good in hot alkali; not for concentrated acid |
Concentrated hydrochloric and sulfuric acid attack nylon. Send the acid, its concentration and temperature with the enquiry, and the fill is chosen to them.
How should pickling line brushes be run?
- Set engagement evenly across the width, from a light wipe to an active scrub as the duty needs.
- Re-set the engagement as the fill wears.
- Inspect cores and journals for corrosion at every brush change.
- Keep spare rolls dry and out of acid mist.
- Follow the line’s lockout and chemical safety procedures for every change.
What do we need to quote pickling line brushes?
- The line drawing: strip width, roll position, diameter and shaft.
- The acid or alkali, its concentration and temperature.
- Strip material and the residue: smut, scale, sludge or oil.
- Line speed and whether the roll is driven or idling.
- Quantity per design: 100 pieces for rolls.
When will brushing not finish the job?
Heavy hot-rolled scale is broken first by a scale breaker or shot blasting, and the acid does the rest. A strip that keeps coming out with smut may need a change in acid strength, temperature or line speed. Brushes remove what the acid has loosened.
What mistakes shorten pickling brush life?
- Running nylon in concentrated hydrochloric or sulfuric acid.
- Running PP above its temperature limit, where it softens.
- Using an uncoated carbon steel core in the bath.
- Setting the rolls so hard that the fill bends over and stops scrubbing.
Questions buyers ask about Metal Acid Pickling & Degreasing Line Brush Use
Which brush fill resists hydrochloric or sulfuric acid?
Polypropylene, the standard for pickling duty up to about 80°C, and PBT for hotter duty up to about 120°C. Concentrated hydrochloric and sulfuric acid attack nylon.
How is smut removed from strip after pickling?
With scrubber rolls of silicon carbide abrasive nylon, usually in pairs above and below the strip, running wet against it before the rinse.
Continue Exploring
Recommended Reading & Related Brush Resources
Metal Acid Pickling Brush Roller
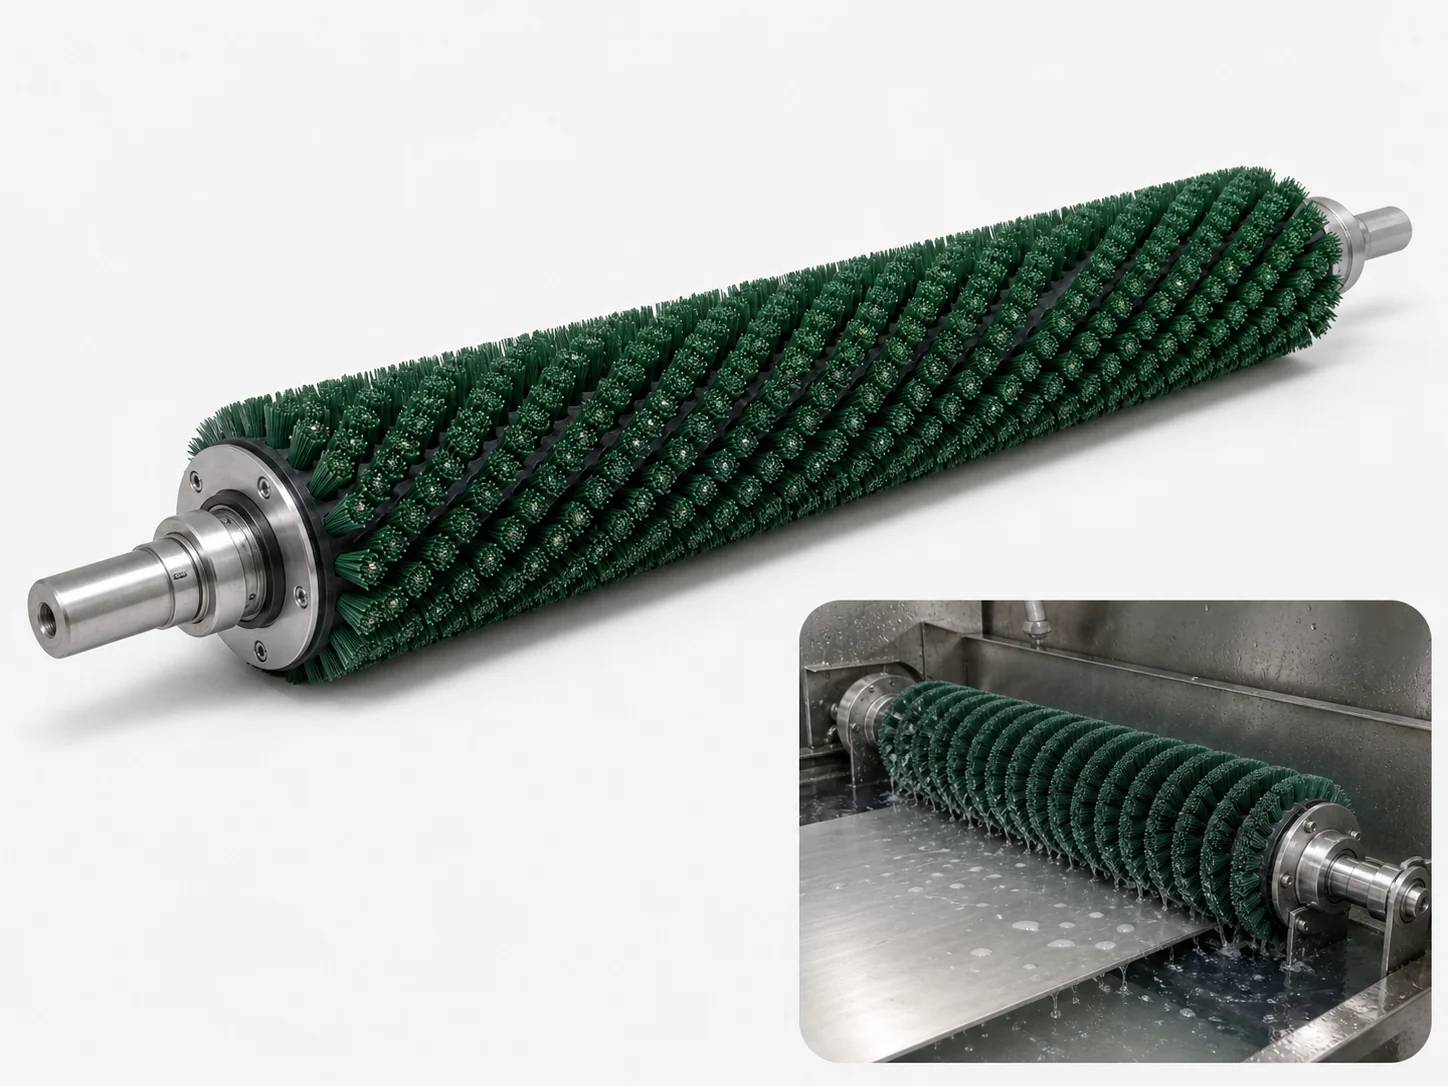
Custom acid pickling brush roller for steel strip and line-roll cleaning. PP, PBT, SiC nylon or 316 wire fill; 100–500 mm OD.
See the specification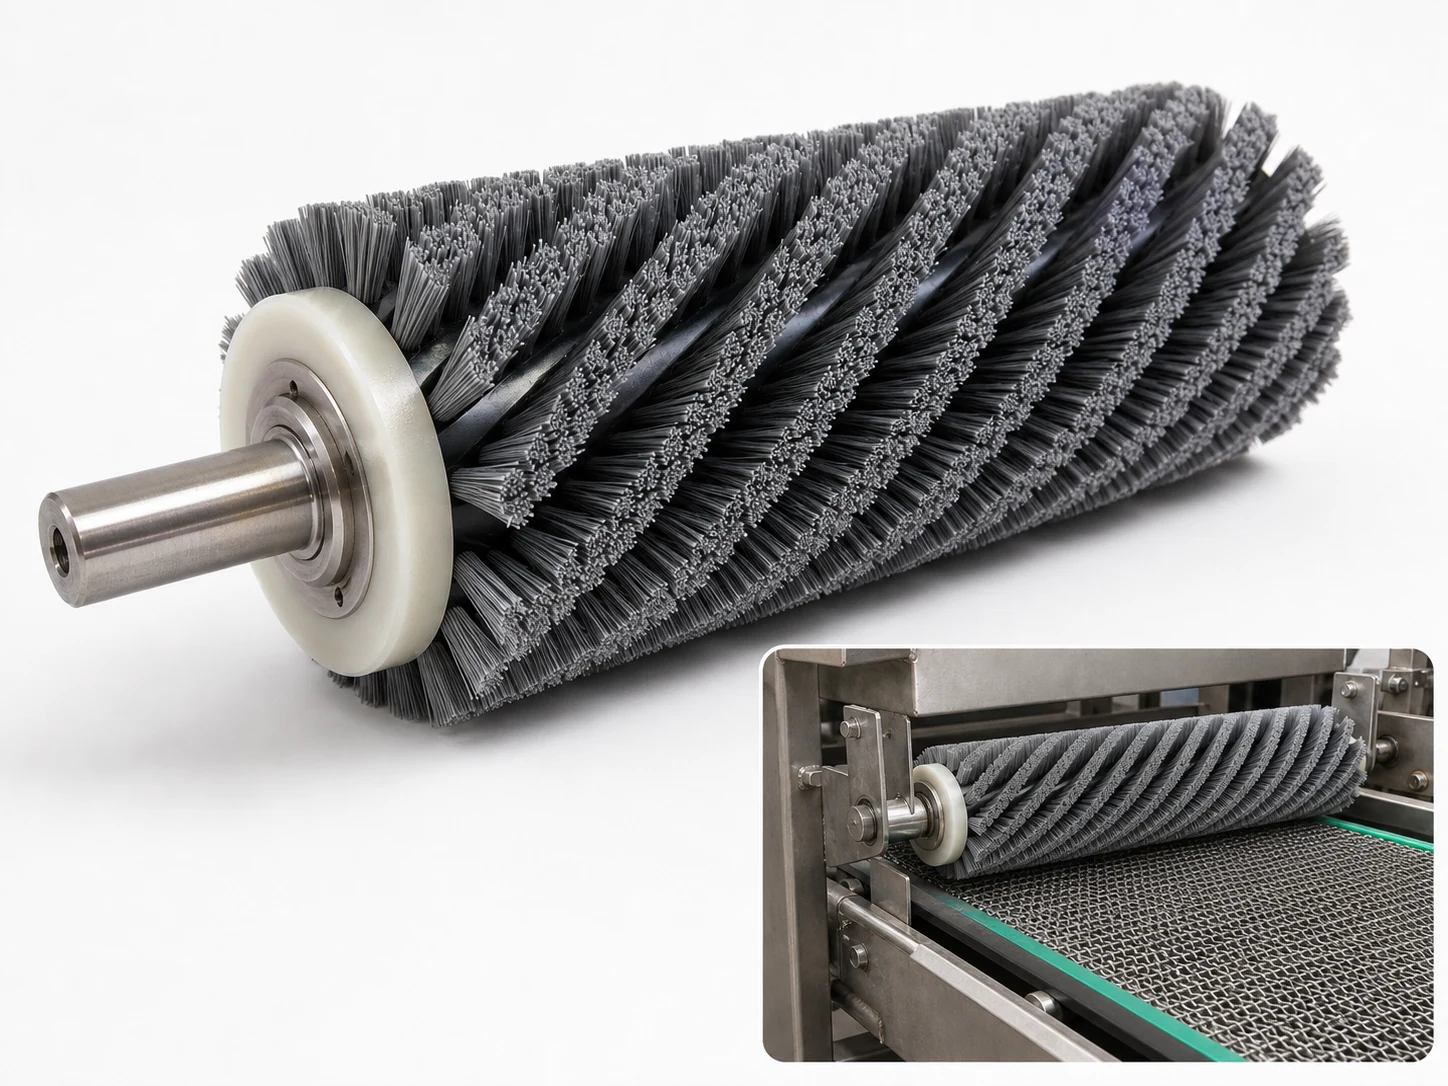
Plating Line Brush Roller
Plating line brush roller for oxide, salt, and sludge removal in pickling and rinse sections. PP and PBT acid-resistant fill, built to your line drawing.
See the specification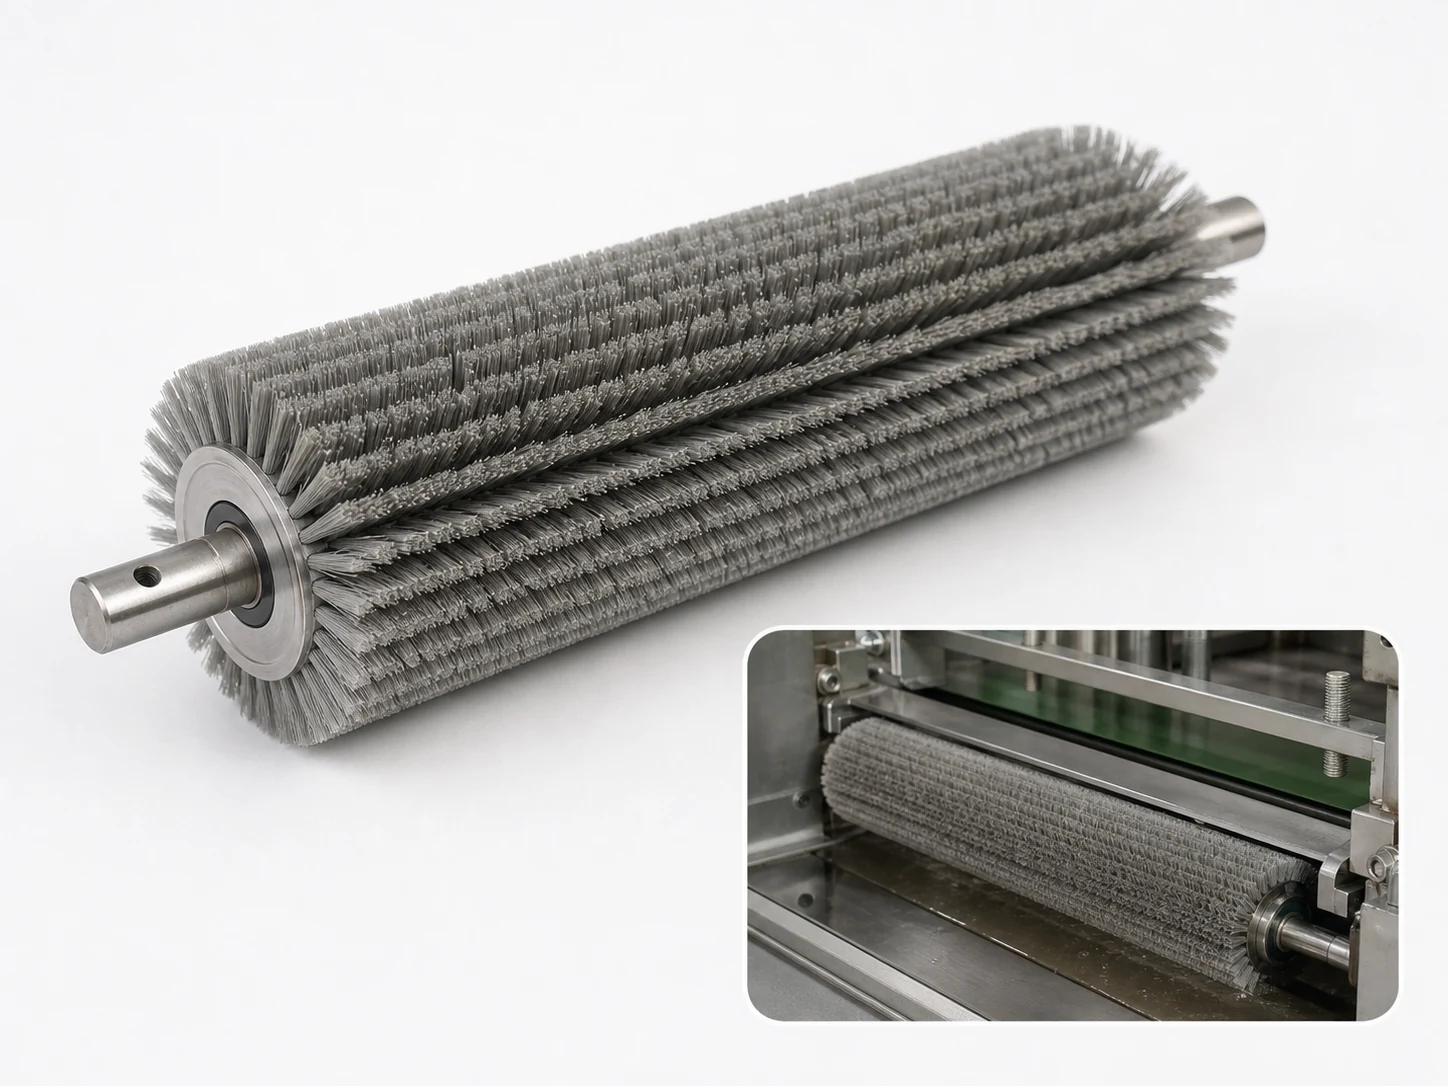
Passivation Line Brush
Acid-resistant roller or strip spanning the strip width, lifting oxide smut and acid salts after the bath so the rinse and dry sections work clean.
See the specification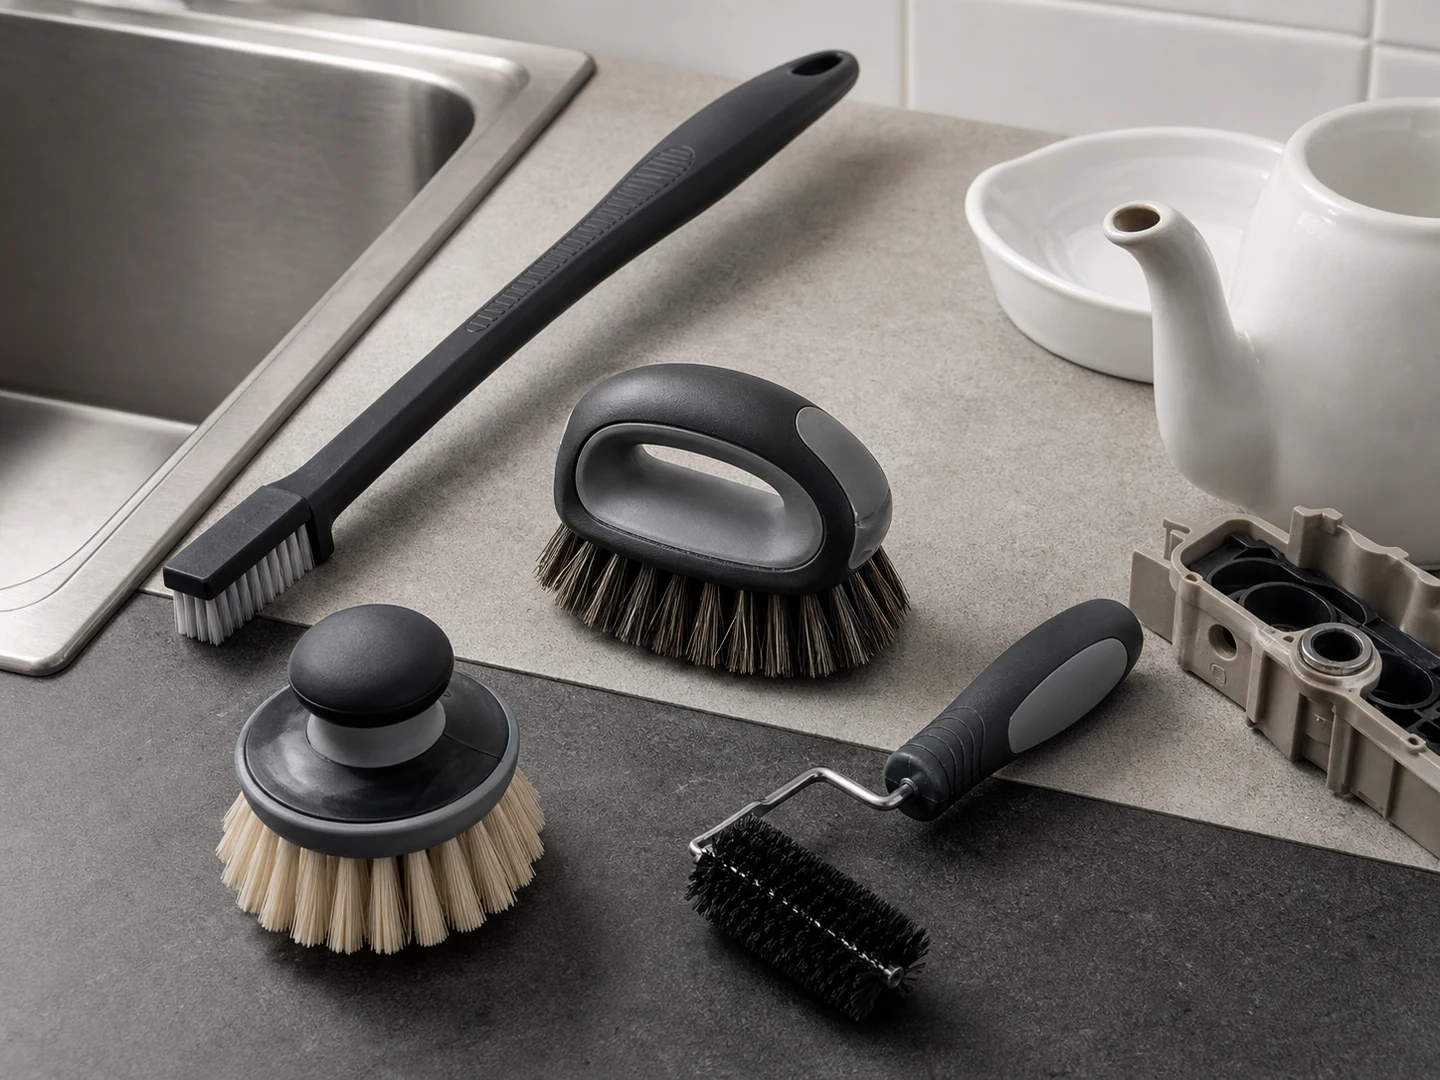
Custom Handheld Detail Brushes
A handheld detail brush puts the operator's hand pressure into a small place: a seam, a grout line, a vent, a connector, a mold vent or a grinder chute.
See how this type is built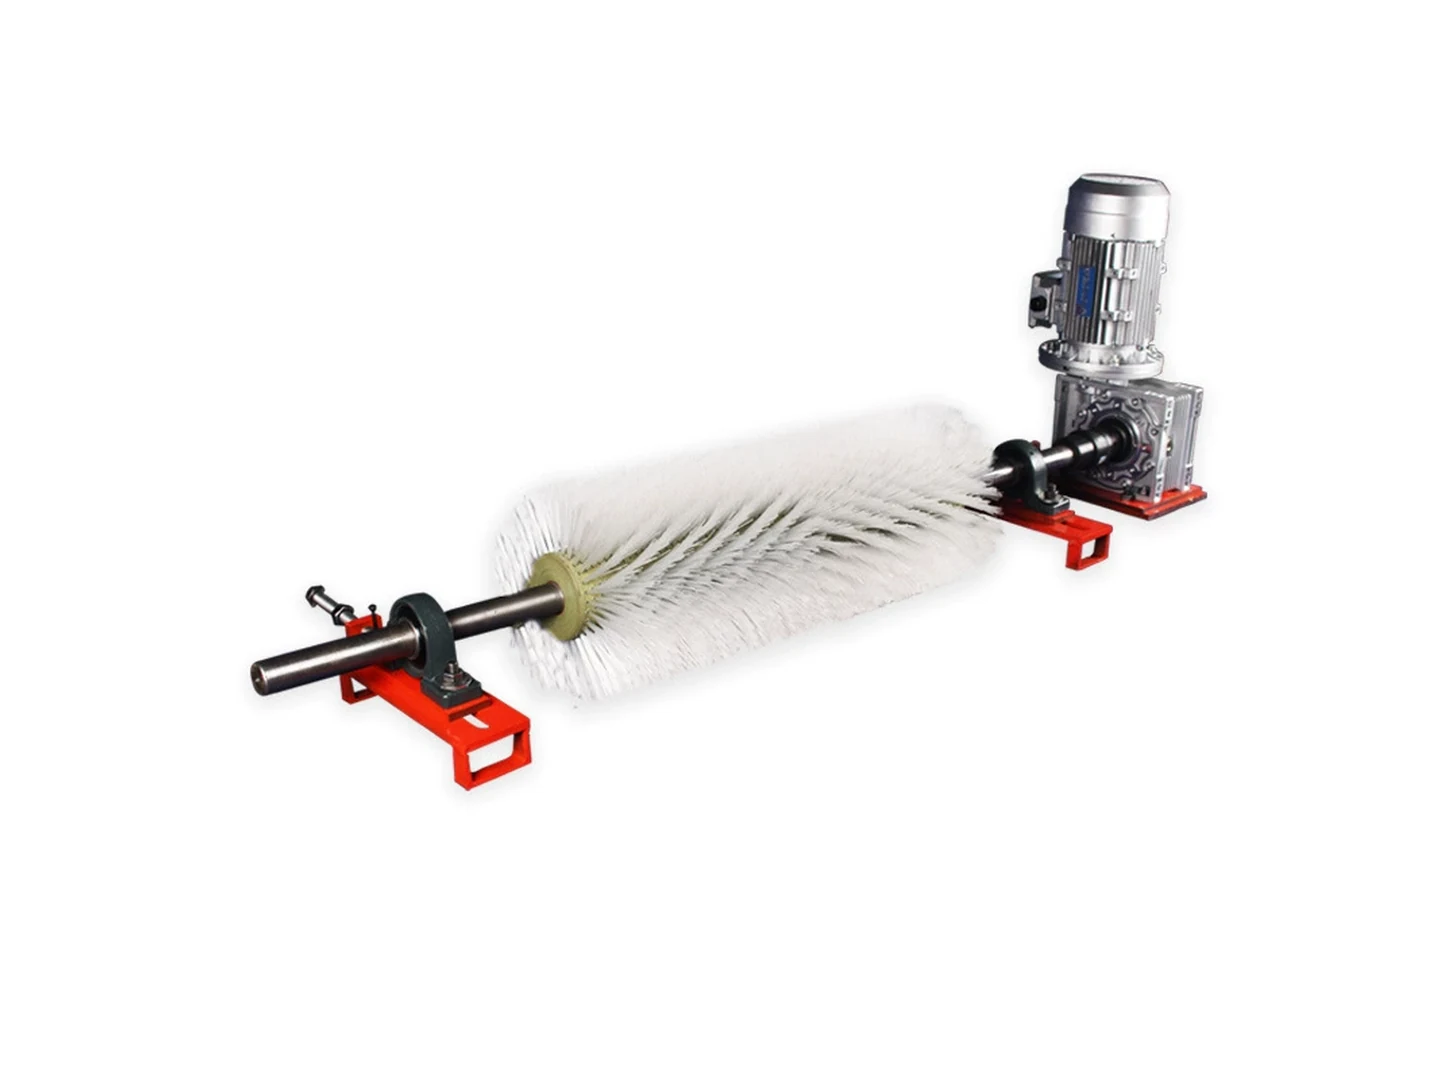
Custom Roller and Conveyor Brushes
A roller brush turns on its own axis and holds an even line of contact across the full width of a belt, sheet, screen or moving product.
See how this type is built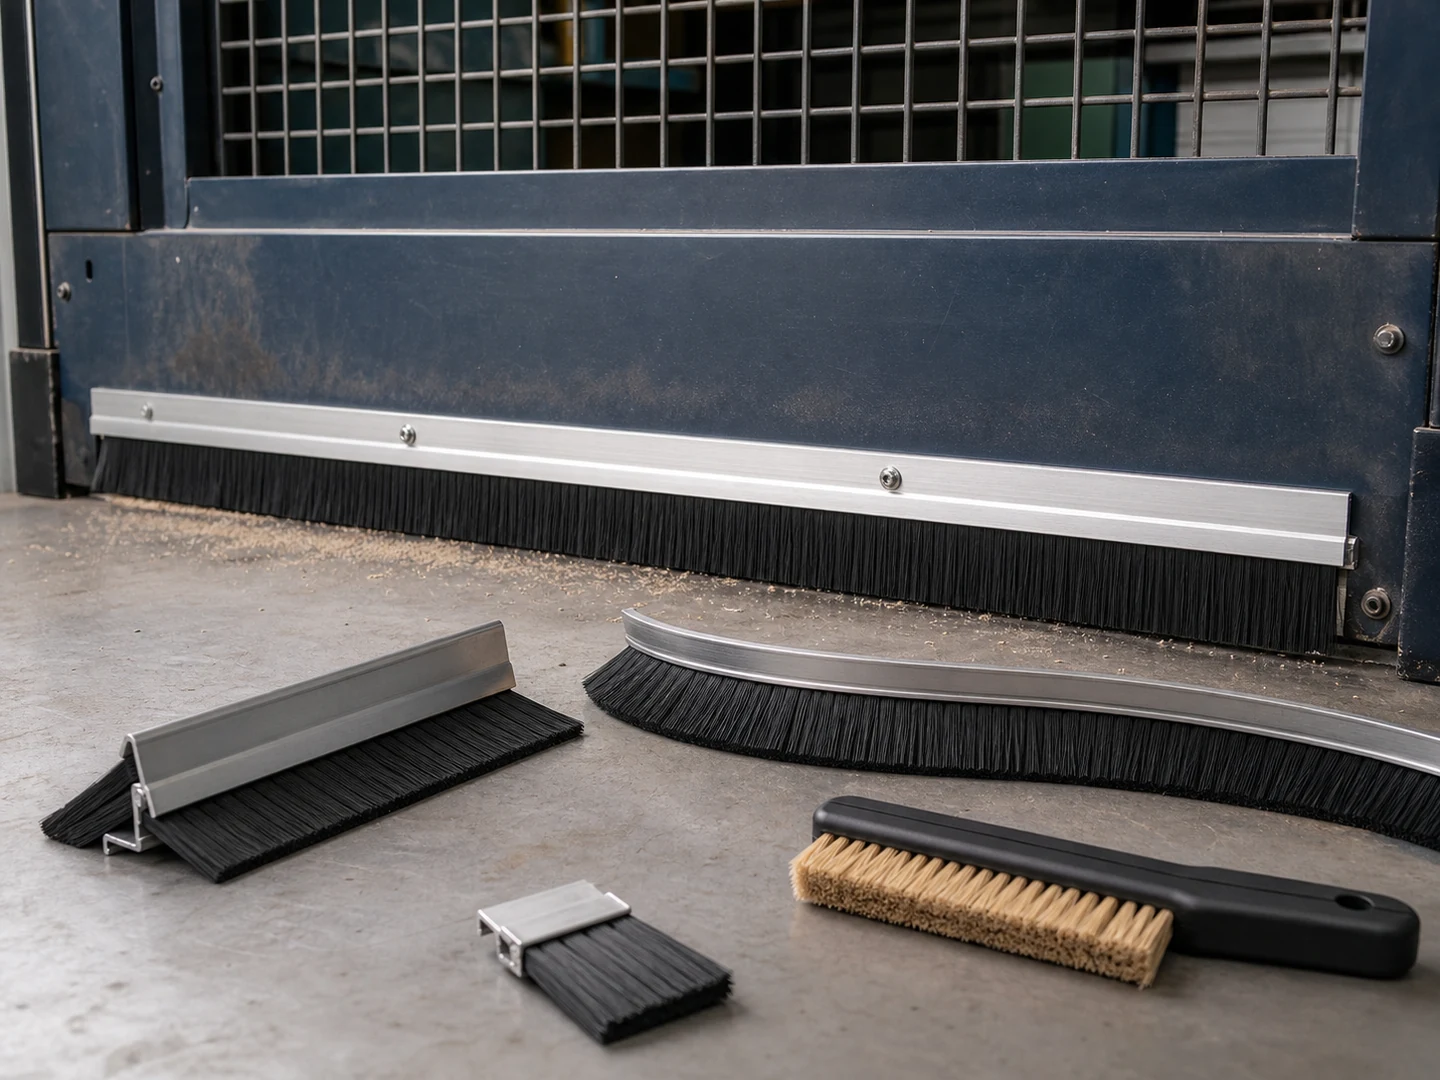
Custom Strip Seal Brushes
A strip brush is a continuous line of fill held in a channel or backing.
See how this type is built
Nylon PA
Nylon is the default brush filament: tough, springy and long-wearing, in a stiffness range from soft detail fill to coarse scrubbing fill.
Compare this material
Polypropylene PP
Polypropylene (PP) bristles absorb almost no water, so a PP brush scrubs as firmly wet as it does dry and stands up to most acids, alkalis and detergents.
Compare this materialCustom Manufacturing RFQ
Discuss This Application
Share the working surface, residue, dimensions, material direction, interface, quantity and drawing or sample photo.
We reply to every request within 24 hours, with a quotation or with the questions we need answered first. If the brush can be made on our existing tooling, we make the sample directly. If it needs new tooling, we quote a sample fee and a tooling fee, and the sample fee is credited against the bulk order. Need an NDA first? We sign yours before you send drawings, and the files you send are never shown to other customers.
- MOQ500 pcs for small hand-held brushes, 100 pcs for medium and large ones
- SampleTypically 3–7 days
- ProductionFrom 7 days after sample approval, by size and quantity
- Payment30% deposit and 70% before shipment above US$10,000; smaller orders on agreed terms
“We need a brush to remove wet residue from a stainless steel conveyor, about 800mm wide. The current brush wears quickly. We can send photos.”
“We sell drinkware and need a cleaning brush to include with the product. Quantity around 5,000 pieces.”