
Coolant Tank Cleaning Brush
OEM / ODM custom manufacturing · made to order
Long-reach coolant tank cleaning brush with nylon PA or polypropylene fill for sludge, fines, biofilm, and coolant residue in sumps and reservoirs.
- Brush type
- Custom Handheld Detail Brushes
- Material
- Polypropylene PPNylon PA
- Working length
- 80–250 mm along the scrub direction, set by available stroke space between baffles
- Overall length
- 200–400 mm standard; extended reach handles available for deeper sumps
- Application
- Industrial Machine CleaningCNC Machine Chip CleaningMetal Acid Pickling & Degreasing Line Brush Use
- MOQ
- 100 pcs
- Lead time
- Within 7 days (up to 100 pcs)
- Sample
- Typically 3–7 days
What can this brush do for you?
Reaches the back wall and under baffles from the cleanout opening
Most coolant tanks are accessible through a narrow cover or cleanout, not through a wide-open top. A head width matched to that opening, combined with an extended or angled handle, lets the operator scrub the far wall, floor-to-wall seams, and the shadow zone under baffle plates without removing internal hardware. The result is a complete cleaning pass from a single access point instead of a partial one plus disassembly.
Keeps its fill stiff and intact in wet, alkaline coolant chemistry
Polypropylene and nylon PA fill both tolerate continuous exposure to water-miscible coolants and common alkaline sump cleaners, but they behave differently. PP picks up almost no water, so it does not soften or swell in submerged service. Nylon PA holds more stiffness when wet and resists abrasion from chips and fines. The fill is selected for the actual chemistry, which keeps the brush scrubbing instead of shedding softened or broken filaments into the coolant.
Removes sludge and soft deposits without gouging steel, aluminum, or lined tanks
Nylon and PP filament ends can be left straight-cut for aggressive scrubbing or flagged and feathered for gentler contact on epoxy paints, plastic baffles, and sensor bodies. Because the fill is non-metallic, the brush loosens residue through repeated filament contact rather than grinding. That protects the tank wall while still breaking up the film that holds tramp oil and fines in place.
Works around screens, level sensors, pump suction lines, and chip conveyor returns
Head geometry is not limited to a simple rectangle. A tapered front edge, corner radius, notch, or stepped trim can be built around the hardware inside the tank. The brush then reaches into the tight seats where sludge collects behind brackets and cable conduits — the places a mop, scraper, or straight-backed brush cannot enter.
Does not introduce metal fragments or rust into the coolant system
Non-metallic filament fill and a polymer or stainless backing mean the brush itself cannot shed wire pieces or corrode into the sump. That protects downstream pumps, nozzles, and filters, and avoids a secondary contamination source caused by the cleaning tool itself.
Technical Specifications
Dimensions are project-specific unless stated otherwise. The values below represent the standard working range for machine coolant tank service and the parameters we confirm before production.
| Parameter | Value / Options |
|---|---|
| Brush head width | 100–200 mm, matched to the cleanout opening and tank width |
| Brush head length | 80–250 mm along the scrub direction, set by available stroke space between baffles |
| Trim length | 20–60 mm free bristle length; shorter trim for flat scrubbing, longer trim for contour and hardware |
| Overall length | 200–400 mm standard; extended reach handles available for deeper sumps |
| Fill material | Nylon PA (PA6, PA612) or Polypropylene PP, specified for coolant type and cleaner chemistry |
| Filament diameter | 0.3–0.8 mm; heavier diameters for chip-filled sludge, lighter diameters for lined surfaces and film |
| Head backing | PP, glass-filled PP, or stainless steel plate with drainage slots or holes |
| Handle material | PP, fiberglass, stainless steel, or composite shaft; optional TPE overmolded grip |
| Head profile | Flat rectangular, oval, round, tapered front, notched, or contoured block |
| Head angle | Straight, 15–45° offset, or cranked shaft for under-baffle and wall access |
| Rinse / drainage design | Open-back or slotted backing so loosened sludge releases during rinsing and the head air-dries |
| Working chemistry | Water-miscible coolants, alkaline sump cleaners, light oil, and mild acid solutions; material grade matched to concentration and temperature |
| Brush type | Custom Handheld Detail Brushes |
| How it is driven | Hand-guided |
| Cleaning target | Machine-tool coolant tanks, sumps and reservoirs, after draining |
| Surface or part | Tank floors, walls, corners, baffles and internal fixtures |
| Residue or debris | Settled metal fines, tramp-oil sludge, biofilm and hardened coolant residue |
| Mounting / connection | Threaded Removable / Fixed |
We do not assign the same polymer fill to every coolant tank. The fill, backing, and handle are chosen after reviewing the actual coolant, sump cleaner, operating temperature, and tank surface. That prevents a chemically acceptable brush from failing mechanically, or a mechanically right brush from degrading in the cleaning solution.
Medium brush
100 pcs
Minimum order
Worked with two hands or on a pole: chimney, gutter and pond-filter brushes, discs, cups and tank brushes.
Production lead time, once the specification is confirmed
- Up to 100 pcsWithin 7 days
- 101–5,000 pcsWithin 14 days
- 5,001–50,000 pcsWithin 21 days
- Over 50,000 pcsConfirmed with your quotation
Peak season can extend these times; the shipping date is confirmed in writing with your quotation. Sampling and shipping are quoted separately.
A hand-directed industrial cleaning brush built for the inside of machine tool coolant tanks, sumps, and fluid reservoirs. Its extended reach, chemical-resistant filament fill, and open-back head design let operators loosen settled metal fines, tramp-oil sludge, biofilm, and hardened coolant residue from tank floors, walls, corners, and around baffles without fully dismantling the tank.
What is a Coolant Tank Cleaning Brush?
A Coolant Tank Cleaning Brush is a hand-guided maintenance brush with a filament-filled head and an extended handle, built for scheduled sump cleanouts rather than for in-service coolant polishing. It is used after the coolant has been drained or pumped down, when a wet layer of sludge, tramp oil, biological film, and settled fines remains on the tank floor, walls, baffles, and internal fixtures.
In operation, the operator reaches through the cleanout opening and uses push-pull and short scrub strokes to loosen the adhered layer so it can be flushed, vacuumed, or scooped out. The brush is not a substitute for a chip scraper or vacuum for bulk solids, and it is not designed for turning or powered machine surfaces. It is the contact tool that breaks the bond between the deposit and the tank before the rinse step.
Because coolant chemistry and tank construction vary widely from one machine to another, there is no single universal fill or handle length. The configuration is built around the tank: opening size, internal depth, baffle spacing, residue type, and the coolant and cleaner chemistry the brush will contact.
How do I choose the right one?
Four decisions shape the configuration: access, residue, chemistry, and contact geometry.
Start from the opening, not the tank volume
Measure the cleanout opening or narrowest path the brush must pass through, then set the head width to travel that path. A head that is too wide binds against the opening or baffles. A head that is too narrow scrubs fewer square inches per stroke and slows the maintenance pass. Also check the deepest point the operator needs to reach; that sets handle or shaft length.
Match the fill to the deposit and the surface
Heavy sludge with chips and fines calls for stiffer nylon PA in a thicker diameter and shorter trim. Soft biofilm, tramp-oil film, and lightly adhered deposits can be handled with PP or medium nylon in a longer trim that follows floor unevenness. If the tank is epoxy lined or has plastic baffles, specify flagged or rounded filament tips and lower stiffness to avoid paint damage. If the scale is hard, cemented, or rust-bonded, nylon and PP may be too soft; that kind of deposit usually needs a stainless-steel, brass, or abrasive brush or an acid descaling step before brushing.
Select the polymer for the chemistry, not just the residue
Polypropylene is the safer default for highly alkaline sump cleaners and continuous water immersion because it absorbs almost no moisture. Nylon PA is the better option when the operator needs higher stiffness and abrasion resistance, and it works well in water-miscible coolants and light oils, but it can be affected by strong acids, certain oxidizers, or prolonged high-temperature exposure. Review the coolant, cleaner concentration, and bath temperature before locking the fill.
Adjust trim, angle, and head shape for the contact surface
Flat tank floors use a flat-head, short-trim brush for fastest scrubbing. Walls, under-lip zones, and the area behind baffles benefit from an angled or offset head. Longer trim wraps around pipe brackets and cable conduits; shorter trim transfers more operator pressure into the deposit. A notched or tapered front can be added when a sensor or bracket occupies the natural path of the head.
Match the handle to control, not only reach
Extra length reaches deep, but it also reduces the pressure the operator can apply and can make the brush tiring to control. For long reaches, a D-handle or T-handle improves two-handed control. In wet chemical service, a fiberglass, stainless, or composite shaft with a chemical-resistant grip outlasts untreated wood if wood is used.
When this is not the right brush
Use a wire or abrasive brush only when the deposit is cemented scale, heavy rust, or baked-on residue that nylon and PP cannot break. Use a scraper or vacuum for bulk solids, and use a magnetic pick-up for ferrous chips before brushing. Use powered or rotary brushes only if the tank geometry and access allow controlled machine motion and the operator is protected; most sump cleanups stay with a hand brush for control around sensors and hoses.
Can I customize this brush?
Yes. The coolant tank brush is built around your tank, not from a fixed stock shape. We work from your cleanout dimensions, tank depth and width, baffle spacing, hardware locations, residue description, and coolant or cleaner chemistry. To shorten the review, send a photo or sketch of the tank interior with the major obstructions marked.
We can adjust:
- Head dimensions and geometry — width, length, depth, front taper, corner radius, notches, cutouts, or a multi-surface contour
- Filament system — PP or nylon PA, diameter, trim, stiffness, straight, flagged, or rounded tips, density, and color coding
- Handle and reach — length, straight or angled shaft, D-handle, T-handle, loop grip, TPE overmold, and hanging feature
- Backing design — PP, glass-filled PP, or stainless steel; slotted or drilled for drainage and fast drying
- Head-to-handle connection — fixed for cost efficiency, or threaded/twist-lock for replaceable heads
- Color and marking — custom color for tank or machine identification, pad print, laser marking, or molded part number
- Packaging — bulk case, individual bag, maintenance-kit packing, or project-specific labeling
The key is to define the environment and the contact surface accurately before production so the first sample matches the actual tank, not a generic specification.
Where does this brush work best?
- CNC machine tool coolant tanks and sumps at scheduled cleanout or coolant change, where settled fines and tramp-oil sludge collect on the floor and back corners.
- Grinding machine tanks and chip traps where abrasive swarf, wheel grit, and heavy coolant sediment pack into seams and beneath screens.
- Central coolant systems, transfer tanks, and filtration unit reservoirs where biological slime and floating tramp oil leave wall films above the working fluid line.
- Baffled tanks and partitioned sumps where the brush head must pass a narrow divider gap and still scrub the adjacent compartment.
- Parts washer and wash-down system reservoirs that accumulate chemical deposits and soft sludge on internal walls.
For bulk chip removal, use a scraper, shovel, or vacuum first, then use this brush for the remaining adhered layer and the tight-access zones. The brush is not the right tool for large piles of dry or long stringy chips.
When is a coolant tank cleaning brush worn out rather than just dirty?
Can this brush be used while the coolant tank is still full?
It should not be. The brush is designed for drained or pumped-down tanks. Brushing in a full sump suspends debris and can push sludge toward pump inlets, nozzles, or valves. Drain or transfer the coolant first, remove bulk solids, brush the residual layer, then rinse and recharge the system.
What should the operator check before reaching into a machine tool coolant tank?
Confirm the machine is under lockout or tagout if the operator will enter the enclosure, the coolant pump is off, and the tank is drained to a safe working level. Inspect the brush for loose fill, cracked backing, or a bent shaft before it enters the tank, since a broken filament or handle fragment can become a new contaminant.
How can I avoid carrying bacteria or residue from one machine to another?
Rinse the brush thoroughly after each use with clean water or the same sump cleaner used in the tank, work the root of the filament fill to release trapped sludge, and hang the brush to air dry. For shops with multiple machines and coolant types, use color-coded handles or assign a brush per machine group so a contaminated brush cannot spread biofilm or incompatible chemistry.
Will this brush remove hard water scale and rust from tank walls?
It removes soft scale, dried coolant residue, and loose rust, but it will not grind off cemented mineral scale or heavy rust. If a sharp tool or a fingernail cannot mark the deposit, it is probably too hard for nylon or PP fill. In that case, descale or derust with the appropriate chemical step first and use the brush for the softened layer, or switch to a wire brush if the tank surface allows metal contact.
How do I know if the head angle or trim is right for our baffled tank?
Check the gap between the baffle and any adjacent wall or hardware. If the gap is small and the target surface sits behind the baffle, request a narrower head, shorter trim, or an offset head so the brush can enter without bending the fill permanently. A prototype or first-article brush can be tested in one tank before ordering the full maintenance set.
How long should a coolant tank brush last in scheduled maintenance?
There is no fixed interval; replace it on condition. Replace the brush or the replaceable head when the filament is permanently matted, bent at the root, brittle, or worn down by roughly 30 percent of the original trim, or when the backing shows cracks. A worn brush increases operator effort and leaves more residue behind, so replacement is a consistency issue, not just a cosmetic one.
Guides that go deeper on this
Continue Exploring
Recommended Reading & Related Brush Resources
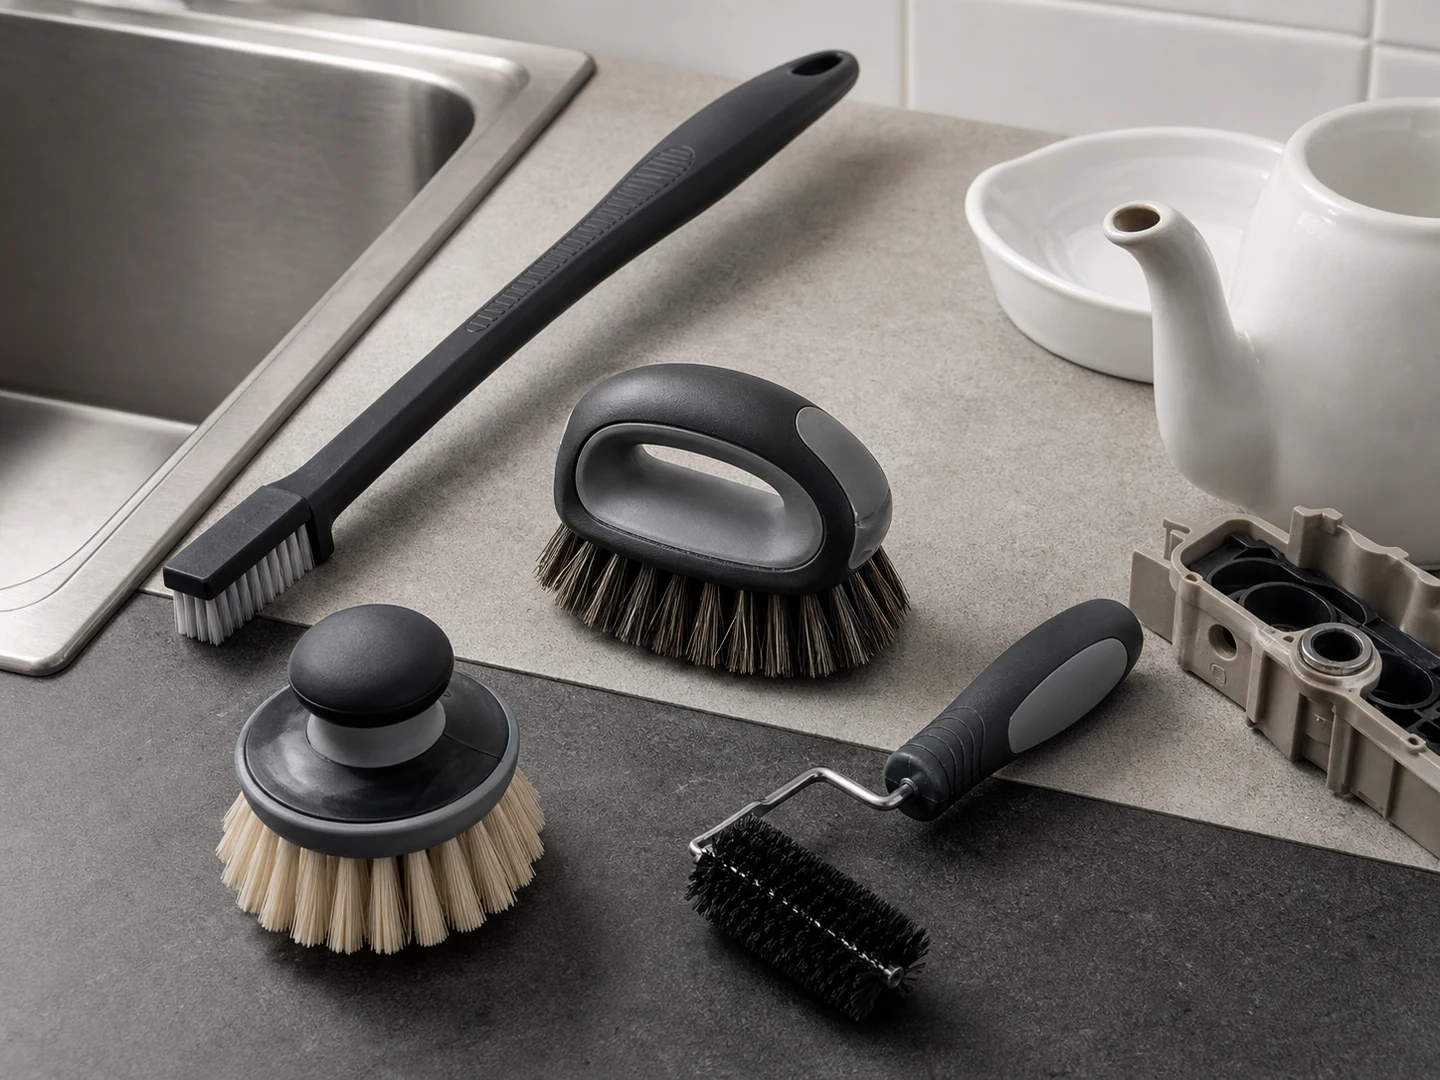
Custom Handheld Detail Brushes
A handheld detail brush puts the operator's hand pressure into a small place: a seam, a grout line, a vent, a connector, a mold vent or a grinder chute.
See how this type is built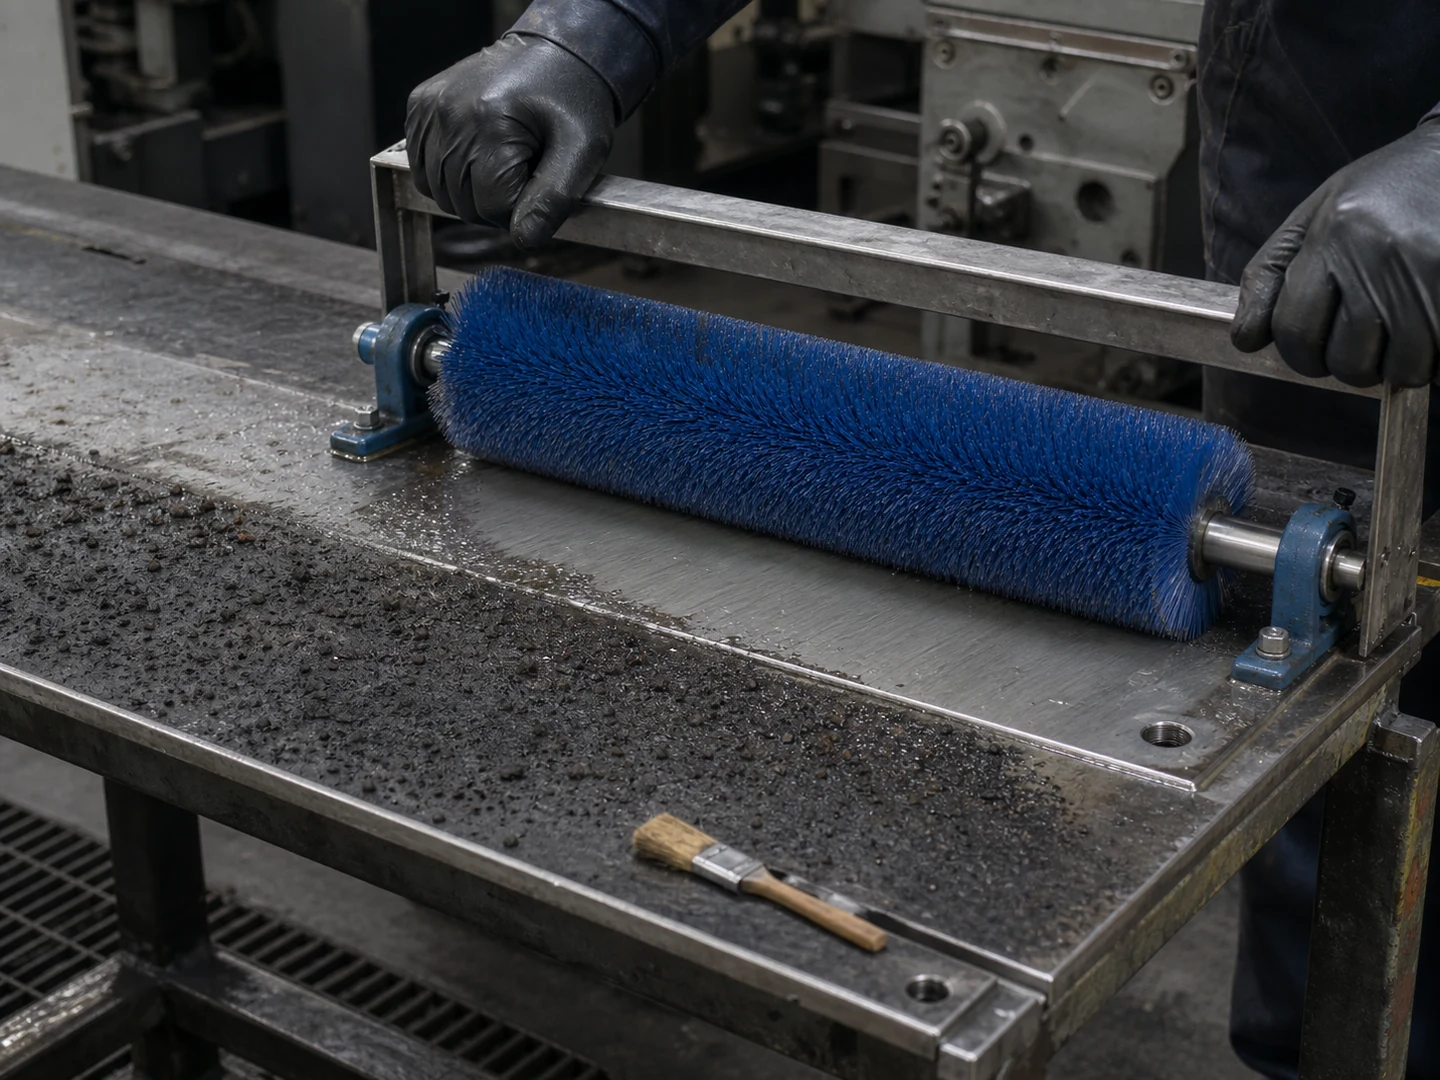
Industrial Machine Cleaning
Machine tools and production equipment are cleaned with brushes that move chips, fines and caked dust into a pan or extraction, never into the air or under a slide.
See the cleaning job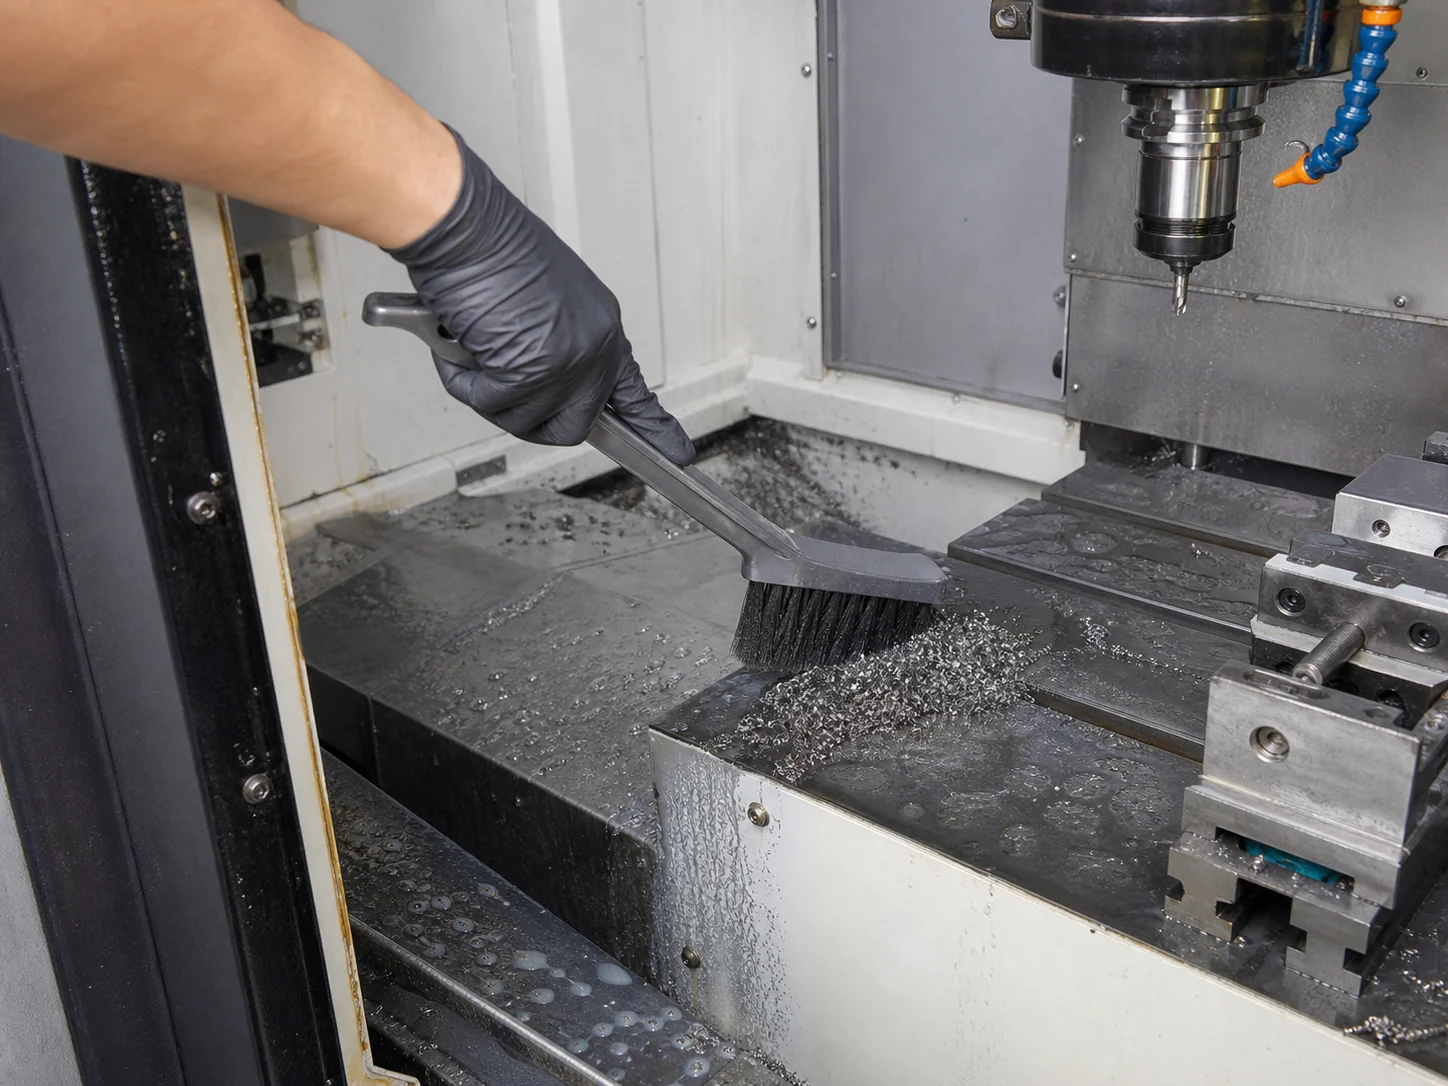
CNC Machine Chip Cleaning
Chips on a CNC machine cost accuracy before they cost cleaning time. One chip on a spindle taper moves the tool.
See the cleaning job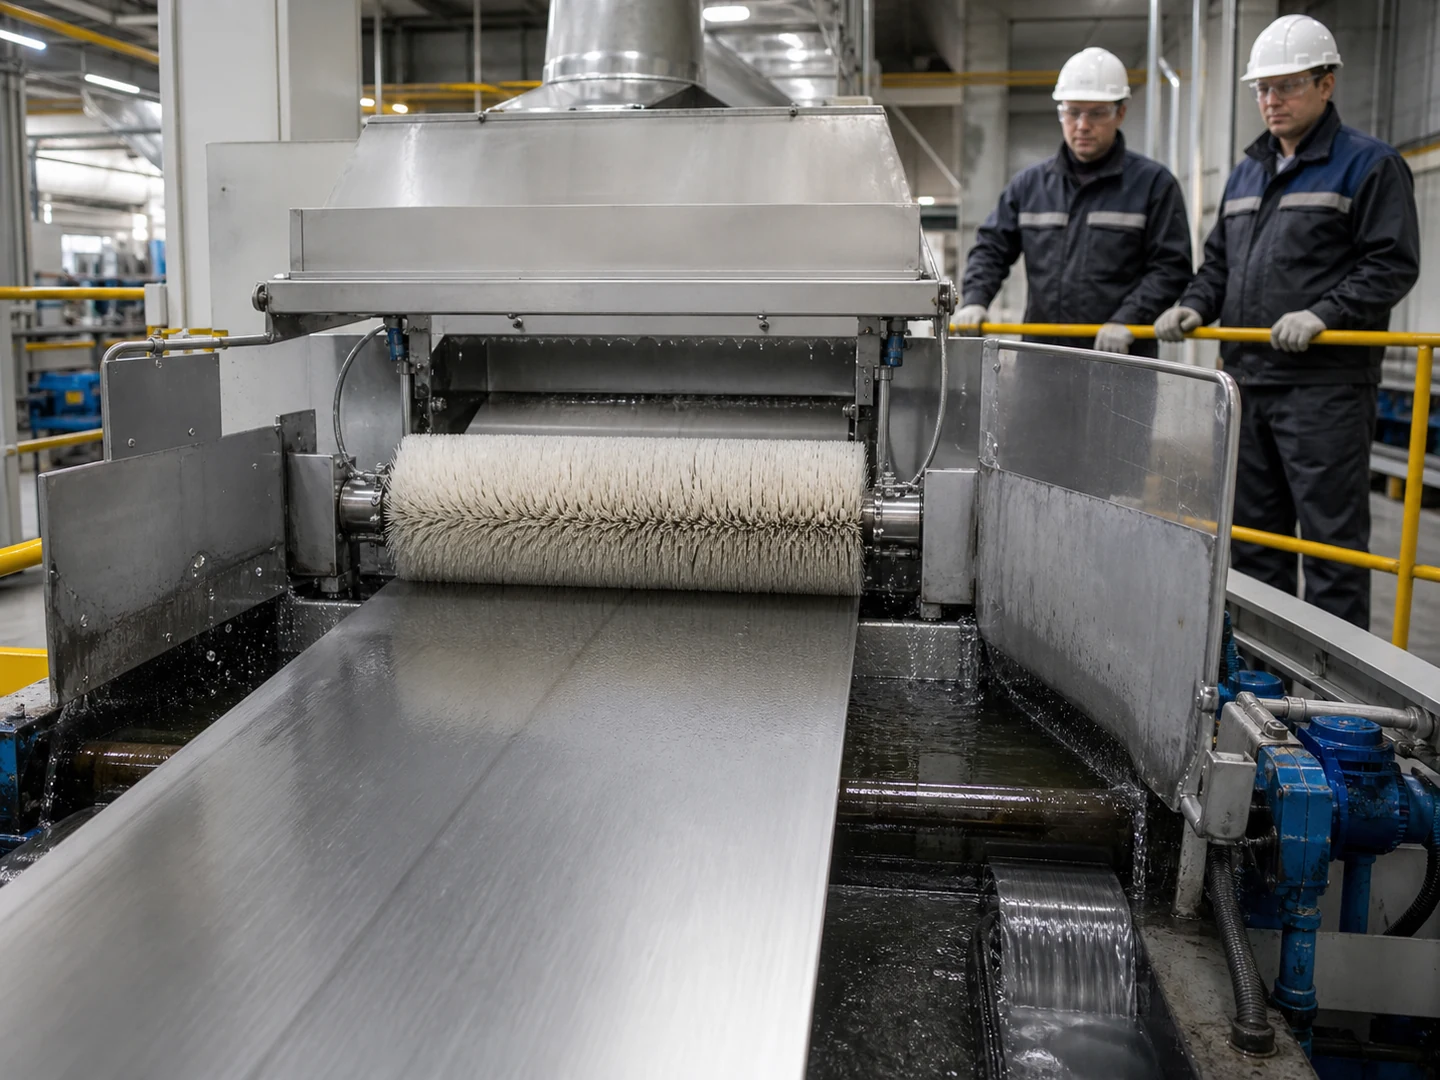
Metal Acid Pickling & Degreasing Line Brush Use
On a pickling or degreasing line the brushes run in the process liquid all shift, so the chemistry and temperature decide the fill before the residue does.
See the cleaning job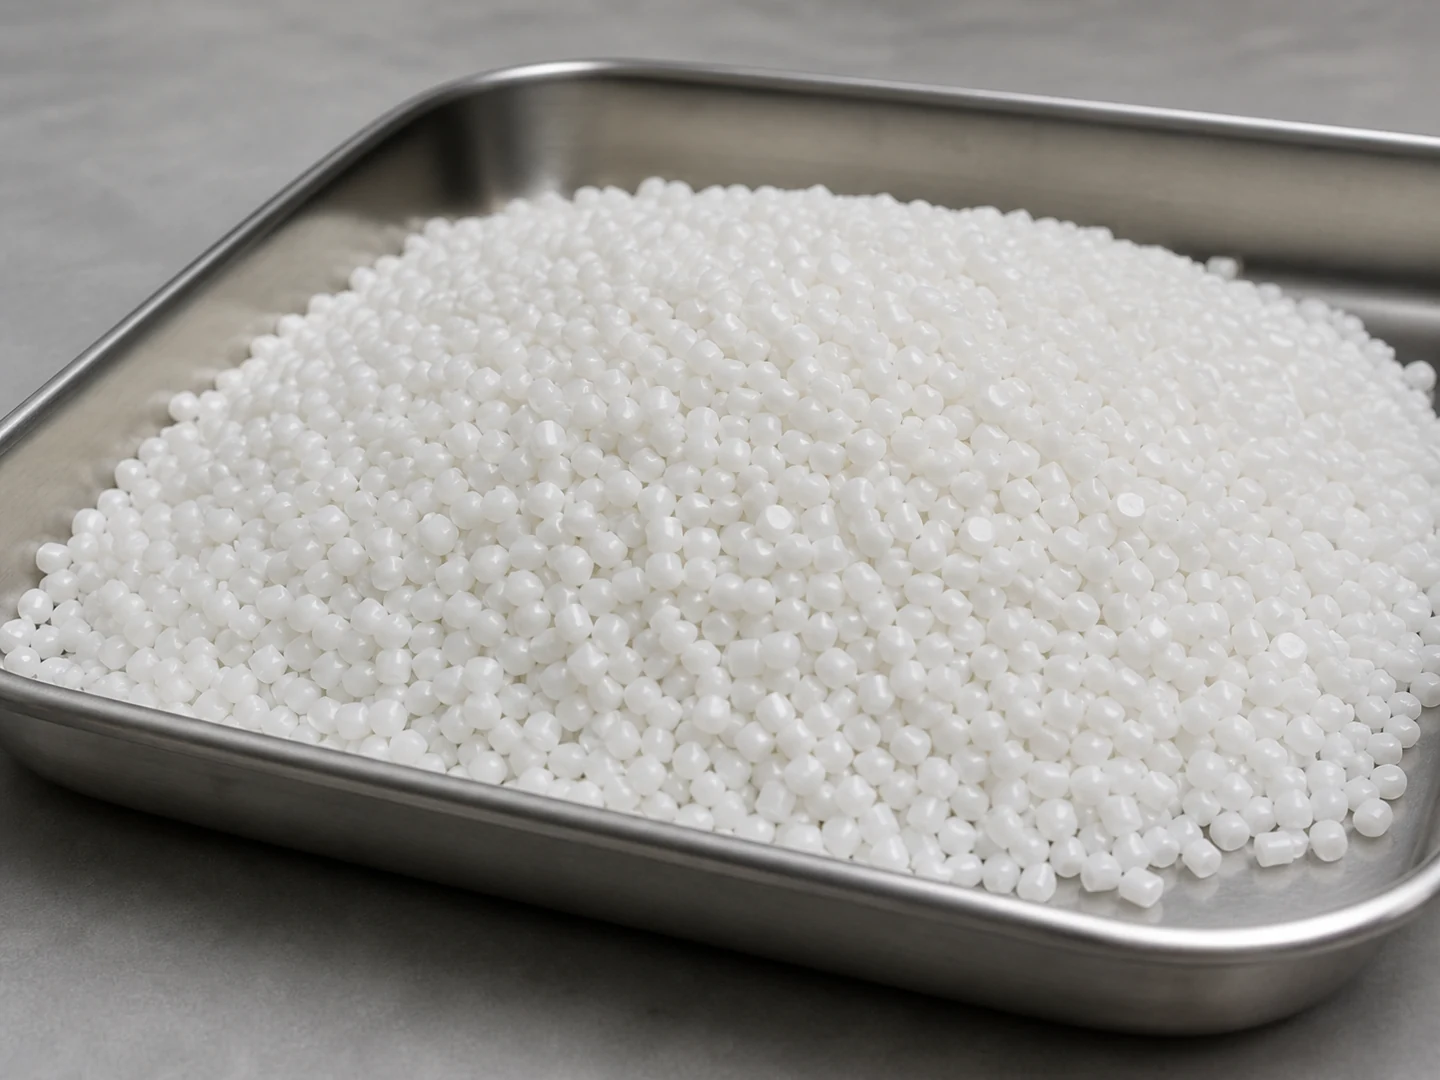
Polypropylene PP
Polypropylene (PP) bristles absorb almost no water, so a PP brush scrubs as firmly wet as it does dry and stands up to most acids, alkalis and detergents.
Compare this material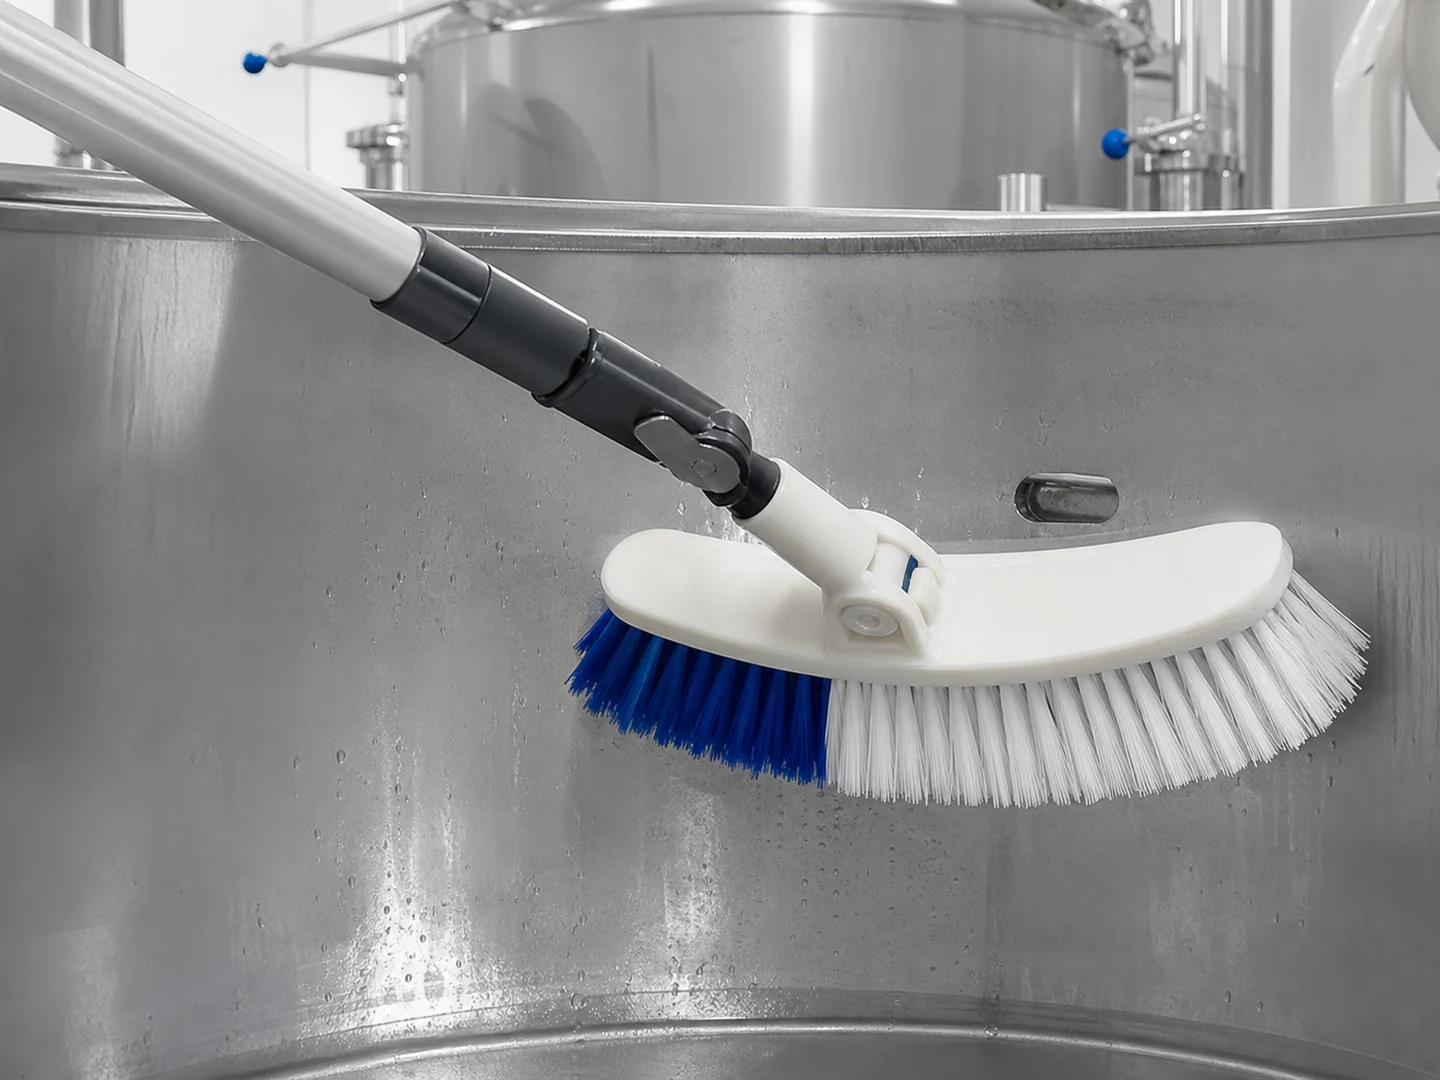
Water Treatment Tank Brush
PP or nylon water treatment tank brush for walls, baffles, drains, and bottom transitions. Broad heads from 100–300 mm with extension-handle mounting.
Compare the specification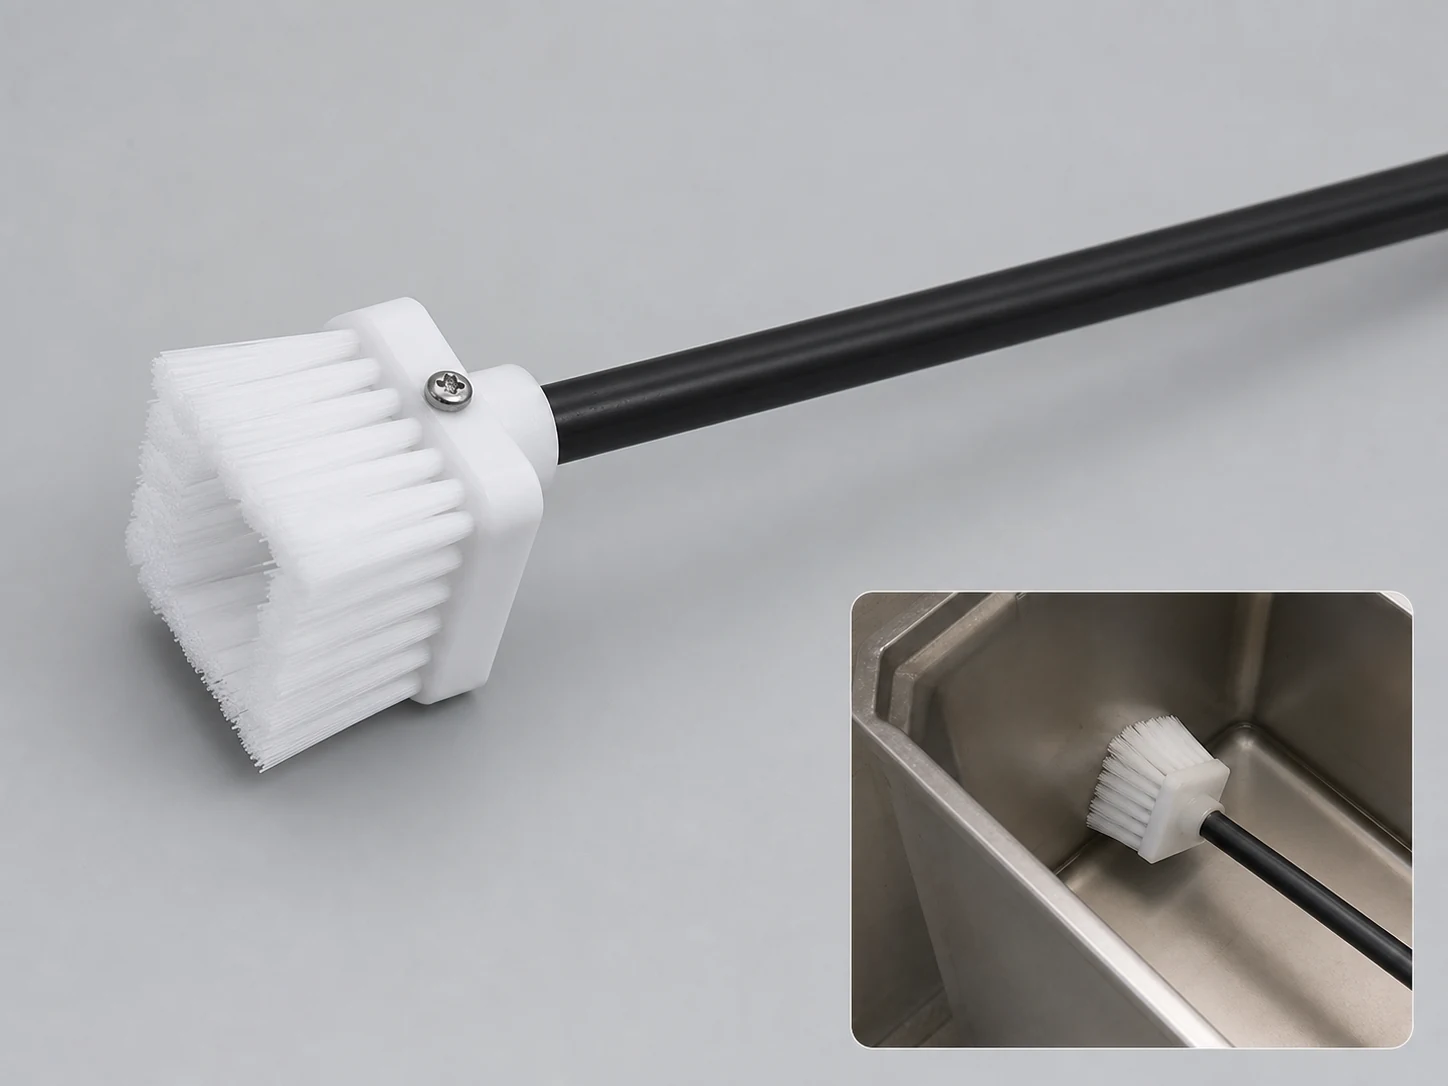
Square Tank Cleaning Brush
Square tank cleaning brush with nylon PA fill for flat walls, 90° corners, weld seams, and drains. Threaded for extension handles.
Compare the specification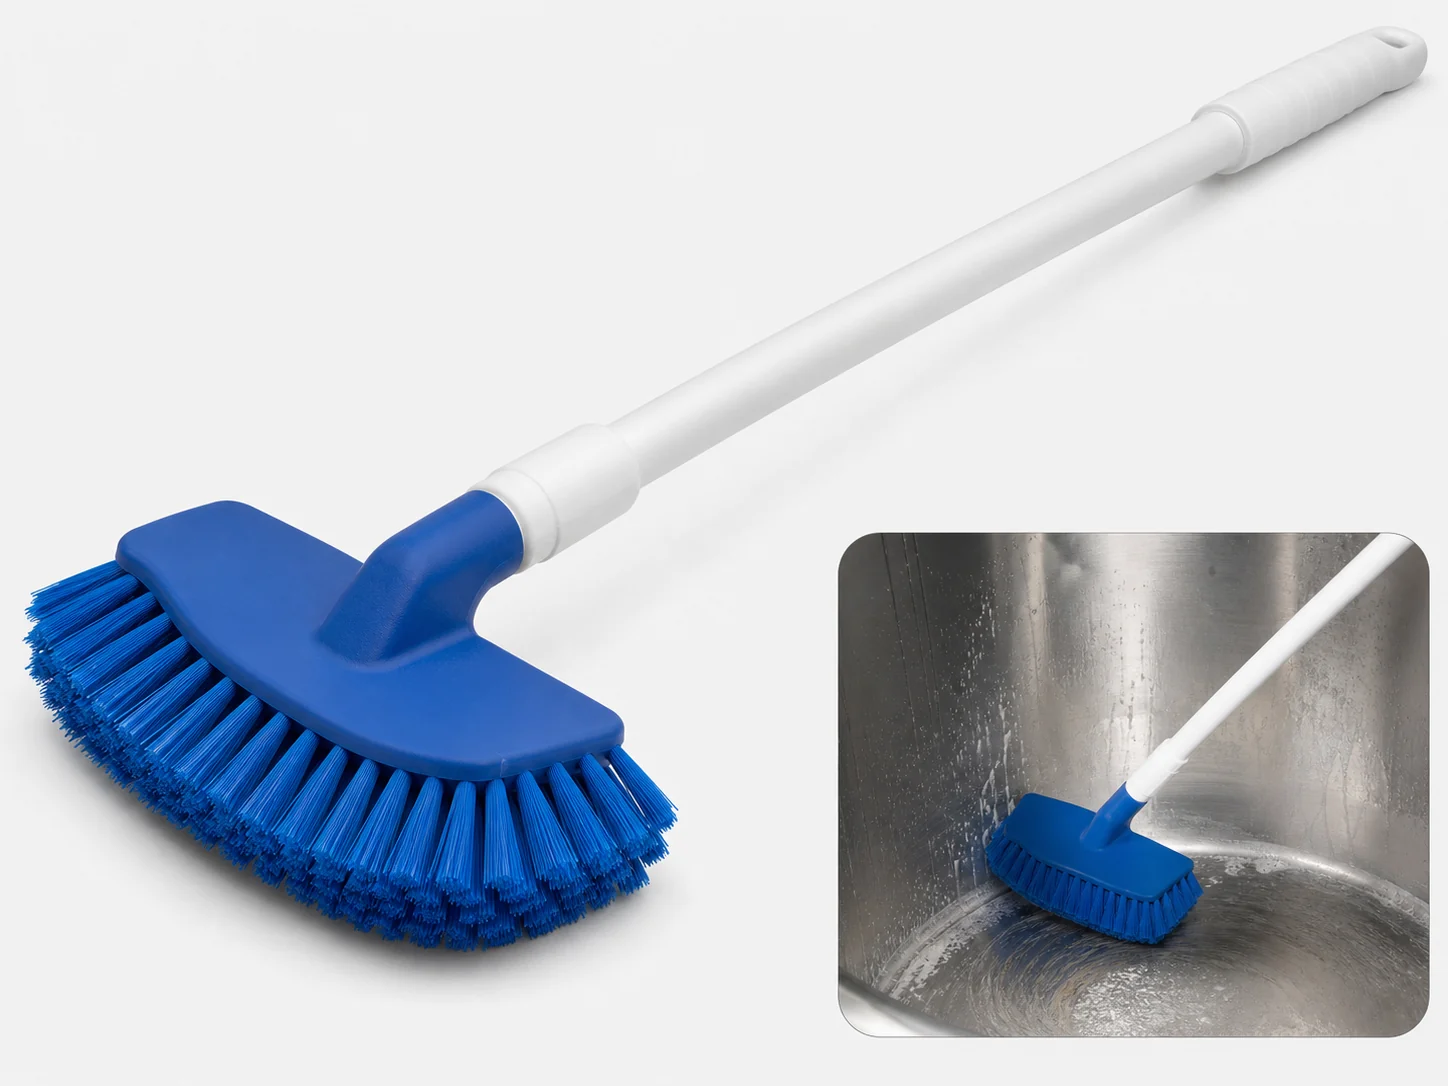
Brewery Tank Cleaning Brush
Radial fill contacts rounded tank walls without dead zones, lifting yeast film, beerstone and CIP residue from welds and manways with no metal contact.
Compare the specificationCustom Manufacturing RFQ
Describe Your Application
For an accurate quotation, please provide the main dimensions, material preference, working surface, residue, quantity, and a drawing or photo.
We reply to every request within 24 hours, with a quotation or with the questions we need answered first. If the brush can be made on our existing tooling, we make the sample directly. If it needs new tooling, we quote a sample fee and a tooling fee, and the sample fee is credited against the bulk order. Need an NDA first? We sign yours before you send drawings, and the files you send are never shown to other customers.
- MOQ500 pcs for small hand-held brushes, 100 pcs for medium and large ones
- SampleTypically 3–7 days
- ProductionFrom 7 days after sample approval, by size and quantity
- Payment30% deposit and 70% before shipment above US$10,000; smaller orders on agreed terms
Have the old brush? Send a photo on WhatsApp
Drawing or photo optional — it speeds things up, it does not gate the enquiry.
“We need a brush to remove wet residue from a stainless steel conveyor, about 800mm wide. The current brush wears quickly. We can send photos.”
“We sell drinkware and need a cleaning brush to include with the product. Quantity around 5,000 pieces.”