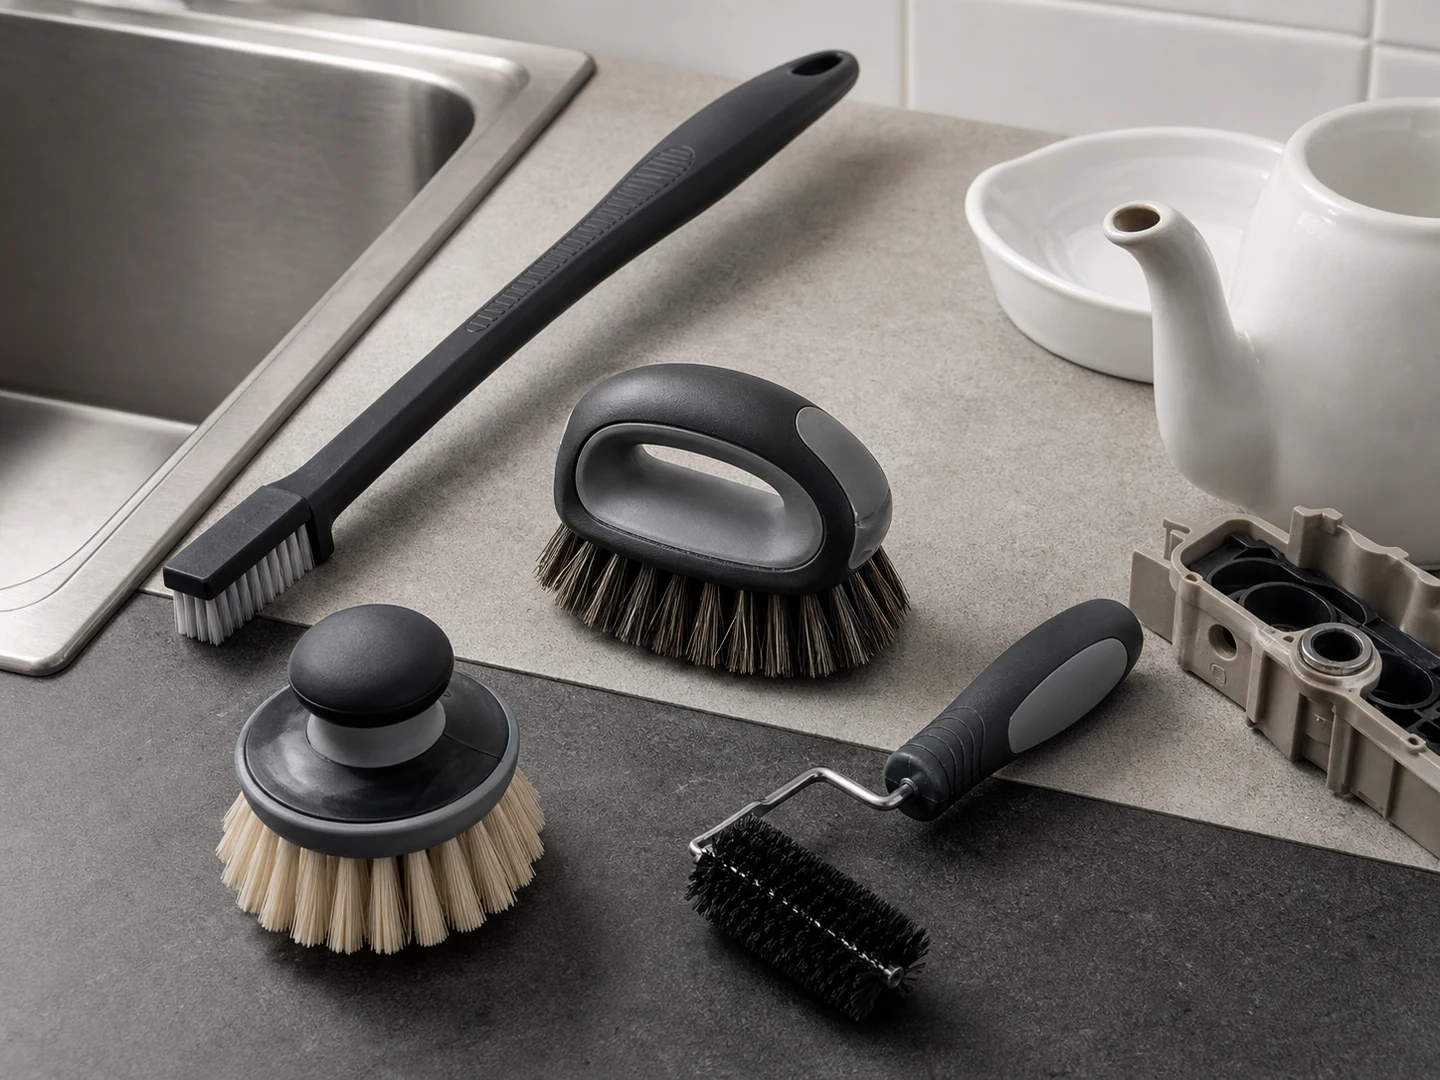
Why is a contact-surface brush judged differently?
Because it is judged by what it leaves, not only by what it removes. A filament in the product can mean a recall, and a fill whose materials cannot be shown to meet your standard cannot be used at all. Start from the standard and from how the brush holds its fill, then choose the head that reaches the seam.
What makes these surfaces different?
- The materials have to meet a standard: food-contact rules and, in pharmaceutical work, material traceability apply to the brush you buy, not only to how you use it. Name the standard, such as FDA 21 CFR or EU 10/2011, and the materials are chosen to it; food-contact testing is arranged per order, at the customer’s cost.
- Shedding is the failure: how well the fill is held matters more than how fast it cleans, and a brush that sheds is replaced, not kept going.
- Color coding is a process control: keeping brushes to their zones is often why a color is specified, and swapping the color breaks the control.
- The seam is the target: countertop joints, gasket grooves, tank welds and equipment corners hold what flat surfaces do not.
- The cleaning chemistry is harsh and daily: caustic, acid and peracetic sanitizer in rotation, often hot.
Which fill for which duty?
| Condition | Where to start | Why |
|---|---|---|
| Hot alkaline washdown | PBT | Keeps its stiffness wet and hot, where nylon softens |
| Acid and caustic in the same cycle | PBT or Polypropylene PP | Survives both ends of the CIP cycle |
| Daily peracetic or chlorine sanitizer | PBT | Does not swell or lose trimmed diameter over repeated cycles |
| A wiping or sealing edge against product | Silicone | A food-grade contact edge with no loose filament to come out; the edge still wears and can chip, so inspect it like any other brush |
| Delicate product: dough, produce, tablets | Soft Nylon PA or PU Sponge | Lifts residue without bruising or marking the product |
| Pharmaceutical process contact | PTFE Filament | Chemically inert |
How should a hygienic brush be built?
So that it can be cleaned as thoroughly as the surface it cleans: tufts held so they cannot pull out, a solid block with no cavity to hold residue, and a handle that hangs to drain. Where a brush stays on the machine, the same rule applies to the core and the mount. The head comes last, chosen from the narrowest seam it has to enter.
What usually goes wrong?
- Buying on cleaning performance and meeting the material requirement for the first time at the audit.
- Open staple pockets and blind holes in a wet zone. They hold water and product and are very hard to clean out, which is why wet zones often use brushes built without them.
- Ignoring the color code because the replacement in stock was another color. That is the control failing, not the brush.
- Keeping a worn brush past the point where it sheds. One shed filament costs more than the brush.
What should you send for a quote?
The zone and the standard it works to, the cleaning chemistry and temperature, whether the brush touches product directly, your color-coding scheme, and the narrowest seam it must reach.